
Preliminary Treatment

Preliminary wastewater treatment is a critical first step in the water treatment process, designed to prepare the inflow for subsequent treatment stages. This stage involves the removal of coarse solids and other large materials that could potentially cause damage to pumps and other treatment equipment. Doing so helps protect the intricate processes that follow, such as biological treatment and secondary clarification. A comprehensive preliminary treatment system usually includes screening and grit removal alongside other methods, such as comminution, which aids in breaking down large objects into smaller, more manageable pieces.
The importance of an effective preliminary treatment system cannot be overstated, as it ensures the efficient operation of the subsequent treatment stages. It can also be adapted for industrial wastewater pretreatment, adjusting to the varying nature of industrial effluents. Well-designed preliminary treatment is essential for maintaining the quality and performance of wastewater treatment plants and ensuring compliance with ever-evolving environmental regulations.
Key Takeaways
- Preliminary wastewater treatment is essential for removing coarse solids to protect subsequent treatment stages.
- It includes screening, comminution, and grit removal to manage waste materials.
- The design of preliminary treatment systems must accommodate diverse industrial effluents and regulatory standards.
Preliminary Treatment of Wastewater: Essentials for Efficient Process Flow
Preliminary wastewater treatment is the first critical stage in the wastewater treatment process, laying the groundwork for further filtration and purification. It is designed to remove large and small objects that could impede subsequent treatment phases.
Purpose and Goals
The primary purpose of preliminary treatment is to prepare wastewater for subsequent treatment processes by removing coarse solids and other large materials. These initial steps are crucial as they prevent damage to downstream equipment and reduce the load on secondary treatment facilities.
Process Overview
Preliminary treatment involves several physical operations, primarily:
- Screening: Removal of large waste solids such as rags, sticks, and plastics. Screening uses devices like bar racks and fine screens that act as sieves to capture solid materials.
- Grit Removal: Sedimentation of inorganic solids, like sand and gravel, is achieved through grit chambers. Grit removal protects downstream processes from abrasion and deposition.
- Comminution: A process that grinds the larger solids that pass through the screens into smaller pieces, making the ensuing treatment stages more effective.
These treatments are the quintessential steps included in what is known as the preliminary treatment of wastewater and set the stage for primary, secondary, and tertiary treatments that follow.
Subcategory Overview: Key Processes in Preliminary Treatment
Preliminary treatment encompasses several distinct unit processes, each targeting a specific category of influent material. Understanding how each process works — and how they interact — is essential for proper system design, operation, and troubleshooting. The subsections below cover the primary process types, their mechanisms, and their role in protecting downstream treatment.
Primary Treatment Process
Following the physical removal steps of preliminary treatment, the Primary Treatment Process represents the next major stage in the treatment train, focusing on the sedimentation of suspended solids and the separation of floatable materials through primary clarifiers. Where preliminary treatment removes gross solids and grit mechanically, primary treatment uses gravity settling in large basins to reduce total suspended solids (TSS) by approximately 50–70% and biochemical oxygen demand (BOD) by 25–40% before biological treatment begins. The efficiency of this downstream stage depends directly on how thoroughly preliminary treatment has removed screenings and grit — undersized screens or inadequately designed grit chambers will increase the solids loading to primary clarifiers, reducing their hydraulic retention time and settling performance. Engineers sizing primary clarifiers must account for the solids removal rates achieved upstream in preliminary treatment, as the two stages are hydraulically and operationally interdependent.
Screening
Screening is typically the first unit operation that raw influent encounters upon entering a treatment plant. Bar screens, step screens, and fine screens remove coarse materials — rags, plastics, wood, and other floatable debris — that would otherwise damage downstream pumps, clog pipes, and foul secondary treatment equipment. Screen opening sizes range from approximately 6 mm for coarse bar screens down to 0.5–1 mm for fine drum screens, with the appropriate selection depending on influent characteristics, downstream process sensitivity, and the plant’s regulatory requirements for solids capture. Mechanical screens with continuous self-cleaning mechanisms are standard at medium to large facilities, while manual bar screens remain practical for small or remote installations. The volume of screenings generated — typically 0.5 to 10 mL per liter of wastewater — drives decisions around compaction, washing, and disposal logistics.
Grit Removal
Grit Removal targets the inorganic heavy fraction of influent — sand, gravel, eggshells, coffee grounds, and similar dense particulates — that screens cannot capture due to their small size but high specific gravity. Left untreated, grit causes accelerated wear on pump impellers and mechanical components, accumulates in digesters and aeration basins, and reduces the effective volume of downstream tanks. Grit chambers are designed to achieve a controlled flow velocity — typically in the range of 0.3 m/s — at which inorganic grit settles while lighter organic solids remain in suspension and continue downstream. Common configurations include horizontal flow channels, vortex-type chambers, and aerated grit chambers, each with different removal efficiencies and headloss characteristics. Aerated systems are preferred where organic carryover is a concern, as the spiral flow pattern improves the selectivity of grit capture.
Comminution
Comminution addresses a practical gap in the screening process: materials that are too small to be captured by bar screens but large enough to cause problems downstream — rags, fibrous materials, and plastic fragments — are shredded in-line by comminutors or grinders. Rather than removing these solids from the flow, comminution reduces their particle size to a manageable range that can pass through the plant without fouling downstream equipment. Comminutors are installed in-channel and use rotating cutters or grinding mechanisms to process the material continuously. This approach eliminates the handling and disposal logistics associated with screenings but transfers the solids load into the liquid stream, which must ultimately be managed in the sludge treatment process.
Flow Equalization
Flow Equalization is a preliminary treatment strategy that buffers the hydraulic variability inherent in municipal wastewater collection systems. Diurnal flow patterns, storm events, and industrial batch discharges can cause influent flow rates to vary by a factor of 3–5 times or more relative to average daily flow. Equalization basins — either in-line or side-line — dampen these surges, allowing downstream unit processes to operate at more consistent hydraulic and organic loading rates. In-line equalization passes all flow through the basin and provides the greatest load dampening, while side-line configurations divert only peak flows, reducing basin volume requirements. Proper sizing of an equalization basin requires analysis of diurnal flow patterns, peak-to-average flow ratios, and the hydraulic capacity of the downstream processes being protected.
Oil and Grease Management
Oil, fat, and grease management is a specialized component of preliminary treatment, particularly relevant for facilities receiving significant contributions from food service establishments, food processing industries, or other FOG-generating sources. Grease interceptors and FOG traps intercept these materials before they enter the collection system, while dissolved air flotation (DAF) systems are used within treatment plants to float and skim oily materials from the influent stream. Uncontrolled FOG accumulation causes severe operational problems — including blockages in collection systems, reduced settling performance in primary clarifiers, and interference with biological treatment — making effective preliminary management essential wherever FOG concentrations are elevated.
Comparison of Preliminary Treatment Processes
The table below compares the primary unit processes used in preliminary wastewater treatment across key operational and design parameters.
| Process | Target Material | Removal Mechanism | Typical Applications | Key Limitations | Relative Cost | Maintenance Profile |
|---|---|---|---|---|---|---|
| Bar/Fine Screening | Coarse solids, rags, plastics, floatables | Physical interception (bar or mesh) | All municipal WWTP intakes; required by most permits | Does not remove fine inorganic grit or FOG | Low–Moderate | Daily inspection; regular cleaning of screen panels; screenings disposal |
| Grit Removal | Sand, gravel, dense inorganic solids | Gravity settling at controlled velocity | All municipal plants; especially those with CSO or SSO inputs | Does not remove fine organics; requires velocity control | Moderate | Grit chamber cleanout; pump and classifier servicing; periodic dewatering |
| Comminution | Rags, fibrous material, small solids | In-line mechanical shredding | Small–medium plants; older facilities lacking fine screens | Transfers solids to liquid stream rather than removing them; cutter wear | Low–Moderate | Regular cutter inspection and replacement; in-channel servicing required |
| Flow Equalization | Hydraulic and organic load surges | Detention and mixing in equalization basin | Plants with high peak-to-average flow ratios; combined sewer systems | Large footprint; requires mixing to prevent septicity; odor management needed | Moderate–High (capital) | Mixer servicing; pump maintenance; odor control equipment |
| Oil & Grease Removal | Fats, oils, and grease (FOG) | Gravity separation or dissolved air flotation | Food processing, restaurant, or industrial-heavy service areas | Limited effectiveness for emulsified FOG without chemical addition | Low (traps) – High (DAF) | Trap pumping frequency; DAF carrier water system; skim collection |
| Primary Treatment Process | Suspended solids, floatable organics | Gravity sedimentation in clarifiers | Municipal secondary WWTP upstream of biological treatment | Limited BOD removal; dependent on upstream preliminary performance | Moderate–High | Sludge removal; scum baffle cleaning; clarifier mechanism servicing |
Selection and Specification Framework
Comparing unit processes side by side is only the first half of the design decision. The second half is matching each process to the plant’s actual influent characteristics, flow regime, staffing model, and capital constraints. The sequence below reflects how headworks design decisions are typically made in practice.
Step One: Characterize the Influent and Flow Regime
Every downstream decision depends on knowing what actually arrives at the plant. Collect at minimum a full year of influent flow data at 15-minute or hourly resolution, then derive average daily flow, peak hour flow, peak-to-average ratio, and the wet-weather response of the collection system. Separate sanitary systems typically show peaking factors of 2 to 3, while combined or heavily infiltrated systems routinely exceed 4 to 5. Characterize the solids side as well: screenings volumes, grit quantities, and FOG loading vary enormously between service areas. Grit quantities in separate sanitary systems commonly fall in the range of 1 to 15 cubic feet per million gallons, while combined systems with sanded winter roads can generate an order of magnitude more. Designing a headworks on assumed values rather than measured ones is the single most common source of undersized channels and chronically overloaded grit systems.
Step Two: Select Screen Type and Opening Size
Screen selection is a trade-off between capture rate and screenings handling burden. Coarse bar screens with 25 to 50 mm clear openings protect pumps but pass most rags. Mechanically cleaned bar screens at 6 to 25 mm are the municipal default. Fine screens at 1 to 6 mm are increasingly specified where membrane bioreactors, fine-bubble diffusers, or thickening equipment sit downstream, because those processes are unforgiving of rag carryover. Every reduction in opening size increases screenings volume, and screenings handling — washing, compaction, containerization, and hauling — is where the operating cost lives. Specify the downstream process sensitivity first, then let it dictate the opening size rather than choosing the screen and hoping downstream equipment copes.
Step Three: Choose the Grit Removal Configuration
Horizontal-flow grit channels are the simplest configuration and rely on maintaining an approximately constant velocity near 1 ft/s, which requires a proportional weir or Parshall flume control section. They suit small plants with limited flow variation. Aerated grit chambers offer better organic selectivity and tolerate wider flow ranges, at the cost of air supply energy and diffuser maintenance. Vortex chambers provide the smallest footprint and lowest headloss, which makes them the common retrofit choice in constrained sites, though their fine-grit capture efficiency depends heavily on flow being kept within the design envelope. Whichever configuration is selected, the grit washing and dewatering train downstream deserves as much design attention as the chamber itself, since poorly washed grit with high organic content creates odor and disposal problems.
Step Four: Decide Between Comminution and Screening Removal
Comminution and screening solve the same problem in opposite ways: one removes solids from the stream, the other reduces their size and passes them on. Modern practice strongly favors removal. Shredded rags reassemble into ropes downstream, bind on pump impellers and mixer shafts, and accumulate in digesters, so the apparent savings in screenings handling reappear as downstream maintenance. Comminution remains defensible at small plants without staff to manage screenings handling, in retrofit situations where channel geometry cannot accommodate a mechanical screen, and as a backup in a bypass channel. New headworks designs should generally specify screening removal as the primary process.
Step Five: Determine Whether Equalization Is Warranted
Equalization is justified when the peak-to-average flow ratio exceeds what downstream processes tolerate, when industrial batch discharges create shock organic loads, or when wet-weather flows would otherwise force a bypass. It is expensive in footprint and requires active mixing and odor control to prevent septicity, so it should not be specified reflexively. Compare the capital and operating cost of a basin against the cost of upsizing the downstream processes it would protect; at plants with modest peaking factors, upsizing is often cheaper over the asset life.
Step Six: Weigh Lifecycle Cost and Staffing Reality
Headworks equipment is the most maintenance-intensive part of most treatment plants, and the labor assumption embedded in a design is as important as the equipment selection. A fine screen with an automated washer-compactor costs more at purchase but consumes far less operator time than a manually raked bar screen. Conversely, sophisticated equipment at a plant with one part-time operator and no local service support tends to end up bypassed. Match the level of automation to the staffing model the utility can actually sustain over a 20-year horizon.
Screening
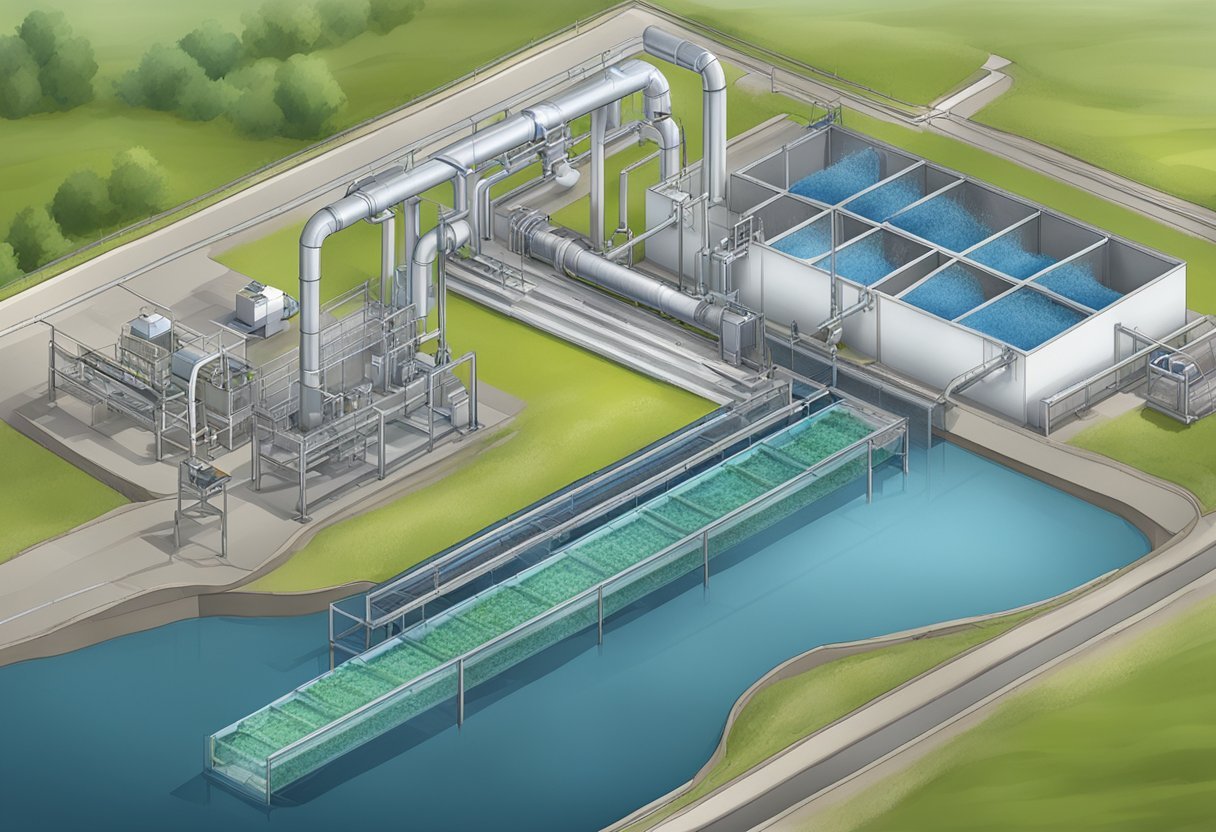
Screening is a crucial first step in the preliminary wastewater treatment process, designed to protect downstream equipment from large solids and various debris. Its efficiency impacts the performance and longevity of subsequent treatment stages.
Types of Screens
Multiple screens are utilized in wastewater treatment, each serving a distinct purpose. Manual screens require human effort and are suitable for small or remote facilities. On the other hand, mechanical screens are automated, handling larger volumes efficiently. Examples include bar screens, where wastewater passes through bars spaced to allow water flow while capturing larger solids, and fine screens, which have smaller openings to catch finer particles. Professionals looking for detailed equipment comparisons by manufacturer and configuration can explore our guide to Screening Equipment for bar screens and fine screen selection specifics.
Screening Equipment
Screening equipment is engineered to cope with diverse types of waste components. Coarse screens generally have openings over 6 mm and are the first line of defense. Micro screens with openings as small as 1 mm are employed for finer particles. The choice of equipment depends on factors such as flow rate, load debris, and downstream processes, with common types including rotary drums, step screens, and continuously cleaned bar screens.
Handling Screenings
The material captured by the screening process, known as screenings, requires careful handling. After removal, screenings are often washed to recover organic material and compacted to reduce volume, lowering disposal costs. Proper handling ensures that screenings do not contribute to odors or attract pests.
For a comprehensive look at screening in wastewater treatment, including maintenance and operation specifics, one can refer to resources like the U.S. Environmental Protection Agency’s guidance on Preliminary Wastewater Treatment. If not properly managed, these screenings can lead to increased operational costs and environmental concerns.
Bar Screens
Bar screens are employed primarily for the removal of large solids from wastewater. They consist of parallel bars that capture large debris while allowing water and smaller particles to pass through. Mechanical bar screens are often utilized with automatic mechanisms to clear the accumulated debris to facilitate handling and disposal. The effectiveness of bar screens depends significantly on the spacing between bars, which usually varies from 6 to 40 mm (US EPA).
- Typical Bar Screen Features:
- Material: Stainless steel or other corrosion-resistant materials
- Spacing: 6 to 40 mm
- Types: Manual or automatic
Comminution
In preliminary wastewater treatment, comminution refers to a process that grinds solid waste in the water into smaller pieces. This mechanical treatment is essential to prevent more extensive, solid matter from causing blockages or damaging the equipment in subsequent treatment stages.
Comminutors operate by using a combination of rotating blades or grinding mechanisms. As wastewater enters the comminution device, these blades effectively cut the solid materials, such as rags or plastic, into finer particles that can easily pass through the plant without hampering operations.
Debris Removal
The goal of debris removal is to protect the treatment facility’s infrastructure from damage caused by solids such as rags, sticks, and other materials. Innovative technologies like comminutors and grinders are introduced after bar screens to further shred and grind debris into smaller pieces, allowing for smoother processing. These units are typically installed in the channel and are essential for reducing the size of the debris, thus minimizing potential clogs and maintenance issues (WEF).
- Methods of Debris Reduction:
- Comminutors: Rotary devices that slice solids
- Grinders: Break down particles by abrasive action
- Installation: In-channel for continuous debris processing
Key Benefits:
- Protects Downstream Equipment: By reducing the size of solid particles, comminution safeguards pipes, pumps, and other apparatus from clogging or damage.
- Improves Processing: Smaller particle size can enhance the effectiveness of subsequent treatment processes, like sedimentation and biological treatment.
Considerations:
- Maintenance: Comminutors require regular upkeep to maintain their functional integrity and efficiency.
- Operation: Proper operation ensures the efficacy of the process, reducing the likelihood of malfunction or breakdowns.
Through comminution, wastewater treatment plants ensure that larger solids are reduced to a manageable size, aiding the overall treatment process and efficiency. When integrated with other preliminary treatments, such as screening and grit removal, these systems create a more consistent and controlled wastewater flow, less taxing on facility infrastructure.
Grit Removal
In the preliminary wastewater treatment, grit removal is critical for protecting downstream equipment from abrasion and minimizing deposit formation in channels and pipelines. Grit, primarily sand, gravel, and other heavy materials, is removed to prevent excessive maintenance and ensure efficient treatment operations.
Grit Chambers
Grit chambers are specifically designed basins where the velocity of wastewater flow is controlled to allow grit to settle out while organic material continues in suspension. They are typically rectangular or circular and constructed to provide easy grit sedimentation and removal. This process is fundamental as it reduces the wear on mechanical equipment, maintains tank volume, and prevents the grit from overflowing into other treatment units.
Aerated Grit Chambers
Aerated grit chambers employ aeration to create a spiral flow pattern to effectively separate grit from the wastewater stream. Air is introduced at the bottom of the chamber, which allows for a selective settling. Organic materials remain in suspension due to the upward velocity of air bubbles, thereby improving grit settling. This process offers a higher level of grit removal efficiency compared to non-aerated systems.
Grit Handling and Disposal
Once separated from the wastewater, grit must be handled and disposed of appropriately. Grit handling involves washing to remove attached organic material, dewatering to reduce volume and weight for disposal, and sometimes storing before final disposal. Proper disposal methods prevent environmental contamination and comply with regulations. Grit is often taken to landfills, but it can also be used as landfill cover, road-based construction material, or in other beneficial applications if it meets local standards for reuse.
Solids Removal

Preliminary treatment in wastewater management is crucial for removing solid pollutants before they reach the primary treatment stages. This step involves separating and eliminating various solids that could hinder the efficiency of subsequent processes.
Coarse Solids Removal
Coarse solids removal is a process that targets larger, easily removable objects from wastewater. This is often achieved using a physical barrier, such as a bar screen, which traps materials like sticks, rags, and large debris. The trapped solids are then mechanically removed to prevent damage to pumps and other equipment down the line. Additionally, this technique aids in the protection of more sensitive processes from operationally challenging waste.
Suspended Solids Removal
Suspended solids removal encompasses various methods to extract finer particles floating in the wastewater. Grit chambers are integral in this phase, designed to settle out sand, grit, pebbles, and other inorganic solids by reducing the flow velocity of wastewater, allowing dense particles to settle. The clarified effluent then moves forward for additional treatment, while the settled grit, often comprising inorganic materials, is cleaned out from the chamber. Removing these fine suspended solids is vital to prevent sediment build-up in tanks and channels and reduce the wear on mechanical components.
Oil and Grease Management
Managing oil and grease in wastewater is crucial to prevent blockages and maintenance issues in sewage systems. Effective removal techniques ensure that treatment plants operate efficiently and meet environmental regulations.
FOG Traps
Fat, oil, and grease (FOG) traps are essential in intercepting grease before it enters wastewater systems. They are typically installed in locations where oily waste is produced, such as restaurant kitchens. FOG traps work by cooling wastewater, allowing the lighter oil to separate and float while heavier solids settle at the bottom. These traps are regularly maintained to ensure they function correctly, as outlined in best practices for Fats, Oil, and Grease management.
Floating Materials Removal
Removing floating materials—such as oils and greases that rise to the surface of pretreatment tanks—is a critical step. Technologies for this process include skimmers that scrape the water’s surface to collect floating substances. This, combined with FOG traps, forms a comprehensive approach to managing oil and grease levels in wastewater, which is further described in the Effluent Guidelines Program Plan 14 by the U.S. Environmental Protection Agency.
Flow Regulation and Measurement
Flow regulation and measurement are critical components in the preliminary treatment of wastewater. They ensure consistent inflow rates and accurate monitoring, essential for efficient operation and compliance with environmental regulations.
Equalization
Equalization is the process of stabilizing the flow rate to facilitate consistent wastewater treatment. Through flow neutralization, heavy surges are buffered, and flow stabilization is achieved, improving the overall efficiency of the treatment plant. Equalization basins are used to dampen fluctuations, allowing for uniform flow conditions. For a detailed review of basin sizing, mixing requirements, and in-line versus side-line configurations, see our full guide on Flow Equalization in wastewater treatment.
Flow Control Devices
Flow control devices are instrumental in managing the movement of wastewater through a treatment facility. These include weirs and Parshall flumes, designed to measure flow rates accurately. Additionally, magnetic and ultrasonic flow meters monitor flow continuously, ensuring that regulation criteria are met and adjusting the process as needed. Accurate flow measurement and monitoring enable operators to maintain optimal conditions and adhere to permit requirements.
Pretreatment for Industrial Wastewater
Industrial wastewater requires effective pretreatment to protect both public health and the environment. Pretreatment processes are designed to remove harmful materials before sewage is discharged into municipal sewer systems. They typically involve physical, chemical, and biological steps to eliminate pollutants that could otherwise damage sewer infrastructure or interfere with subsequent treatment stages.
Physical Pretreatment Methods:
- Screening: Devices like bar screens and fine screens intercept solids like rags, sticks, and plastics.
- Sedimentation: This allows heavier particulate matter to settle out of the water column.
- Equalization Basins: These basins dampen flow surges and facilitate uniform treatment.
Chemical Pretreatment Options:
- Neutralization: For pH adjustment, either acids or alkalis may be added.
- Coagulation and Flocculation: These processes use chemicals to encourage the accumulation of fine particles into larger ones that can be removed more easily.
Biological Pretreatment Steps:
- Although less common as a preliminary measure, there are instances where specific biological treatments may take place to degrade organics.
Pretreatment prevents potential damage to treatment facilities and ensures compliance with regulatory standards for discharge. Successful pretreatment processes contribute significantly to the overall effectiveness of wastewater management and speak to the robustness of industrial responsibility in safeguarding water quality.
Design Considerations
When designing a system for the preliminary wastewater treatment, engineers must assess critical factors such as the variable loads the facility will encounter and the types of equipment that will best handle these conditions. Durability and ease of access for maintenance are likewise pivotal to ensure sustainable operation.
Hydraulic and Organic Loadings
- Hydraulic Loadings: Calculating the peak flow rates is crucial to determining the size of channels, screens, and grit chambers. Facilities must accommodate variations in flow and load while avoiding overflows during storm events.
- Organic Loadings: Preliminary treatment processes are not primarily designed for organic removal, yet they are affected by the presence of organic materials. Engineers must estimate the average and peak organic loads to appropriately size equipment to efficiently remove debris and grit without compromising the subsequent treatment stages.
Equipment Selection
- Types of Screens: The screen selection depends on the wastewater’s nature and the degree of material removal required. From coarse to fine screens, each serves the purpose of protecting downstream processes. The choice of screens significantly determines the efficiency of the preliminary wastewater treatment.
- Grit Removal Systems: Grit chambers, whether horizontal flow, aerated, or other types, should be chosen based on the specific needs of the facility. The design must facilitate effective grit extraction to prevent abrasion and sedimentation in downstream equipment.
Maintainability and Accessibility
- Equipment Access: The design layout must provide ample space for operations staff to access equipment easily for inspection, maintenance, and repairs. This ensures that screens and grit removal systems are readily reachable.
- Maintenance Planning: A system’s design should factor in the ease of equipment maintenance. For instance, mechanical screens and comminutors require regular servicing to remain operational. Thus, the inclusion of redundancies and the choice of durable materials are essential for long-term functionality.
Design Details and Standards
The sections above cover what each process does and how to choose between them. This section covers the numbers, methods, and published standards that govern how each is sized and specified.
Sizing Methodology
Headworks sizing follows a consistent sequence regardless of the technologies selected. Establish the design peak hour flow, since preliminary treatment is a peak-flow process rather than an average-flow process. Size the influent channel for a velocity that keeps grit in suspension until it reaches the grit chamber — approximately 2 to 3 ft/s at peak flow — while avoiding velocities so high that they scour deposits from the invert during low flow. Size the screen for the allowable headloss at peak flow with a partially blinded screen face, not a clean one, and verify that the resulting upstream water surface does not surcharge the incoming sewer. Then size the grit system for detention time and surface loading at peak flow, and confirm that the removal, washing, and dewatering equipment can handle the peak grit generation rate rather than the average. Finally, check the entire hydraulic profile from the influent sewer invert to the downstream process at both minimum and maximum flow.
Key Parameters That Differ by Process
- Bar screen approach velocity: typically 1.25 to 3 ft/s at the channel upstream of the bars, high enough to keep grit moving but low enough to avoid forcing debris through the openings.
- Bar screen headloss: commonly designed for roughly 6 inches clean and up to 24 inches at the cleaning trigger point, with the mechanism actuated on differential level rather than time alone.
- Horizontal grit channel velocity: approximately 1 ft/s maintained across the flow range by a proportional weir or flume control section, with detention on the order of 45 to 90 seconds.
- Aerated grit chamber detention: typically 2 to 5 minutes at peak flow, with air supply in the approximate range of 3 to 8 cubic feet per minute per foot of tank length.
- Vortex grit chamber detention: often under 30 seconds, with performance highly sensitive to staying inside the manufacturer’s flow envelope.
- Equalization basin volume: derived from a cumulative inflow mass diagram against the desired constant outflow rate, with mixing energy sufficient to prevent solids deposition and septicity.
All values above are typical or approximate design ranges and should be confirmed against the governing state standard and the equipment manufacturer’s data for the specific application.
Applicable Standards and References
Recommended Standards for Wastewater Facilities, commonly known as the Ten States Standards, governs headworks channel velocities, screen provisions, and grit chamber design in many states and is adopted or referenced by numerous state regulatory agencies. WEF Manual of Practice No. 8 / ASCE Manual of Practice No. 76, Design of Municipal Wastewater Treatment Plants, provides the underlying design methodology for screening, grit removal, and equalization. 40 CFR Part 403 establishes the National Pretreatment Program that governs industrial user discharges to publicly owned treatment works. 40 CFR Part 133 defines secondary treatment requirements that downstream processes must meet, which in turn drives preliminary treatment performance expectations. NFPA 820, Standard for Fire Protection in Wastewater Treatment and Collection Facilities, establishes hazardous area classification and ventilation requirements for headworks structures, which are among the most restrictive areas of a plant. OSHA 29 CFR 1910.146 governs permit-required confined space entry for grit chambers, wet wells, and channels.
Specification Checklist
- Design average, peak hour, and peak wet-weather flows, with the data source and period of record stated
- Measured or documented screenings, grit, and FOG generation rates for the service area
- Screen type, clear opening, materials of construction, and cleaning actuation logic
- Screenings washing, compaction, conveyance, and containerization approach
- Grit chamber configuration, control section, and design velocity or detention time
- Grit pumping, classification, washing, and dewatering equipment with capacity at peak generation
- Complete hydraulic profile at minimum, average, and peak flow, including bypass and channel isolation conditions
- Redundancy provisions: number of channels, bypass arrangement, and manual backup screen
- Odor control and ventilation design, with NFPA 820 area classification documented
- Confined space access, hoisting provisions, and equipment removal path for every submerged component
- Flow measurement device type, location, and accuracy required by the discharge permit
- Corrosion protection specification for the headworks environment, including coatings and fastener metallurgy
Field Notes
Commissioning Considerations
Headworks commissioning should include a witnessed test at both minimum and maximum design flow, not just at whatever flow happens to arrive on the day. Verify that the screen cleaning cycle triggers correctly on differential level, that the grit chamber control section maintains its design velocity across the flow range, and that the grit washer discharges material with visibly low organic content. Confirm that every isolation gate seats, that the bypass channel is functional, and that the manual backup screen can be installed by two operators without a crane. Record baseline headloss across each screen at a known flow; this becomes the reference against which future blinding is measured.
Common Specification Mistakes
- Sizing on average flow instead of peak hour flow. Preliminary treatment sees the full peak, and a channel sized on average flow surcharges the incoming sewer during the first storm.
- Assuming grit and screenings quantities instead of measuring them. Service-area variation is large enough that assumed values regularly miss by a factor of five or more.
- Specifying fine screens without a screenings handling train. Smaller openings mean far more screenings, and manual handling of that volume is not sustainable.
- Neglecting the control section on a horizontal grit channel. Without a proportional weir or flume, velocity varies with flow and the chamber either passes grit or captures organics.
- Omitting a bypass channel or a manual backup screen. Headworks cannot be taken offline, and there is no downstream process that tolerates raw influent.
- Under-designing ventilation and corrosion protection. The headworks is the most corrosive and most hazardous atmosphere in the plant, and NFPA 820 classification is frequently applied too late in design.
- Placing flow measurement in a hydraulically unsuitable location. Insufficient straight run upstream of a flume or meter compromises permit-required reporting accuracy.
Operations and Maintenance Comparison
Mechanically cleaned bar screens require daily visual inspection, periodic rake and chain servicing, and continuous attention to the screenings conveyor, which is the component most likely to jam. Fine screens add brush or spray-wash maintenance and are more sensitive to grease accumulation, particularly in cold weather. Grit systems shift the maintenance burden to pumps, cyclones, and classifiers, all of which handle an abrasive slurry and wear at a predictable rate; budgeting for wear parts on a defined interval is more effective than replacing on failure. Comminutors demand regular cutter inspection and are serviced in-channel, which brings confined space entry into routine maintenance. Equalization basins need mixer servicing and consistent attention to odor control, since a basin allowed to go septic will generate complaints faster than almost any other process at the plant.
Troubleshooting by Symptom
Rags accumulating on downstream pumps and mixers point to screen openings that are too large, a screen that is bypassing during peak flow, or a cleaning mechanism that is not keeping up. Grit accumulating in aeration basins and digesters indicates a grit chamber operating outside its velocity or detention envelope, or grit removal equipment that cannot keep pace with generation. High organic content in removed grit points to excessive capture velocity or an underperforming washer, and shows up as odor complaints at the dumpster. Rising headloss across a screen at unchanged flow signals blinding, usually from grease in cold weather. Persistent odor at the headworks generally traces to septic influent arriving from long force mains, and is addressed upstream or with chemical addition rather than by changing the preliminary equipment.
Pro Tip: Weigh Your Screenings and Grit
Most plants estimate screenings and grit volumes from container fill rates, which is imprecise and makes trending impossible. Recording hauled weights by load — and normalizing them to millions of gallons treated — turns preliminary treatment into a measurable process. The trend line reveals collection system changes, seasonal FOG patterns, and declining equipment performance months before an operator notices a problem, and it provides the documented generation rates that the next headworks design will need.
Environmental and Regulatory Compliance
In preliminary wastewater treatment, compliance with environmental and regulatory standards is paramount. Facilities must adhere to guidelines established by entities such as the U.S. Environmental Protection Agency to protect public health and the environment.
Key Components:
- Screening: To comply with regulations, facilities must effectively remove large solids through screening, which could otherwise damage equipment and hinder subsequent treatment stages.
- Grit Removal: Regulated removal of inorganic materials, such as sand, protects downstream processes from abrasion and sedimentation.
Regulatory Bodies:
- Federal: U.S. EPA
- State: Various state environmental agencies
- Local: Municipal wastewater treatment authorities
Compliance also involves meeting specified thresholds for removing objects and sediments in preliminary treatment. Regular inspections and monitoring are conducted to ensure adherence to prescribed effluent standards. Facilities may face penalties for non-compliance, including fines or sanctions.
Documentation is crucial. Facilities must maintain accurate operational parameters and incidents records to demonstrate continuous compliance. This documentation may be subjected to regulatory audits to confirm that environmental protections are being adequately observed.
By strictly following these regulations, preliminary wastewater treatment operations play a critical role in preserving water quality and safeguarding ecosystems.
Future Trends in Preliminary Wastewater Treatment
The landscape of preliminary wastewater treatment is evolving as technologies advance. Shortly, the sector anticipates several promising trends to enhance efficiency and sustainability.
- Automation and Smart Screening: The integration of automation is set to rise. Innovative screening technologies will utilize real-time monitoring to optimize the removal of large and small debris, thereby preventing mechanical issues downstream.
- Advanced Materials: Screens and other preliminary devices may employ advanced materials, which are more resistant to wear and corrosion. These materials will likely prolong the lifecycle of equipment and reduce maintenance requirements.
- Energy Efficiency: There will be an emphasis on reducing energy consumption within preliminary treatment facilities. This could involve adopting innovative designs that minimize the energy required for screening and grit removal.
- Resource Recovery: Preliminary treatment processes may start incorporating designs that facilitate the recovery of valuable resources, such as phosphorus from grit.
- Compact Designs: The need for more compact treatment systems is growing, particularly in urban settings. The industry may see more compact units that can handle larger volumes of wastewater relative to their size.
- Combination Systems: Units that combine several treatment stages into one may gain popularity. These systems can streamline wastewater treatment processes and offer substantial space savings.
Technologies like comminutors are expected to become more sophisticated, with improvements aimed at enhancing refined screening capabilities to protect downstream processes from operational problems.
It’s anticipated that future advancements will further solidify the critical role of preliminary treatment facilities in maintaining efficient and reliable wastewater treatment infrastructures.
Frequently Asked Questions
What are the main components involved in the preliminary stage of wastewater treatment?
In the preliminary stage of wastewater treatment, physical units like bar racks, coarse screens, fine screens, and comminutors are utilized to protect further treatment processes by removing large and small objects from the wastewater.
How does preliminary treatment differ from primary treatment in wastewater management?
Preliminary treatment is designed to remove large debris and protect equipment. In contrast, the primary treatment typically refers to the settling out of suspended solids through sedimentation tanks or clarifiers, which is the next step in wastewater management.
How does preliminary treatment differ from secondary treatment in wastewater management?
Preliminary treatment in wastewater management involves physically removing large solids and debris from the wastewater, while secondary treatment focuses on biological processes to remove dissolved and suspended organic matter. Preliminary treatments is the first step in the treatment process, preparing the wastewater for further purification in the secondary treatment phase.
Can you provide examples of standard equipment used during the preliminary wastewater treatment?
Standard equipment used during the preliminary treatment includes bar racks, fine screens for filtering debris, and grit chambers for separating sand and other small, heavy particles from the wastewater stream.
What are the objectives of using preliminary treatment before other stages in wastewater treatment?
Preliminary treatment aims to remove materials that could pose mechanical issues to downstream processes, reduce the load on secondary treatments, and increase the overall efficiency and lifespan of the wastewater treatment facility.
How does tertiary wastewater treatment build upon preliminary and primary treatments?
Tertiarywastewater treatmentr builds upon the previous stages by further polishing the effluent to achieve higher quality water standards, often involving advanced techniques like filtration, nutrient removal, and disinfection, intended for more stringent environmental regulations.
What substances are typically removed during the preliminary treatment of wastewater?
During the preliminary treatment, substances such as rags, large solids, and materials that could cause clogging or mechanical issues are typically removed to prevent damage to downstream treatment equipment and processes.
Which impurities are targeted for removal during the preliminary stage of water treatment?
In the preliminary treatment of water, the primary focus is removing large solids and grit. These include sticks, leaves, rubbish, sand, and gravel. These materials are typically screened out to protect the subsequent stages of treatment from physical damage and to reduce the overall load on the filtration systems.
Why is sedimentation an integral part of preliminary water treatment?
Sedimentation is a critical process in preliminary water treatment because it allows for settling suspended solids. The treatment plant can efficiently remove a significant portion of the solids from the water by giving these particles time to settle in a sedimentation basin. This process improves the effectiveness of downstream filtration and disinfection stages.
Conclusion
Key Takeaways
- Preliminary treatment is a peak-flow process — channels, screens, and grit chambers must be sized on design peak hour flow, because that is when downstream damage actually occurs.
- Measure, don’t assume, solids generation — screenings, grit, and FOG quantities vary by an order of magnitude between service areas, and assumed values are the most common cause of an overloaded headworks.
- Screening removal beats comminution in new designs — shredded rags reassemble downstream and reappear as pump, mixer, and digester maintenance rather than as savings.
- Grit chamber performance depends on velocity control — a horizontal channel without a proper control section will either pass grit at high flow or capture organics at low flow.
- Match automation to the staffing model — sophisticated headworks equipment at a plant without the staff or service support to maintain it ends up bypassed.
- Preliminary performance sets the ceiling for what follows — the Primary Treatment Process and every biological stage after it inherit whatever the headworks fails to remove.
Preliminary treatment is the least glamorous and most consequential stage of a wastewater treatment plant. Screening, grit removal, comminution, flow equalization, and FOG management each address a distinct fraction of the influent, and together they determine how much abrasion, ragging, and hydraulic shock the rest of the plant absorbs. A headworks designed on measured influent data, sized for peak conditions, and equipped with realistic screenings and grit handling will quietly protect tens of millions of dollars of downstream assets for decades.
The design framework is straightforward in outline: characterize the influent and flow regime from real data, select screen openings based on downstream process sensitivity, choose a grit configuration that suits the site’s flow variability and footprint, treat comminution as a legacy option rather than a default, and justify equalization against the cost of the processes it protects. Where those decisions are made deliberately and documented against the governing standards, preliminary treatment stops being a maintenance headache and becomes the reliability foundation the rest of the treatment train depends on.