
Henry Pratt vs Wey Valve for Gate Valves: Pros/Cons & Best-Fit Applications
Introduction
In the design and operation of municipal and industrial wastewater treatment plants, few components cause more disproportionate downtime relative to their cost than isolation valves. A seized gate valve in a grit chamber or a leaking knife gate in a sludge line can force partial plant shutdowns, bypass pumping, and significant unplanned maintenance expenditure. For engineers specifying isolation equipment, the market offers distinct tiers of technology, often represented by the choice between general-purpose municipal standards and high-performance severe-duty solutions.
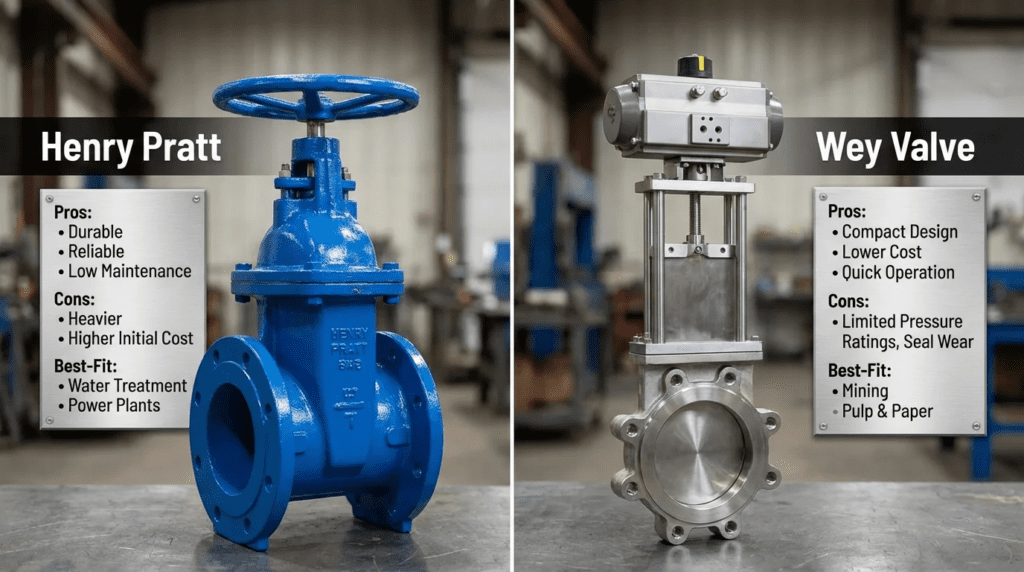
This article provides a technical comparison of these two approaches. Henry Pratt, a Mueller Water Products brand, is widely installed in the North American municipal market, known for broad compliance with AWWA standards. Wey Valve, part of Sistag, originated with a focus on difficult industrial slurries and is frequently specified for severe-duty applications involving grit, rags, and high solids.
For the consulting engineer or plant superintendent, understanding the mechanical nuances between these approaches—specifically regarding sealing geometry, body construction, and maintenance accessibility—is critical. Selecting the wrong valve type can lead to a line that cannot be isolated for pump maintenance, or rapid erosion of the seat in abrasive flows.
A correction to one side of this comparison. Wey Valve is correctly characterized: it is a Swiss manufacturer within the Sistag group, its knife gate valves are genuinely distinguished by the transverse sealing arrangement and pocket-free bottom geometry described below, and it is routinely specified for severe-duty slurry service.
Henry Pratt, however, is not a knife gate valve manufacturer. Pratt’s product lines are butterfly, ball and plug valves. Nor is Pratt the Mueller group’s resilient wedge gate valve brand — that is Mueller Co. The recognized knife gate manufacturers in North American municipal and industrial service are DeZURIK, Orbinox, Bray/Fabri-Valve, Wey and Red Valve, and a genuine bid comparison against Wey would be drawn from that list.
What remains valid, and is the reason this article is worth reading, is the underlying technology comparison: standard municipal knife gate construction against severe-duty construction, which is a real specification decision at the head of any plant handling grit. The article has been reframed on those terms, with Wey retained as the severe-duty example it legitimately is.
See also our guide to top gate valve manufacturers, and our comparisons of McWane and Mueller gate valve lines and DeZURIK and Bray.
How to Select / Specify
Duty Conditions & Operating Envelope
The first step in specification is defining the severity of the service. Standard AWWA C509 and C515 resilient wedge gate valves are excellent for clean water and treated effluent but often fail in raw sewage because debris prevents the wedge from seating. In these scenarios, knife gate valves are required.
- Solids Content: For fluids with low solids such as RAS and WAS, standard knife gates are generally sufficient. For high solids or heavy grit loads, the bottom seating geometry becomes critical.
- Operating Pressure: While standard municipal knife gates are commonly rated for Class 150 service, the ability to seal tightly at low differential pressures is often overlooked. Some designs rely on line pressure to assist the seal; in gravity flow lines, that assistance is absent.
- Frequency of Operation: Valves cycled daily, such as SBR fill and decant valves, require robust packing glands and actuation mounting hardware compared to isolation valves cycled annually.
Materials & Compatibility
- Body Materials: Cast iron or ductile iron is standard for municipal service. For industrial wastewater, 316 stainless steel or duplex stainless may be required. Modular designs allowing mixed materials, such as a ductile body with stainless wetted parts, offer flexibility that fully cast designs do not.
- Gate Materials: The gate blade must be harder than the seat to prevent galling. 17-4 PH stainless steel is a common upgrade for high-strength requirements.
- Seat Elastomers: EPDM is standard for water and wastewater. Nitrile is required if hydrocarbons or fats, oils, and grease are present. Fluoroelastomers are reserved for high-temperature industrial chemical service.
Installation Environment & Constructability
- Lug vs. Wafer: Full lug bodies are generally preferred for dead-end service capability. If a downstream pipe is removed for maintenance, the valve must hold full pressure.
- Face-to-Face Dimensions: In retrofit applications, MSS SP-81 standardizes the face-to-face dimension for knife gates. However, heavy-duty or wide-body valves designed for zero leakage may exceed these standard dimensions, requiring piping modifications.
- Orientation: Knife gates generally perform best in horizontal lines with the stem vertical. If installed in vertical lines, the potential for solids to settle in the bonnet or seat pocket increases, which differentiates flush-bottom designs from pocket designs.
Reliability, Redundancy & Failure Modes
The primary failure mode for knife gate valves is packing leakage, followed by seat leakage. The architecture of the packing gland is a major differentiator.
- Packing Gland Design: Standard designs use multiple layers of braided packing compressed by a gland follower. Over time, this packing consolidates and leaks.
- Transverse Seals: Advanced designs, notably Wey’s signature feature, use a transverse seal that can be re-energized or repacked while the valve is under full line pressure. This is a critical feature for process lines that cannot be drained for maintenance.
- Bottom Clogging: In conventional knife gates, the gate descends into a bottom groove to seal. This groove fills with solids, preventing full closure. Flush-bottom designs eliminate this cavity.
Lifecycle Cost Drivers
Capital versus operational expenditure is the central tension. A commodity knife gate carries a lower purchase price but may require frequent packing adjustment and earlier replacement. A severe-duty knife gate carries a higher purchase price but can operate far longer with minimal intervention. For critical buried service or inaccessible vaults, the higher capital option typically yields a lower total cost of ownership.
Comparison Tables
| Feature/Criteria | Standard Municipal Knife Gate | Wey Valve (Sistag) |
|---|---|---|
| Primary Market Focus | Municipal water and wastewater, general service | Industrial process, severe duty wastewater, mining |
| Key Design | Conventional perimeter seal; compliance with AWWA C520. | Transverse seal technology; pocket-free bottom design options. |
| Sealing Mechanism | Resilient seat, typically EPDM, located in the valve body. | Mechanically retained seal; repackable under pressure. |
| Bottom Body Geometry | Often uses a bottom cavity for the gate to seat, with risk of solids packing. | Available with flush bottom design to eliminate jamming in high solids. |
| Pressure Ratings | Typically Class 150 for standard AWWA service. | Standard Class 150, with high-pressure lines available well above that. |
| Maintenance Profile | Standard packing adjustments required; seat replacement usually requires valve removal. | Can be repacked under full pressure on applicable models; longer service intervals in abrasive media. |
| Cost Tier | Low to medium, competitive bid focus. | Medium to high, lifecycle performance focus. |
| Application | Recommended Strategy | Best Fit & Rationale |
|---|---|---|
| Potable Water Isolation | AWWA C509/C515 Resilient Wedge Gate | Waterworks gate valve. Resilient wedge gate valves are the industry standard, cost-effective, and certified for drinking water. |
| Raw Sewage (Headworks) | Knife Gate with stainless wetted parts | Severe duty. High grit and rag content can jam standard gates. Shearing capability and a pocket-free bottom prevent failure to close. |
| Return Activated Sludge | Standard Knife Gate | Either. RAS is generally non-abrasive and standard knife gates offer good value. Severe-duty designs are used where zero leakage is critical for process control. |
| Grit Slurry / Cyclone Feed | Severe Duty Knife Gate (hardened) | Severe duty. The abrasive nature of grit destroys standard resilient seats. Robust bodies with hardened deflectors are required. |
| Digester Gas Isolation | Zero Leakage Requirement | Severe duty. Gas service requires tighter shutoff than liquid service. Transverse seal technology provides superior gas tightness compared to standard packing. |
| Buried Service | High Reliability / Low Maintenance | Either. If a gate valve suffices, a resilient wedge gate is standard. If a knife gate is required buried, a design that avoids excavation for packing leaks is preferred. |
Engineer & Operator Field Notes
Commissioning & Acceptance Testing
During commissioning, verification of zero leakage claims is essential. For knife gate valves, MSS SP-81 permits a defined leakage rate for metal-seated valves, while most modern resilient-seated knife gates should hold effectively bubble-tight.
- Hydrostatic Testing: Ensure the valve is tested in the direction of flow indicated on the body. Many knife gates are unidirectional; testing in reverse can dislodge the seat.
- Actuator Stops: For electric actuation, set the open and close limits based on position, with torque protection as backup. A common error is setting the close limit strictly on torque, which can drive the gate through the bottom of the body as the seat wears.
Common Specification Mistakes
Standard resilient wedge gate valves have a pocket at the bottom where the wedge seats. In sludge lines, this pocket fills with debris, preventing the valve from sealing. Specify AWWA C520 knife gate valves for solids-bearing fluids.
Another frequent error involves unidirectional versus bidirectional specifications. While a manufacturer may state a valve is bidirectional, the pressure rating often drops significantly in the reverse direction. Engineers must review the reverse pressure rating specifically for pump discharge applications where backflow holding is required.
O&M Burden & Strategy
- Standard packing design: Maintenance focuses on tightening the packing gland follower, a routine task. If the seat fails, the line must be isolated and drained to remove the valve for rebuilding.
- Transverse seal design: Maintenance involves injecting sealing compound into the seal ports to re-energize the seal against the gate. This can often be done while the system is live, reducing downtime. However, operators must be trained not to over-pressurize the sealant, which increases actuation torque.
Troubleshooting Guide
- Symptom: Valve will not close completely.
Cause: Solids compacted in the bottom seating area.
Fix: If equipped with flush ports, purge the body. If not, the line must be depressurized and the valve flushed manually, which highlights the advantage of flush-bottom designs. - Symptom: Leakage at the stem area.
Cause: Packing relaxation.
Fix: Tighten gland nuts evenly. On transverse seal designs, inject sealing compound into the packing ports.
Design Details / Calculations
Sizing Logic & Methodology
Sizing a gate valve is typically straightforward, matching line size, but velocity checks are prudent. High velocities through a knife gate can cause flutter and gate vibration if the valve is used for throttling, which it generally should not be.
Isolation Is Only Real If You Can Prove It
Knife gate valves in wastewater service are usually installed for one purpose: to allow a piece of equipment to be taken out of service safely. That makes their failure mode more consequential than a leak rate suggests. A valve that passes when closed does not merely waste water; it puts maintenance staff into a line they believe is isolated.
Two design provisions address this, and neither is expensive at construction:
- Double block and bleed at critical maintenance points. Two valves in series with a drain between them allow staff to verify isolation by observing the bleed, rather than trusting a single closed valve. For confined space entry or for any line carrying digester gas, this should be the default rather than an upgrade.
- A drain or test connection downstream of every isolation valve serving equipment that will be opened. Without it, the only way to discover a passing valve is to break the joint.
The operational counterpart matters as much. Knife gates in solids service must be exercised, and exercised through full travel rather than cracked. A valve left open for years accumulates compacted solids in the seat area, and the first time it is genuinely needed is the worst time to discover it will not close the last few percent. Where the valve protects a lockout point, that exercise record is a safety document, not a maintenance convenience.
Actuator Sizing: The Safety Factor
When sizing pneumatic or electric actuators, the breakaway thrust is the critical parameter. It is the sum of the force from line pressure acting on the gate area multiplied by a friction factor, plus packing friction, plus a safety margin.
- Friction Factor: Varies by media. Clean water is at the low end; sludge and grit substantially higher.
- Packing Friction: Higher for transverse seal valves due to tighter seal compression compared with standard loose packing.
- Safety Factor: Roughly 1.25 for clean water, 1.5 to 2.0 for sludge and grit.
Engineers frequently undersize actuators for high-performance sealing designs because they apply standard friction tables. Tighter sealing requires higher thrust actuation.
Standards & Compliance
- AWWA C520: The governing standard for knife gate valves in municipal service, covering body materials, testing, and ratings.
- MSS SP-81: Stainless steel, bonnetless, flanged knife gate valves. Important for face-to-face dimension standardization.
- Flange Standards: Ensure the valve flanges match the mating pipe flanges and the correct pressure class.
- Build America, Buy America: For projects funded through the State Revolving Funds or WIFIA, domestic sourcing requirements apply to iron and steel products including valves.
FAQ Section
What is the main difference between standard and severe-duty knife gate valves?
The primary difference lies in design philosophy and target application. Standard municipal knife gates align with AWWA C520 and suit general water and wastewater service. Severe-duty designs feature transverse sealing and pocket-free bottoms, aimed at applications involving heavy slurries, grit, and industrial waste where zero leakage and online maintainability are required.
When should I specify a flush-bottom knife gate valve?
A flush-bottom design should be specified whenever the fluid contains solids that settle or compact, such as grit, lime slurry, or heavy sludge. In standard pocket designs, the gate must push into a groove to seal; if this groove fills with solids, the gate cannot fully close, leading to leakage.
Are knife gate valves suitable for throttling service?
Generally no. Knife gate valves are designed for on/off isolation. Using them for throttling places the gate in the high-velocity flow stream, causing vibration and rapid erosion of the bottom edge of the gate. If throttling is required, a V-port knife gate or a control valve should be selected.
Why is the transverse seal important?
Unlike standard stuffing boxes that compress vertical packing, a transverse seal creates a continuous seal profile that can be re-energized by injecting sealant while the valve is under pressure. This reduces downtime compared to standard packing glands that may require the valve to be isolated for maintenance.
Can I use a standard resilient wedge gate valve for wastewater?
Yes, with limitations. Resilient wedge gate valves are standard for potable water and clean effluent. However, for raw sewage or fluids with stringy solids, the wedge design can trap debris and prevent a seal. In these applications a knife gate is the superior engineering choice.
What is the typical lifespan of a knife gate valve in wastewater?
In general wastewater service, a quality knife gate can last 10 to 15 years. Wear components, the seat and packing, typically require attention every few years. In severe abrasive grit service, a standard valve may last only a short time, whereas a hardened severe-duty valve can extend that considerably.
Conclusion
KEY TAKEAWAYS
- Selection Rule: Use AWWA-standard valves for general isolation, RAS and WAS, and clean water. Use severe-duty designs for grit, heavy sludge, screening channels, and critical isolation points.
- Sealing Technology: Understand the difference between standard packing glands and repackable transverse seals.
- The Pocket Problem: Avoid pocket-bottom valves in grit or heavy solids service; specify flush-bottom designs to prevent jamming.
- Cost vs. Value: A high-performance valve commands a substantial price premium but eliminates the common failure modes of packing leakage and seat obstruction.
- Actuation: High-performance sealing requires higher actuator thrust. Do not use standard safety factors for severe duty valves.
The engineer’s role is to match equipment capabilities to process risk. There is no single best valve; there is only the correct valve for the specific duty cycle.
For the majority of municipal infrastructure where budgets are tight and fluids are relatively consistent, AWWA-compliant gate and knife gate valves offer reliable, industry-standard performance. They are the backbone of general municipal water infrastructure.
However, when the application shifts to the head of the plant—grit removal, screening, raw sewage—or into industrial slurry processing, the calculus changes. The cost of a valve failing to close, requiring bypass pumping and vacuum trucks, far exceeds the initial premium of a high-performance valve. In these scenarios, the robust architecture, transverse sealing, and flush-bottom designs characteristic of Wey Valve provide assurance against clogging and leakage.
Successful specification requires detailing not just pressure and flow, but the nature of the solids, the criticality of the isolation, and the maintenance capabilities of the plant staff.