
Metering Pumps Materials Selection: Cast Iron vs Stainless vs Duplex in Wastewater
Introduction
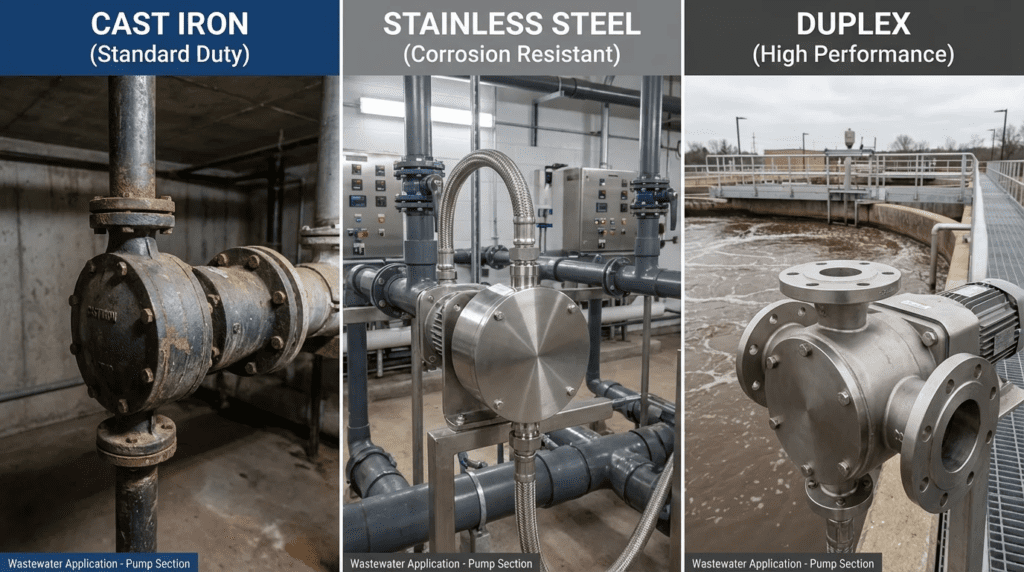
In municipal and industrial wastewater treatment, the precision of chemical dosing is directly linked to process compliance, yet the longevity of the dosing equipment is often compromised by material mismatching. A common point of failure in chemical feed systems is not the mechanical drive mechanism, but the degradation of wetted parts due to unforeseen corrosive or abrasive interactions. When engineers approach Metering Pumps Materials Selection: Cast Iron vs Stainless vs Duplex in Wastewater applications, they are navigating a trade-off between initial capital expenditure and total cost of ownership.
Plant reliability experience consistently shows that a large share of premature metering pump failures stem from chemical attack or material fatigue rather than from mechanical wear on the drive end. This is particularly prevalent in facilities handling aggressive coagulants, high-viscosity polymers, or abrasive lime slurries. While thermoplastic liquid ends (PVC, PVDF) dominate the low-pressure utility market, applications requiring high pressure, wide temperature tolerance, or hazardous-area compliance call for metallic liquid ends.
This article provides a technical framework for selecting between cast iron, 300-series stainless steel, and duplex stainless steel. It is designed to help consulting engineers and plant superintendents specify the correct alloy for the hydraulic, chemical, and physical stresses found in modern treatment facilities, and complements the broader guidance on how to specify metering pumps for municipal service. Improper specification can lead to leaks, process upsets, and safety hazards, making material selection a critical engineering discipline.
How to Select and Specify Metallic Liquid Ends
Selecting the appropriate alloy requires analysis beyond simple chemical compatibility charts. Engineers must consider the mechanical properties required to withstand the pulsating nature of reciprocating pumps alongside the electrochemical environment of the process fluid.
Duty Conditions & Operating Envelope
The first step is defining the hydraulic stress the pump head will endure. Unlike centrifugal pumps, metering pumps generate high peak pressures on each discharge stroke. The material must possess sufficient fatigue strength to withstand millions of cycles without cracking.
- Pressure Ratings: Pressure capability is set by the pump design, not by the alloy alone, but the alloy sets the ceiling the designer can reach. Cast iron liquid ends are limited by lower tensile strength and casting porosity concerns. 316 stainless steel covers the great majority of municipal and industrial metering duties. Duplex, with roughly double the yield strength, is what allows the very high discharge pressures encountered in sludge injection and deep-well disposal service. Always take the pressure rating from the manufacturer’s data for the specific model and material, not from the alloy.
- Temperature Dynamics: Treatment chemicals can react exothermically or be stored outdoors in freezing conditions. Metals offer superior dimensional stability over plastics across wide temperature ranges. Thermal expansion coefficients differ: 316SS expands more than duplex, which affects clearance tolerances in plunger pumps subject to thermal cycling.
- Variable Flow & Shock: In systems with rapid flow changes or potential water hammer, ductility matters. Duplex absorbs more energy before failure than gray cast iron, which is brittle.
Materials & Compatibility
When analyzing Metering Pumps Materials Selection: Cast Iron vs Stainless vs Duplex in Wastewater, chemical resistance is the primary driver.
Cast Iron (ASTM A48 gray / A536 ductile): Historically used for pump housings and occasionally for wetted parts in non-corrosive, near-neutral pH service. It is susceptible to general rusting and to rapid attack in acidic environments, where it undergoes graphitic corrosion — selective leaching of the iron matrix that leaves a weak graphite network behind, so the part retains its shape while losing nearly all strength. In modern wastewater plants its use in wetted parts is largely restricted to specific polymer blends or oil-based additives.
Stainless Steel (316/316L, cast equivalent CF8M): The industry standard. It relies on a passive chromium-oxide layer for protection and performs well with many polymers, alkaline solutions, and non-oxidizing acids. It is vulnerable to pitting and crevice corrosion in high-chloride environments such as brine, ferric chloride, or wastewaters with high total dissolved solids.
Duplex Stainless Steel (2205, cast equivalent CD3MN): A microstructure of roughly equal ferrite and austenite provides about double the yield strength of 316SS and substantially better resistance to localized corrosion. It is the preferred material for abrasive slurries, due to higher hardness, and for high-chloride environments where 316SS would be at risk of chloride stress corrosion cracking.
When specifying alloys for chloride-rich service, calculate the Pitting Resistance Equivalent Number:
PREN = %Cr + 3.3(%Mo) + 16(%N)
316SS typically lands around 24–26. Duplex 2205 is around 35. A PREN above roughly 32 is generally recommended for seawater or high-chloride brackish service. PREN is a screening tool, not a guarantee: it does not account for temperature, crevice geometry, or oxidizing species.
Hydraulics & Process Performance
Material hardness affects hydraulic efficiency over time, particularly in plunger-style metering pumps, where softer metals wear at the packing interface and lose volumetric efficiency.
- Cavitation Damage: If a pump cavitates, imploding bubbles produce micro-jets that erode the liquid end. Duplex, with higher hardness and strength, resists cavitation erosion better than cast iron or 316SS.
- Viscous Handling: For thick sludge or polymers, surface finish reduces friction losses. Stainless steels can be electropolished to low roughness values, improving flow characteristics for viscous fluids. Cast iron generally has a rougher as-cast finish, creating higher drag and potential deposition points.
Installation Environment & Constructability
The external environment is as critical as the internal fluid. Wastewater treatment plants often have atmospheres containing hydrogen sulfide (H2S) or chlorine vapors.
- Atmospheric Corrosion: Unpainted cast iron rusts rapidly in a headworks building. While initially cosmetic, this seizes bolts and impedes maintenance. 316 stainless is the baseline requirement for external hardware and pump heads in these zones.
- Structural Weight: Duplex allows thinner wall sections for a given pressure, reducing the weight of large high-pressure liquid ends and easing installation and maintenance access.
Reliability, Redundancy & Failure Modes
- Cast Iron: Fails by general corrosion and wall thinning, by graphitic corrosion in acid service, or by brittle fracture under impact or freezing.
- 316 Stainless: Susceptible to chloride stress corrosion cracking, with risk rising sharply above roughly 60 °C in chloride-bearing service. This failure mode develops with little external warning.
- Duplex: Specifically resistant to chloride SCC. Its failure mode is more commonly gradual wear or seal failure, which gives operators a leak as a warning sign rather than a sudden rupture.
Lifecycle Cost Drivers
The initial purchase price hierarchy is cast iron, then 316SS, then duplex. Operating cost frequently inverts that order.
If a 316SS liquid end requires replacement every few years due to pitting while a duplex head lasts the life of the installation, duplex yields a lower total cost of ownership even at a significant price premium. The labor cost to replace a liquid end, downtime, and cleanup costs for leaked chemicals usually exceed the material premium.
The Liquid End Is Not the Part That Fails
Nearly every specification conversation about metering pump materials is about the head casting. In service, the head casting is rarely what stops the pump. In a diaphragm metering pump the parts that fail are the diaphragm and the check valves, and neither is made of the alloy under discussion.
The diaphragm is the pressure boundary and the wear item. PTFE-faced diaphragms are the municipal default because PTFE is chemically inert across nearly everything a plant feeds, but PTFE is also relatively stiff, which limits stroke and makes the diaphragm sensitive to over-pressure events and to cold starts with viscous fluid. Specify the diaphragm material explicitly, specify a diaphragm rupture detection method for anything hazardous, and confirm the manufacturer’s diaphragm life expectation at the actual discharge pressure rather than at the catalog maximum.
The check valves determine whether the pump meters accurately at all. Volumetric accuracy in a reciprocating pump depends on the suction and discharge valves seating completely on every stroke, which is exactly what solids, crystallizing chemicals, and off-gassing prevent. Ball and seat material selection is a separate decision from the head: ceramic or alumina balls for abrasives, PTFE or elastomer seats for compliance against fine grit, and double ball arrangements for low-flow accuracy. Lime slurry and sodium hypochlorite both defeat single-ball valves, for opposite reasons — one deposits, the other off-gasses and unseats the ball.
The practical instruction is to write three separate material lines into the specification: liquid end alloy, diaphragm, and check valve balls and seats. A specification that names only “316SS liquid end” leaves the two components that actually govern accuracy and uptime to the vendor’s standard selection.
Material Comparison Tables
The following tables compare the three primary metallic options. Use Table 1 for technical property analysis and Table 2 to determine best fit for specific wastewater applications.
| Feature | Gray Cast Iron (A48) | Ductile Iron (A536) | Stainless Steel (316L / CF8M) | Duplex (2205 / CD3MN) |
|---|---|---|---|---|
| Corrosion Resistance (General) | Low (rusts readily) | Low (rusts readily) | High (passive layer) | Very high (resists pitting) |
| Chloride Resistance | Poor | Poor | Moderate (risk of SCC) | Excellent (resists SCC) |
| Abrasion Resistance | Moderate | Moderate | Moderate | High (greater hardness) |
| Yield Strength (Approx.) | No meaningful yield point; brittle. Tensile roughly 20–60 ksi by class. | 40–55 ksi depending on grade | ~30 ksi minimum for CF8M castings | ~65 ksi minimum for CD3MN castings |
| Failure Character | Brittle fracture; graphitic corrosion in acid | Ductile but corrodes | Ductile; SCC risk in chlorides | Ductile above about −50 °F; embrittles at cryogenic temperatures |
| Typical Application | Drive housings only | Non-corrosive oils, neutral slurries, housings | Polymers, dilute acids, general chemical feed | Abrasive lime, high-pressure sludge, high chlorides |
| Relative Cost Factor | 1.0 (baseline) | 1.1–1.3× | 1.8–2.5× | 3.0–4.0× |
| Chemical / Fluid | Cast Iron Suitability | 316SS Suitability | Duplex Suitability | Engineering Notes |
|---|---|---|---|---|
| Polymer (emulsion / Mannich) | Acceptable if pH neutral | Best fit | Unnecessary | 316SS is standard. Cast iron can rust and contaminate the polymer, reducing its effectiveness. |
| Lime Slurry | Poor (erosion risk) | Good | Best fit | Duplex hardness resists lime grit better than 316SS. Check valve ball and seat selection matters more than the head here. |
| Ferric Chloride | Unacceptable | Poor / risky | Conditional | Ferric attacks most metals. PVDF or titanium are preferred. If metal is required for pressure, duplex or super duplex is the minimum. |
| Sodium Hypochlorite | Unacceptable | Unacceptable | Poor | Warning: trace transition metals catalyze hypochlorite decomposition, releasing oxygen that gas-locks the pump and accelerates loss of strength in the solution. Titanium or a high nickel alloy are the only reasonable metals; PVDF is the normal choice. |
| Raw Sludge / Scum | Moderate | Good | Best fit | High solids and variable pH favor the hardness and corrosion resistance of duplex. |
Engineer & Operator Field Notes
Specifying the material is only half the task. Successful implementation requires acceptance testing and maintenance protocols tailored to the metallurgy selected.
Commissioning & Acceptance Testing
- Hydrostatic Testing: Ensure the liquid end is hydrotested above the design pressure per the manufacturer’s procedure. Check for weeping at casting pores, although modern investment casting largely eliminates this.
- Passivation Verification: For 316SS and duplex, request certificates of passivation. If the passive layer was damaged during machining or assembly and not restored, the pump will show tea staining or rust spots within weeks in a humid plant environment.
- Material Traceability: For critical high-pressure applications, require positive material identification by X-ray fluorescence to confirm the alloy matches the specification, including molybdenum content for 316 and the ferrite balance for duplex.
Common Specification Mistakes
Specifying “stainless steel” without designating the grade is a critical error. 304SS lacks molybdenum and will fail rapidly in chloride-bearing wastewater. Always specify ASTM A351 Grade CF8M (cast 316) or ASTM A890 Grade 4A (CD3MN, duplex 2205) as a minimum.
Another error is coupling dissimilar metals. Connecting a duplex liquid end to carbon steel piping without dielectric isolation creates a galvanic cell that accelerates corrosion of the carbon steel at the connection.
A third is specifying the head alloy and leaving the diaphragm and check valve materials to the vendor’s standard, which puts the two shortest-lived wetted components outside the specification entirely.
O&M Burden & Strategy
- Cast Iron: Requires regular external painting to prevent housing corrosion. Monitor for wall thinning if used in slurry service.
- Stainless Steel (316): Requires periodic cleaning to remove deposits. Under-deposit corrosion is a leading killer of stainless steel: where sludge or chemical scale builds on the surface, oxygen is depleted locally and the passive layer breaks down.
- Duplex: Lowest maintenance burden. Higher hardness means integral check valve seats last longer, reducing the frequency of head replacement or re-machining.
Troubleshooting Guide
Symptom: Reddish-brown staining on a stainless liquid end.
Cause: Iron contamination from tools used previously on carbon steel, or depletion of the passive layer.
Fix: Passivation treatment. If pitting has progressed, replacement is necessary.
Symptom: Cracks radiating from bolt holes.
Cause: Chloride stress corrosion cracking in 316SS, or over-torquing in cast iron.
Fix: Upgrade the alloy if SCC is confirmed; enforce torque values if mechanical overload.
Symptom: Dose drifts down while the stroke setting is unchanged.
Cause: Check valve fouling or wear, or a partially failed diaphragm — not a head material problem.
Fix: Inspect and replace valve balls and seats, then verify delivered volume against a calibration column.
Design Details and Calculations
Sizing Logic & Methodology
When selecting the material, evaluate the flow velocity through the liquid end ports. High velocities with abrasive fluids accelerate erosion.
- Calculate Port Velocity: velocity equals volumetric flow rate divided by port cross-sectional area, in consistent units. Use the peak instantaneous rate, not the average: a simplex reciprocating pump delivers its flow over a fraction of each cycle, so peak port velocity is several times the mean.
- Evaluate Erosion Risk: For lime slurry or grit-bearing sludge, 316SS erodes prematurely at sustained high velocity. Duplex tolerates higher velocity in abrasive service because of its greater hardness. Where the duty permits, lowering velocity by increasing port size is more effective than upgrading the alloy.
- Derating for Temperature: Metals lose strength as temperature rises. Wastewater service is typically near ambient, but exotherms and hot chemical rooms raise head temperature. Confirm the alloy’s allowable stress at operating temperature per the applicable piping or vessel code.
Specification Checklist
- Liquid End Material: state “ASTM A351 Grade CF8M (316SS)” or “ASTM A890 Grade 4A (duplex 2205).”
- Diaphragm: state the material and facing (for example PTFE-faced) and require a rupture detection provision for hazardous chemicals.
- Check Valves: state ball and seat materials and configuration (single or double ball) for the specific chemical.
- Check Valve Seats: specify whether seats are integral, which is practical in duplex, or replaceable inserts, which is preferable in 316SS.
- Surface Finish: specify a maximum roughness value for polymer service to facilitate cleaning.
- Fasteners: “all external hardware shall be 316 stainless steel.” Do not allow zinc-plated steel fasteners on a stainless liquid end.
- Calibration: require a calibration column or equivalent means of verifying delivered volume in the field.
Standards & Compliance
- API 675: the standard for controlled-volume positive displacement pumps, defining steady-state accuracy, linearity, repeatability, and construction requirements. Frequently adopted for high-specification projects.
- ASTM A351 / A890: the casting specifications that give the alloy designations worth naming in a specification.
- NACE MR0175 / ISO 15156: written for sour service in oil and gas and framed around H2S partial pressure, so it does not transfer directly to municipal wastewater. Where it is referenced for digester-area equipment, cite it as guidance for material selection rather than as a governing requirement, and confirm the actual H2S exposure.
- NSF/ANSI 61: required for wetted components in potable water chemical feed. Certification applies to specific products, not to alloys generically.
Frequently Asked Questions
What is the main difference between 316 stainless steel and duplex for metering pumps?
Strength and localized corrosion resistance. Duplex 2205 has a mixed austenitic-ferritic microstructure giving roughly twice the yield strength of 316 austenitic stainless. It also resists chloride stress corrosion cracking and pitting substantially better, making it the right choice for abrasive slurries and high-chloride wastewater, at a higher initial cost.
When should I use cast iron for a metering pump in wastewater?
For the non-wetted drive housing, and for liquid ends only in non-corrosive, near-neutral pH service such as certain oil-based additives or neutral polymers where cost is the binding constraint. It is not recommended for general chemical dosing — acids, hypochlorite, coagulants — because of poor corrosion resistance and the risk of contaminating the process fluid.
Is 316L stainless steel compatible with sodium hypochlorite?
Generally no. 316L tolerates very dilute hypochlorite briefly, but the oxidizing nature of the solution causes pitting and crevice corrosion, and dissolved transition metals catalyze decomposition of the hypochlorite itself, producing oxygen that gas-locks the pump. Specify PVDF or PVC, or titanium or a high nickel alloy where metal is unavoidable.
Does duplex stainless steel require special maintenance?
It requires the same passivation discipline as 316SS but is more forgiving in service. Its hardness makes it less prone to handling damage during disassembly. Because the head will likely outlast the soft goods by many years, the practical maintenance focus shifts to diaphragms, valve balls, and seats.
How does temperature affect the choice between stainless and duplex?
Both perform well at wastewater temperatures. 316SS has a higher coefficient of thermal expansion, so duplex is more dimensionally stable under thermal cycling. At the cold end the comparison reverses: austenitic 316SS retains toughness to cryogenic temperatures, whereas duplex is generally limited to around −50 °F because of a ductile-to-brittle transition. This rarely governs in wastewater but matters for outdoor northern installations handling cold chemicals.
Why do specifications call for 316L instead of 316?
The L designates low carbon, at most 0.03%. Lower carbon prevents precipitation of chromium carbides at grain boundaries during welding or slow cooling from casting, which would leave the adjacent metal depleted in chromium and vulnerable to intergranular attack. For welded liquid end assemblies, 316L is the preferred standard.
How does material selection interact with reading the pump curve?
Materials set the pressure ceiling; the curve tells you where on that ceiling you are operating. Erosion and fatigue both scale with the peak discharge pressure and the port velocity at the actual operating point, not the catalog rating, which is why the material decision should follow the duty analysis described in the guide to metering pumps pump curve reading rather than precede it.
Conclusion
KEY TAKEAWAYS
- Cast Iron: Relegate to drive housings and non-corrosive, neutral service only. Low cost, short life in corrosive zones, and prone to graphitic corrosion in acid.
- 316L Stainless: The workhorse, suitable for most metallic metering duties including polymers and pH adjustment. Vulnerable to chlorides and to stress corrosion cracking at elevated temperature.
- Duplex (2205): The problem solver, for high pressure, high abrasion, or high chloride. Highest initial cost, often the lowest lifecycle cost.
- Specify Three Materials, Not One: Liquid end alloy, diaphragm, and check valve balls and seats. The last two are what actually fail.
- Fatigue Matters: Metering pumps impose pulsating loads; rank materials by fatigue strength, not just corrosion resistance.
- Use ASTM Grades: Name CF8M or Grade 4A to avoid receiving an inferior generic alloy.
The decision process for Metering Pumps Materials Selection: Cast Iron vs Stainless vs Duplex in Wastewater balances chemistry, mechanics, and economics. Cast iron is a legacy material with limited remaining utility in corrosive treatment processes; the meaningful choice is between 316L and duplex 2205.
For standard polymer and buffer solutions, 316L remains the most cost-effective and readily available option. As chemical feeds become more concentrated and plants push for longer maintenance intervals, duplex is increasingly the standard for high-load applications. By analyzing PREN values, abrasion risk, and peak pressure — and by writing the diaphragm and check valve materials into the specification alongside the head alloy — engineers can specify systems that minimize downtime and protect public infrastructure investment.