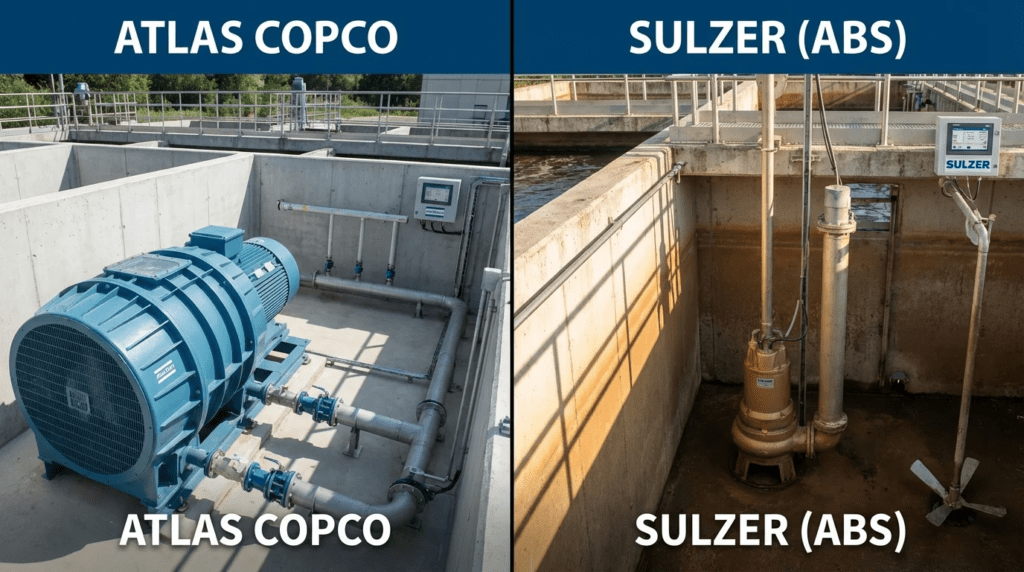
Atlas Copco vs Sulzer (ABS) Aeration Equipment: Comparison & Best Fit
Introduction
For municipal and industrial wastewater treatment plants, aeration is typically the largest single consumer of plant energy. Consequently, the selection of air generation technology is arguably the most critical decision influencing a facility’s 20-year operational expenditure. Engineers tasked with upgrades or new plant designs frequently encounter a choice between market stalwarts, leading to the necessity of a detailed analysis of Atlas Copco versus Sulzer (ABS) blower equipment. While both manufacturers offer high-efficiency solutions, their technological lineages—Atlas Copco stemming from industrial compressed air and Sulzer from specialized wastewater fluid handling—result in distinct operational characteristics.
This equipment is primarily utilized in activated sludge processes, membrane bioreactors, and aerobic digestion systems where oxygen transfer efficiency and reliability are paramount. The operating environment is harsh, characterized by continuous duty cycles, high harmonic loads on electrical infrastructure, and the necessity for wide turndown to match diurnal flow variations.
A poor specification in this category often leads to blow-off, meaning wasted energy during low demand, surge instability, or premature bearing failures due to heat management issues. This article provides a strictly technical, comparative analysis to help engineers navigate the nuances of magnetic bearings, screw technology, and high-speed turbo blowers to ensure the selected equipment aligns with specific process hydraulics and maintenance capabilities.
This is a genuine head-to-head comparison. Atlas Copco and Sulzer compete directly in high-speed turbo blowers for wastewater aeration, across the same duty range, and are routinely named as alternates in the same specification section. The distinctions drawn below are real engineering differences rather than marketing positioning. Note that the subject here is air generation equipment — the blowers themselves — not the diffusers and distribution piping that deliver the air to the basin floor. For that side of the system, see our comparison of SSI and Sanitaire diffused aeration equipment.
This guide sits within our coverage of aeration equipment manufacturers. See also our comparison of Kaeser and Gardner Denver blowers.
Editorial note: this revision removes an unrendered internal cross-reference that had published as literal markup inside one of the FAQ answers, and corrects the description of turndown, which the earlier version expressed as a percentage range rather than as a ratio.
How to Select / Specify
The selection process must move beyond simple nameplate horsepower. The interaction between the blower technology and the system curve determines the actual operating efficiency. The following criteria define the engineering framework for selection.
Duty Conditions & Operating Envelope
The primary driver for selection is the definition of the operating envelope. Wastewater influent flows are rarely static. The system must accommodate minimum day and minimum month flows up to peak wet weather flows.
- Turndown: Turndown is the ratio between the maximum and minimum flow the machine can deliver under control without venting air. A machine capable of operating from 100 percent down to 40 percent of rated flow has a turndown ratio of 2.5 to 1. Magnetic bearing turbo blowers from both manufacturers typically deliver turndown in this range, while Atlas Copco’s ZS screw blowers can often achieve wider effective turndown in lower pressure applications due to positive displacement physics.
- Pressure Fluctuations: In systems with fluctuating water levels, such as SBRs or deep tanks, positive displacement screw machines maintain efficiency across varying discharge pressures better than dynamic turbo machines, which are sensitive to discharge pressure changes.
- Temperature Sensitivity: Inlet air temperature affects density and consequently oxygen mass transfer. Specifications must define performance at the worst-case scenario, typically high ambient summer temperature, to prevent motor overloads or capacity shortfalls.
Materials & Compatibility
While the blower air end is often isolated from the wastewater, the surrounding environment is corrosive due to hydrogen sulfide. The construction of the enclosure and cooling system is critical.
- Impeller Metallurgy: High-speed turbo blowers utilize impellers spinning at 20,000 to 40,000 rpm and above. Materials typically range from high-strength aluminum alloys to titanium. Titanium is preferred for fatigue resistance in high-cycle start/stop applications.
- Cooling Systems: Both manufacturers offer air-cooled and water-cooled options. Air-cooled units require careful HVAC design in the blower room to prevent recirculation of hot air. Water-cooled units, common in larger frames, remove heat load from the room but introduce a water loop maintenance requirement.
- Enclosure Ratings: Standard industrial enclosures may not suffice if the blowers are located near the basins. NEMA 4X is rarely standard for the main cabinet but should be considered for HMI and control interfaces.
Hydraulics & Process Performance
Wire-to-air efficiency is the only valid comparison point. This accounts for losses in the inlet filter, the compression element, the motor, the variable frequency drive, and the cooling fans.
- Efficiency Curves: Do not select based on a single design point. Analyze the efficiency curve superimposed over the plant’s diurnal flow profile. A machine that is 2% more efficient at peak flow but 10% less efficient at average flow will cost more to operate.
- Surge Margins: For turbo blowers, the surge line is a critical constraint. Operating too close to the surge line causes flow instability and potential damage. Both manufacturers utilize advanced control logic to map the surge line, but the physical design of the impeller determines the natural surge margin.
- Rise-to-Surge: This defines how much pressure can increase before the machine surges. Systems with high static head variation require a steeper rise-to-surge characteristic.
Installation Environment & Constructability
Retrofit applications often present significant space constraints. Modern high-speed turbo blowers are significantly smaller than equivalent multistage centrifugal or positive displacement lobe blowers.
- Footprint Density: Both manufacturers’ turbo units are packaged designs, integrating the drive, controls, and blow-off valve. This minimizes site wiring but concentrates heat generation.
- Piping Interfaces: Discharge cone expansion is often required immediately after the blower. Specifications must dictate the distance of straight pipe runs required upstream of the inlet to ensure laminar flow for air mass meters.
- Electrical Harmonics: High-speed motors utilizing permanent magnet synchronous designs require specialized drives. These can generate significant harmonic distortion. Active front end or passive harmonic filters are mandatory specifications to meet IEEE 519 at the point of common coupling.
Reliability, Redundancy & Failure Modes
The core technological differentiator often lies in the bearing design.
- Active Magnetic Bearings: Used by Sulzer HST and Atlas Copco ZB. The shaft levitates, with no physical contact, theoretically offering very long bearing life. The risk point is the complexity of the magnetic bearing controller and the backup power system required to land the shaft safely during a power outage.
- Air Foil Bearings: Used in some smaller turbo units. These are passive and simpler but require a minimum speed to generate the air film. They are susceptible to damage during frequent start/stop cycles if the landing wears the foil coating.
- Rolling Element Bearings: Used in screw blowers. These have a finite life, typically 40,000 to 100,000 hours, and require lubrication, but the failure modes are mechanical and predictable through vibration analysis.
Controls & Automation Interfaces
Modern blowers are essentially computers that compress air. Integration with the plant SCADA is accomplished via industrial protocols such as EtherNet/IP, Modbus TCP, and PROFINET.
- Master Control Panels: In multi-blower installations, a master panel is required to sequence the blowers, balance runtime, and optimize efficiency. Both manufacturers offer sequencing logic. The panel must handle split-range control if different blower technologies are mixed.
- DO Control Loop: The blower controller should ideally receive the dissolved oxygen or ammonia setpoint directly, rather than just a speed reference. This allows the internal logic to optimize the pressure and flow relationship to meet demand.
Maintainability, Safety & Access
- Air Filter Access: The most frequent maintenance task is changing inlet filters. Access should be at floor level without the need for ladders.
- Sound Attenuation: Noise is a significant health and safety concern. Both manufacturers offer sound enclosures reducing noise substantially, but check whether the rating is free-field or piping-connected.
- Voltage Safety: Drives retain high voltage on the DC bus capacitors after shutdown. Lockout/tagout procedures must account for capacitor discharge times, which should be clearly labeled on the enclosure.
Lifecycle Cost Drivers
The total cost of ownership calculation should assume a 15 to 20-year life. Energy consumption will dwarf the initial purchase price.
- Energy: Calculated using the weighted average power draw based on the plant’s flow frequency distribution.
- Maintenance Consumables: Air filters, coolant if liquid-cooled, capacitors for the drive and backup supply, and eventual core overhauls.
- Core Swap: For high-speed turbos, on-site bearing repair is usually impossible. The core, comprising motor, impeller and housing, is swapped out. The cost of a spare core should be factored into the risk analysis.
Comparison Tables
The following tables provide a direct technical contrast between the two primary technology providers and the technologies themselves.
| Manufacturer / Product Line | Primary Technology Focus | Typical Applications | Engineering Strengths | Limitations / Considerations |
|---|---|---|---|---|
| Sulzer HST Series | High-speed turbo with magnetic bearings | Medium to large municipal plants, continuous duty |
|
|
| Atlas Copco ZB Series | Centrifugal turbo with magnetic bearings | Industrial and municipal plants, variable demand |
|
|
| Atlas Copco ZS Series | Rotary screw, positive displacement | SBRs, digesters, industrial high-load |
|
|
| Scenario | Recommended Technology | Key Constraint / Reason | Relative Cost Impact |
|---|---|---|---|
| Large Plant, Steady Base Load | Magnetic bearing turbo (either manufacturer) | Energy efficiency is the dominant driver. Constant operation maximizes the return on high-efficiency turbos. | High capital, lowest operating |
| SBR or Batch Processes (Variable Head) | Rotary screw or hybrid mix | Water level changes create variable backpressure. Turbos may surge or lose efficiency; screws maintain flow stability. | Medium capital, medium operating |
| Small Plant, Limited Maintenance Staff | Rotary screw or positive displacement | Complexity of magnetic bearing electronics may overwhelm local operators. Screw blowers are mechanically understandable. | Low to medium capital, medium operating |
| Digester Gas Mixing / Aeration | Rotary lobe or screw | High pressure, potentially dirty environment, robust operation required over delicate efficiency. | Low capital, higher operating |
| Space Constrained Retrofit | High-speed turbo | Power density. Turbos offer the highest airflow per square foot of floor space. | High capital, offset by construction savings |
Engineer & Operator Field Notes
Real-world reliability is often determined by factors outside the product catalog — specifically, how the equipment is installed, commissioned, and maintained.
Commissioning & Acceptance Testing
- Surge Mapping Verification: During startup, the technician must verify the surge line settings. This involves carefully throttling the machine to ensure the controller detects the approach to surge and initiates the blow-off valve or speed reduction before a surge event occurs.
- Harmonic Analysis: Perform a power quality audit at the drive line side. Verify that total harmonic distortion for voltage and current remains within IEEE 519 limits while the unit is under load. Background plant noise can sometimes trigger drive faults in sensitive high-speed units.
- Temperature Stabilization: Run the unit at full load for at least four hours to verify cabinet cooling effectiveness. Inadequate room ventilation often does not show up until the unit trips on inverter over-temperature during the first heatwave.
Common Specification Mistakes
- Over-Sizing: Engineers often apply safety factors on top of safety factors. This forces the blower to operate at the bottom of its turndown curve during average days, causing instability and poor efficiency. It is better to have a modular design of three smaller blowers than two massive ones.
- Ignoring Inlet Conditions: Specifying flow in standard cubic feet per minute without clarifying site conditions — elevation, humidity, temperature — is a critical error. Blowers compress actual cubic feet per minute. The conversion is significant, especially at high altitudes.
- “Or Equal” Ambiguity: Simply stating “turbo blower” allows air foil, magnetic, and gear-driven units to be bid equally. If the plant maintenance staff is standardized on magnetic bearings, the specification must clearly define active magnetic bearings with backup power to prevent lower-cost alternatives from qualifying.
O&M Burden & Strategy
- Magnetic bearing machines: Routine work is air filter replacement quarterly or semi-annually and cooling fan filter cleaning. Specialized work includes backup power battery replacement every two to four years and capacitor replacement every five to eight years. The burden is very low mechanical labor but requires high-level electrical and controls troubleshooting skills.
- Screw blowers: Routine work is oil level checks, annual oil changes, oil filter replacement, and air filter changes. Long-term work is bearing replacement. The burden is moderate mechanical labor, manageable by general plant mechanics.
Troubleshooting Guide
- Symptom: Blower surging.
Cause: System pressure is higher than the blower can generate at that speed, or flow is too low.
Fix: Check for closed valves downstream, fouled diffusers increasing backpressure, or verify that the dissolved oxygen control loop is not forcing the blower below its minimum speed. - Symptom: High discharge temperature.
Cause: Intake filter clogged, room ventilation failure, or internal cooling loop failure.
Fix: Check filter differential pressure. Verify room HVAC. Clean internal heat exchangers.
Design Details / Calculations
Sizing Logic & Methodology
Engineers must convert process oxygen demand into blower inlet conditions.
- Determine Actual Oxygen Requirement: This comes from the process model based on BOD and ammonia loading.
- Calculate Standard Oxygen Requirement: Correct for site conditions using the alpha factor for wastewater interference, the beta factor for salinity and dissolved solids, and the temperature correction term.
- Convert to airflow in standard cubic feet per minute: Based on the diffuser standard oxygen transfer efficiency, which is depth-dependent. Diffuser efficiency drops as airflow per diffuser increases, so iteration is required between blower sizing and diffuser count.
- Convert to inlet cubic feet per minute: Correct for site elevation, relative humidity, and maximum inlet temperature. Ensure the motor has sufficient horsepower to handle the cold-day scenario with the densest air, even if flow is controlled.
The Blower Room Is Part of the Blower
One category of failure is almost entirely absent from blower comparisons and accounts for a disproportionate share of early trips: the room the machine sits in. A high-speed turbo package rejects a substantial fraction of its input power as heat into the space around it, and it contains power electronics with a defined maximum ambient temperature. Neither manufacturer can protect a machine from a room that was designed as an afterthought.
The provisions that matter are all civil and mechanical, and all cheaper at design than as a retrofit:
- Size the room ventilation from the actual heat rejection of the selected package, at the maximum summer ambient temperature for the site, not from a generic air-changes-per-hour rule. Request the heat rejection figure from the manufacturer in writing and give it to the mechanical designer.
- Separate intake and exhaust so hot discharge air cannot recirculate to the intake. Short-circuiting is the single most common cause of an inverter over-temperature trip that appears only in the first hot week of operation.
- Filter and locate the combustion-free intake away from the headworks and any odor control exhaust. Hydrogen sulfide drawn continuously through an air end and across electronics shortens the life of both.
- Provide for the noise. Sound ratings in submittals are typically free-field at a stated distance; a machine in a small hard-surfaced concrete room will measure higher. If staff will work in the space, plan the treatment rather than discovering the problem at startup.
Specification Checklist
- Performance Standard: Require testing in accordance with ASME PTC 13 for wire-to-air performance, or ISO 1217 where applicable. Do not accept shaft power ratings; they ignore motor and drive losses.
- Harmonic Mitigation: Specify that the drive include active front end or passive filtering to meet IEEE 519 limits at the device terminals.
- Communication: Define the data map explicitly, including flow, discharge pressure, power, speed, surge margin, vibration, and bearing temperature.
- Warranty: For magnetic bearing units, consider requesting an extended warranty on the core, as these are high-cost replacement items.
FAQ Section
What is the main difference between the Atlas Copco ZB and Sulzer HST blowers?
Both are high-speed, magnetic bearing turbo blowers. The primary difference lies in their lineage and packaging. The Sulzer HST is a dedicated wastewater machine known for its robust magnetic bearing design and long history in the sector. Atlas Copco ZB units leverage the company’s industrial compressor background, often featuring highly integrated packaging with proprietary controls. Both are premium efficiency machines, but they use different control philosophies and internal component arrangements.
When should I choose a screw blower over a turbo blower?
Select a screw blower when the application requires operation across a wide range of discharge pressures, such as SBRs with changing water levels, or when the facility has limited electrical troubleshooting capabilities. Screw blowers are positive displacement machines, meaning their efficiency is less sensitive to pressure fluctuations compared to turbo blowers. They are also generally more robust in harsh industrial environments compared to the sensitive electronics of magnetic bearing turbos.
How often do magnetic bearings need to be replaced?
The bearings themselves levitate the shaft, so there is no physical contact and no mechanical wear during operation. However, the auxiliary components supporting them do have a lifespan. The backup landing bearings, used only during power failure, are rated for a specific number of landing events. The capacitors or batteries in the magnetic bearing controller typically require replacement every five to eight years. See the maintenance strategy section above for detail.
Why is wire-to-air efficiency important in blower specifications?
Wire-to-air efficiency measures the total energy consumed by the entire package — drive, motor, cooling fans, filter losses, and compression element — to deliver a specific mass of air. Some manufacturers quote shaft efficiency or isentropic efficiency, which only looks at the compression element and ignores the losses in the motor and drive. Since the drive and motor can account for a meaningful share of losses, wire-to-air is the only way to accurately compare the true electrical cost.
Can I mix different blower technologies in one header?
Yes, this is called hybrid or split-range control. A common and effective strategy is to use a screw blower for the base load or low-flow conditions, due to its stability, and high-speed turbos for peak shaving. This leverages the screw’s pressure robustness and the turbo’s peak efficiency. However, the master control panel must be specifically programmed to manage the handoff between these technologies to prevent surging.
Conclusion
Key Takeaways for Decision Makers
- Efficiency is King: With 20-year lifecycles, a 2% gain in wire-to-air efficiency often justifies a higher initial capital cost.
- Match Tech to Process: Use turbo blowers for steady, high-volume flow. Use screw blowers for variable head or smaller, rugged applications.
- Turndown Matters: Ensure the blower can ramp down to your minimum month flow without venting air.
- Serviceability: Magnetic bearings offer low maintenance but require high-tech support. Screw blowers require oil changes but are mechanically simpler.
- Total Cost: Always evaluate based on energy plus maintenance plus installation, not just bid price.
The choice is rarely a binary decision about which brand is better. It is a specific engineering decision regarding which technology fits the hydraulic profile and maintenance culture of the utility. Sulzer’s HST line remains a benchmark for magnetic bearing reliability in municipal wastewater, while Atlas Copco brings formidable industrial packaging and a diverse portfolio across screw and turbo that allows for hybrid optimization.
Engineers should focus their specifications on the operating envelope, demanding rigorous wire-to-air efficiency guarantees and ensuring that the electrical infrastructure is robust enough to support modern high-speed drives. By prioritizing the system curve over the machine nameplate, utilities can secure a resilient, energy-efficient aeration process that serves reliably for decades.