
Top 10 Inline Grinder Manufacturers for Water and Wastewater
Introduction
In the modern wastewater treatment landscape, ragging has evolved from a nuisance into a critical operational problem. With the proliferation of non-dispersible synthetic wipes and fibrous materials entering collection systems, the reliable operation of downstream pumps, heat exchangers, and centrifuges hangs in the balance. For engineers and operators, the failure of a grinder is not merely a maintenance issue; it often results in pump blockage, sanitary sewer overflows, and regulatory consequences.
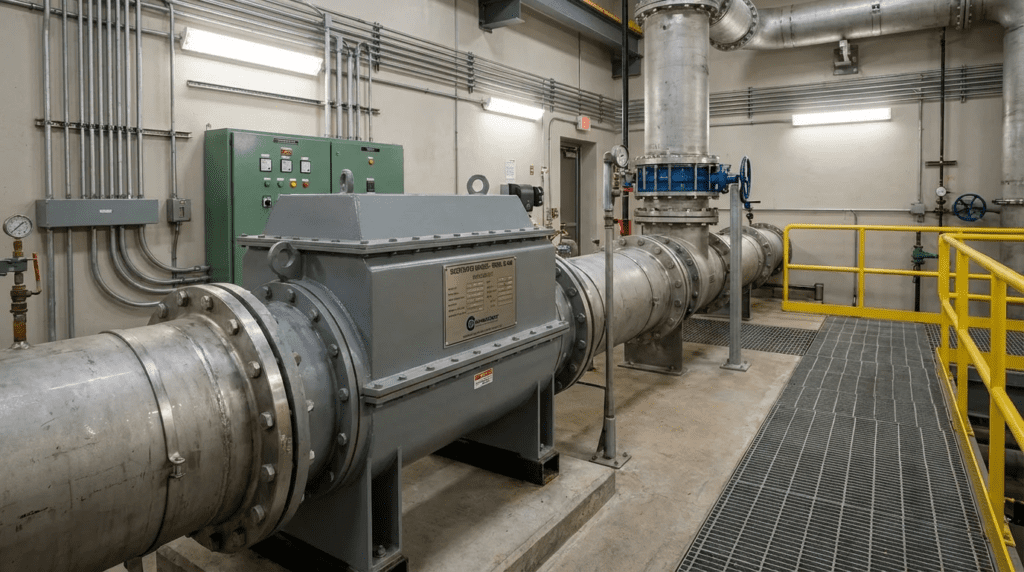
While open-channel grinding is common at headworks, many applications within the plant and at lift stations require closed-piping solutions. This creates a specific demand for robust inline reduction technologies. Selecting the right equipment is difficult, primarily due to the challenge of balancing hydraulic throughput with particle size reduction. An incorrectly specified unit can become a bottleneck, inducing excessive head loss or failing to protect sensitive positive displacement pumps.
This article provides a technical analysis of the inline grinder manufacturers commonly found in municipal and industrial specifications. Beyond a simple list, we explore the engineering mechanics, selection criteria, and specification nuances required to integrate these units effectively.
Two notes on the manufacturer list. First, the entry for a progressive cavity pump manufacturer’s macerator line has been replaced with Moyno, whose inline macerators are an established product in dewatering feed and thickened sludge service. We were unable to confirm a comparable standalone macerator line for the manufacturer previously named here, and a list used to build a bid slate should not carry an unverified entry. Second, the Vogelsang entry now covers both the XRipper twin-shaft grinder and the RotaCut macerator, which are different machines for different duties and were previously conflated.
More broadly, this site carries three overlapping grinder roundups — channel grinders, inline grinders, and a combined guide covering both. The combined guide subsumes the other two, and the set is a consolidation candidate.
This guide sits within our coverage of wastewater grinders. See also our guides to channel grinder manufacturers and residential grinder manufacturers, and our comparison of inline grinder equipment.
How to Select and Specify Inline Grinders
Duty Conditions & Operating Envelope
- Flow Rate vs. Head Loss: Unlike pumps where flow is the output, for grinders flow is a constraint. The manufacturer’s curve must be analyzed to ensure the pressure drop at peak wet weather flow does not starve the downstream pump of net positive suction head.
- Solids Loading: Specifications must distinguish between occasional rags in typical sewage and heavy sludge at 3 to 6 percent total solids. High solids concentrations require higher torque and lower rotational speeds to prevent binding.
- Pressure Rating: Inline units are pressure vessels. While standard housings may be rated for moderate pressure, discharge-side applications often require higher flange ratings. Engineers must verify the pressure rating of the seal housing, not just the cutter chamber.
Materials & Compatibility
- Cutter Hardness: Standard tool steel is often insufficient for grit-laden wastewater. Specifications should call for heat-treated alloy steel or tungsten carbide coated cutters within a defined Rockwell C hardness range.
- Shaft Geometry: Hexagonal shafts are preferred over keyed round shafts. Hex shafts distribute torque load evenly across the cutter faces, minimizing failure points associated with keyway fatigue.
- Housing Materials: Ductile iron is standard for municipal wastewater, but industrial or acidic applications mandate 304 or 316 stainless steel housings to prevent corrosion-induced seal failure.
Hydraulics & Process Performance
- Open Area Ratio: The ratio of the open flow path through the cutter stack to the cross-sectional area of the inlet pipe. A low open area ratio results in high fluid velocities, increased wear, and significant head loss.
- Particle Size Control: Different downstream equipment requires different particle sizes. A centrifugal pump may tolerate coarse solids, while a spiral heat exchanger may require much finer reduction. The tooth count and cutter cam design dictate the final particle size.
Installation Environment & Constructability
- Pipeline Orientation: While many twin-shaft grinders can operate horizontally or vertically, the seal lubrication system must be compatible with the orientation. Vertical installations often require specific seal flush arrangements to prevent air entrapment in the seal chamber.
- Maintenance Access: The design must allow removal of the cutter cartridge without removing the entire body from the pipeline, to minimize downtime and crane requirements.
Reliability, Redundancy & Failure Modes
- Shaft Deflection: Under heavy load, long shafts can deflect, causing cutters to clash. Intermediate shaft supports are required for high-flow, long-stack units.
- Seal Failure: This is the most common failure mode. Cartridge mechanical seals are superior to component seals for ease of replacement. Redundant sealing systems with barrier fluids provide the highest reliability.
- Service Life: In severe sludge applications, cutter stack service life of a few years is typical. Specifications should require guaranteed availability of cutter cartridges.
Controls & Automation Interfaces
- Jam Sensing Logic: The controller must monitor amperage. Upon detecting a spike, it should stop, reverse to clear the obstruction, and retry.
- Progressive Logic: Advanced controllers retry a set number of times before faulting out to protect the motor.
- SCADA Integration: The system must output status and alarms to the central SCADA system via Modbus or EtherNet/IP for remote monitoring.
Maintainability, Safety & Access
- Cutter Cartridge vs. Individual Cutters: Individual cutters allow partial replacement but are labor-intensive to restack. Cartridge designs allow rapid swap-out of the entire element, reducing confined space entry time.
- Auto-Tensioning: Some manufacturers offer auto-tensioning of the cutter stack to compensate for wear, reducing manual tightening intervals.
Lifecycle Cost Drivers
- Energy: High-torque, low-speed grinders are generally energy efficient, but hydraulic losses add indirect energy costs to the main pumps.
- Rebuild Costs: The cost of a cutter exchange program, where the manufacturer swaps a refurbished cartridge for a worn one, should be factored into the lifecycle analysis.
Comparison of Manufacturers and Technologies
Table 1: Manufacturer & Technology Profile
| Manufacturer | Core Technology | Primary Strengths | Typical Applications | Maintenance Profile |
|---|---|---|---|---|
| JWC Environmental (Sulzer) |
Twin-Shaft Low Speed High Torque | Market ubiquity; extensive cutter options; high flow capabilities. | Raw sewage pump stations, sludge lines, institutional waste. | Cartridge and stack exchange programs widely available. |
| Franklin Miller (Taskmaster) |
Twin-Shaft / Cartridge | Cutter cartridge design reduces stack loosening; robust shafting. | Headworks, inline sludge, septage receiving. | Cartridge design simplifies field replacement but requires OEM parts. |
| Vogelsang (XRipper / RotaCut) |
Twin-Shaft / Monolithic plus macerator line | Monolithic ripper rotors eliminate stack tightening; maintenance-in-place access; RotaCut adds an integrated heavy solids trap. | Sludge recirculation, biogas plants, inline sewage. | Rotor replacement is fast; minimal individual parts to manage. |
| Netzsch (N.Mac) |
Twin-Shaft | Integrates with progressive cavity pumps; shock absorption systems for hard solids. | Sludge feed to dewatering, digester recirculation. | Designed for modular maintenance; cutters replaceable without full disassembly. |
| Börger (Multichopper) |
Macerator & Twin-Shaft | Maintenance-in-place design; reversible cutting plates; adjustable tension. | Biogas substrates, sludge thickening, sensitive pump protection. | Quick-release covers allow rapid access to wear parts. |
| Moyno (Macerator) |
Inline Macerator | Designed to protect progressive cavity pumps; integrated control logic. | Dewatering feed, thickened sludge. | Head plate and cutter replacement is straightforward inline. |
| Landia | Chopper Pumps / Knife Systems | Aggressive chopping technology with heavy slurry and agricultural crossover experience. | Heavy sludge, digester mixing loops, lift stations. | External knife adjustment systems available on some models. |
| NOV Mono (Muncher) |
Twin-Shaft | Slow speed; proprietary cutter geometry for fine grinding; energy efficient. | Small to medium lift stations, packaged plants. | Standard individual cutter stack design; long performance history. |
| Hydro-Dyne Engineering | Twin-Shaft | Heavy-duty construction; custom fabrication capabilities for tight spaces. | Headworks screening bypass, septage receiving stations. | Uses standard bearing and seal arrangements for serviceability. |
| Wangen (X-Unit) |
Foreign Object Separator + Cutting | Combines stone and heavy object separation with cutting; protects against catastrophic damage. | Biogas, difficult industrial wastewater, manure processing. | Split process: removal of non-grindables first, then cutting. |
Table 2: Application Fit Matrix
| Application Scenario | Primary Constraint | Best-Fit Technology | Why | Key Spec Requirement |
|---|---|---|---|---|
| Raw Sewage Lift Station | High Flow / Ragging | Twin-Shaft | Must pass high volume of liquid while shredding wipes. | Low head loss design |
| Sludge Recirculation | High Solids / Viscosity | Twin-Shaft or Macerator | Thick sludge requires high torque; hair and fiber need shearing. | Hex shafting; hardened cutters |
| Centrifuge or Press Feed | Particle Size Control | Macerator (perforated plate) | Needs uniform small particle size to prevent nozzle clogging. | Defined output size |
| Septage Receiving | Rocks / Debris | Twin-Shaft with Rock Trap | Rocks will destroy cutters; separation is required. | Integrated heavy object trap |
| Small Package Plant | Budget / Space | Comminutor / Single Shaft | Lower duty cycle; smaller footprint. | Simple controls |
Engineer and Operator Field Notes
Commissioning & Acceptance Testing
- Rotation Logic Check: Do not assume the reverse function works. Physically witness the shafts stop and reverse direction upon simulated jam. Verify the time delay between forward, stop, and reverse to prevent high current inrush from damaging the drive or starter.
- Dry Run Limits: Most inline grinders rely on the process fluid for seal lubrication. Ensure the contractor does not dry-run the unit for rotation checks for more than a few seconds, or seal faces may crack due to thermal shock.
- Amp Draw Baseline: Record the amperage draw with clean water. This establishes the baseline no-load condition against which future maintenance decisions are made.
O&M Burden & Strategy
- Cutter Stack Tightening: For designs with individual cutters, the stack will loosen over time due to vibration and wear. A loose stack allows cutters to wobble, damaging the hex shaft. Schedule a torque check annually.
- Seal Inspection: Inspect the seal chamber barrier fluid monthly. Milky fluid indicates water intrusion; low fluid indicates a leak to the process.
- Spare Parts Inventory: If you do not have a redundant unit, a spare cutter cartridge is a mandatory shelf item. Lead times for new cartridges can be lengthy.
Troubleshooting Guide
- Symptom: Frequent reversing without obvious cause.
Root Cause: Often soft rags wrapping around the shaft rather than a hard object. Alternatively, the amperage trip setpoint may be too close to the running amperage.
Solution: Inspect the stack for wrapping. If clean, adjust the jam timer delay slightly to allow momentary spikes to pass. - Symptom: Excessive noise or vibration.
Root Cause: Bearing failure or a bent shaft.
Solution: Perform vibration analysis. If the frequency matches shaft speed, it is likely imbalance or a bent shaft. If high frequency, suspect bearings.
Design Details and Calculations
Sizing Logic & Methodology
- Determine peak wet weather flow: this is the critical design point.
- Calculate velocity through the grinder open area, not the flange area. Velocity should generally be kept below 6 to 8 ft/s to prevent excessive head loss and abrasive wear.
- Check head loss: consult the manufacturer’s specific curve. Ensure that at peak flow, the head loss does not reduce suction pressure at the pump below the required net positive suction head plus a safety margin.
The Bypass Is Part of the Grinder
An inline grinder differs from a channel grinder in one respect that governs the whole installation: it sits inside a closed pipe, so when it blinds there is nowhere for the flow to go. A channel grinder that blinds raises the upstream water level and, if the designer has provided an overflow weir, the flow passes around it. An inline grinder that blinds simply stops the line.
Every inline grinder therefore requires a valved bypass loop, and the bypass is not an optional refinement:
- Isolation valves on both sides plus a bypass leg, so the unit can be removed for cutter service without taking the process down. Without this, a two-hour cartridge swap becomes a plant outage.
- Differential pressure monitoring across the unit, alarmed to SCADA. Rising differential pressure is the only early warning of a blinding stack, and on the suction side of a pump it is also the leading indicator of impending cavitation.
- Consideration of what happens on power loss. A de-energized grinder is a restriction in the line. If the pump can run while the grinder cannot, the interlock must stop the pump or open the bypass.
Engineers should also confirm that the bypass leg is actually operable by the staff who will need it, at the hour they will need it. A bypass valve at the back of a crowded pipe gallery, reachable only by ladder, is a bypass in drawing only.
Specification Checklist
- Cutter Material: heat-treated alloy steel, surface hardened to a defined Rockwell C range, or tungsten carbide.
- Shaft Construction: hexagonal shafting with a defined minimum tensile strength.
- Seal Configuration: cartridge-style mechanical seals rated above maximum system pressure.
- Controller: NEMA 4X enclosure with PLC-based jam sensing, auto-reverse, and fail-safe alarm contacts.
- Testing: manufacturer to provide certified head loss curves based on water testing.
Standards & Compliance
- NEC / NFPA 70 and NFPA 820: if the grinder is located in a screen room or wet well, the motor and cabling must carry the appropriate hazardous location rating.
- IP Ratings: for washdown environments, IP68 motors are preferred even for dry-pit installations to protect against accidental flooding.
- Build America, Buy America: for federally funded projects, verify domestic sourcing compliance at submittal review.
Frequently Asked Questions
What is the difference between an inline grinder and a macerator?
Inline grinder typically refers to twin-shaft slow-speed units that use counter-rotating cutters to shred solids. These handle high flows and tough solids such as wipes and wood. A macerator often refers to a unit with a perforated plate and a rotating cutting blade. Macerators provide a finer, more consistent particle size but generally have higher head loss and are better suited to sludge or lower-flow applications.
How do you calculate head loss for an inline grinder?
Head loss cannot be calculated using standard pipe friction formulas because the geometry is complex. It must be derived from the manufacturer’s empirical data curves. Factors influencing this include the cutter tooth profile, the open area ratio, and the viscosity of the fluid. Always request a curve adjusted for your specific solids concentration.
How often do cutter stacks need to be replaced?
Cutter life varies heavily by application and grit load. In standard municipal raw sewage, stacks last several years; in abrasive or heavy sludge applications, considerably less. Tungsten carbide cutters can extend life in abrasive applications but increase initial capital cost. Trend the amperage and monitor cutter gap rather than working to a fixed calendar interval.
What is the best way to prevent grinder jamming?
The primary defense is a robust auto-reverse controller. When a hard object is encountered, the current spikes and the unit reverses to reposition the object. However, the best prevention is upstream protection. Installing a rock trap or coarse screen before the grinder prevents non-grindables from reaching the cutters, which is the leading cause of destructive jams.
Can inline grinders be installed vertically?
Yes, most manufacturers offer units capable of vertical installation, but this must be specified during ordering. Vertical units often require different seal flushing arrangements to prevent air pockets forming in the upper seal housing, which would lead to dry running and seal failure.
How much does a municipal inline grinder cost?
Costs vary widely by size, materials, control complexity, and hazardous location requirements, and equipment pricing in this category has moved substantially with material markets. Obtain current quotations rather than relying on published ranges, and remember that installation and electrical integration are separate costs that frequently approach the equipment cost itself.
Conclusion
KEY TAKEAWAYS
- Hydraulics First: Never ignore head loss. Ensure the grinder does not starve downstream pumps.
- Application Matters: Use twin-shaft grinders for raw sewage and wipes; use plate macerators for defined particle size in sludge and dewatering feed.
- Material Selection: Specify hex shafts and hardened alloy or tungsten cutters for longevity.
- Control Logic: Auto-reverse logic is mandatory for protecting the motor and clearing soft jams.
- Lifecycle Approach: Evaluate the cost of replacement cartridges over the asset life, not just the initial bid price.
Selecting inline grinder equipment is a critical engineering task that directly impacts plant reliability. The market offers a range of technologies, from the twin-shaft designs of JWC and Franklin Miller to the maintenance-friendly monolithic rotors of Vogelsang and the precision macerators used ahead of dewatering equipment.
For the specifying engineer, the goal is to match the machine’s mechanical limitations with the fluid’s hydraulic reality. By focusing on open area ratios, seal technology, and ease of maintenance access, engineers can design systems that protect expensive downstream assets without becoming maintenance burdens themselves. Prioritize manufacturers who provide transparent head loss data and robust local support for cutter cartridge exchange.