Metering Pumps Seal Failures: Causes
Introduction
In municipal water treatment and industrial wastewater processing, the chemical metering pump is often the smallest piece of rotating equipment with the highest disproportionate impact on process reliability. When a main lift pump fails, redundancy often covers the gap. When a chemical metering pump fails, regulatory compliance regarding disinfection, coagulation, or pH adjustment is immediately compromised. Among the various failure modes, seal integrity—whether referring to the dynamic packing of a plunger pump or the static/flexing barrier of a diaphragm pump—remains the primary source of unplanned downtime.
Engineers and operators frequently treat seal failures as simple maintenance nuisances, swapping out parts without investigating the root cause. However, a deeper analysis of Metering Pumps Seal Failures: Causes reveals that the vast majority are not due to defective components, but rather result from system-level errors in hydraulic design, material selection, or suction-side piping geometry. In water and wastewater utilities, these pumps handle aggressive fluids ranging from off-gassing sodium hypochlorite and viscous polymers to abrasive lime slurries and corrosive ferric chloride. The operating environment is harsh, and the tolerance for leakage is effectively zero.
Proper selection and specification are the first lines of defense. If the interaction between fluid acceleration, vapor pressure, and elastomer compatibility is not calculated correctly during the design phase, the pump is destined for chronic failure. This article serves as a technical guide for engineers and plant managers to understand the physics and chemistry behind seal compromises, moving beyond symptom management to permanent reliability improvements. Metering pumps occupy a distinct niche within the broader family of pumps for wastewater: they are sized for accuracy rather than throughput, and that difference in purpose is precisely why their failure modes look nothing like those of the transfer and lift equipment operating alongside them.
Metering Pump Subcategories
Seal reliability cannot be assessed in isolation from pump architecture, chemical service, and specification practice, because each of those determines which sealing arrangement is present in the first place. The three subcategories below organize the metering pump topic and each carries its own detailed coverage. Read them as the context around everything that follows: a failure analysis is only useful once you know which technology is installed, what it is dosing, and how it was specified.
Metering Pump Types and Drive Technologies
The fundamental division in metering pump design is how reciprocating motion reaches the process fluid. Mechanical diaphragm pumps connect the diaphragm directly to a driven rod, which is simple and inexpensive but concentrates fatigue stress at the connection point. Hydraulic diaphragm designs interpose an oil chamber so the diaphragm is pressure-balanced rather than mechanically strained, which is what allows them to reach pressures an order of magnitude higher with far longer diaphragm life. Plunger and piston pumps abandon the diaphragm entirely in favour of dynamic packing, trading leak-free containment for pressure capability. Our guide to the diaphragm metering pump covers these drive architectures in detail, along with dosing pump variants, stroke adjustment mechanisms, and the accuracy and repeatability each configuration can realistically deliver. The sealing mechanism follows from the drive choice, not the other way around, which is why architecture selection is the first and most consequential decision in any chemical feed design.
Chemical Metering Pumps and Service-Specific Selection
The chemical being dosed governs materials, valve design, and often the pump technology itself. Sodium hypochlorite off-gasses and crystallizes; polymers are viscous and shear-sensitive; lime slurry is abrasive; sulfuric acid is aggressive and reacts exothermically with water. Each of these behaviours attacks a different part of the pump, and a configuration that performs faultlessly on one will fail rapidly on another. Our chemical metering pumps for water treatment selection guide works through the common water and wastewater chemicals service by service, covering wetted material selection, valve and seat configuration, degassing arrangements, and the containment measures appropriate to each hazard class. It also addresses the specific pumps built for individual duties, including hypochlorite and peroxide dosing, where standard equipment routinely disappoints. The chemical resistance chart is a starting point in that work, never the conclusion, because concentration and temperature shift compatibility substantially.
Specification, Operations, and Performance
The third subcategory covers what happens between the datasheet and the running pump: how to write a specification that produces a reliable installation, how to read and use a metering pump curve, and how to select materials of construction for the piping and pump body rather than just the elastomers. Our guide to specifying metering pumps for municipal lift stations covers the specification process end to end, including duty point definition, turndown requirements, control interface, and the accessories that protect the pump from its own pressure pulses. Related coverage in this group addresses pump curve interpretation for operators and the cast iron, stainless, and duplex materials decision in wastewater service. Most of the failures described later in this article were designed in at this stage, which makes specification the highest-leverage point of intervention available.
How to Select / Specify for Seal Reliability
Preventing seal failure begins at the specification stage. The “seal” in a metering pump is inextricably linked to the pump’s hydraulic performance and chemical environment. Engineers must specify not just a flow rate, but a complete operating context.
Duty Conditions & Operating Envelope
Defining the duty point is insufficient for reciprocating pumps. The pulsating nature of metering pumps creates peak pressures and velocities that far exceed the average values.
- Pressure Transients: Unlike centrifugal pumps, metering pumps generate pressure pulses. If the discharge pressure exceeds the pump’s rating due to a closed valve or line blockage, the weakest point—often the seal or diaphragm—will fail. Specifications must include relief valve settings and pulsation dampener requirements to protect seals from pressure spikes.
- Turndown Ratios: Running a pump at extremely low stroke lengths (e.g., below 10-15%) can cause loss of prime and erratic movement of internal valves, leading to chatter that damages seats and seals. Specify pumps that maintain linearity across the required turndown range without hydraulic instability.
- Temperature Variations: Elastomers have distinct thermal limits. A seal that functions perfectly with 15°C coagulant may swell or extrude when pumping a chemical that has been heated by the sun in an outdoor tank farm.
Materials & Compatibility
Chemical incompatibility is a leading contributor to Metering Pumps Seal Failures: Causes. The “like-for-like” replacement strategy often perpetuates the original specification error.
- Elastomer Swelling vs. Embrittlement: Different chemicals attack seals differently. Solvents may cause EPDM to swell and seize, while acids might cause FKM (Viton) to harden and crack. Manufacturers’ resistance charts are a starting point, but they rarely account for proprietary chemical blends or elevated temperatures.
- Composite Diaphragms: For aggressive service, specify composite diaphragms (usually a PTFE face with an elastomer backing). The PTFE provides chemical resistance, while the elastomer provides structural flexibility. Delamination between these layers is a common failure mode if the vacuum sizing is incorrect.
- Abrasion Resistance: For lime slurries or activated carbon, standard O-rings will be destroyed quickly. Specify ball valves with wider clearances and seals made from abrasion-resistant materials like Alumina Ceramic or specialized urethanes.
Hydraulics & Process Performance
The hydraulic environment on the suction side is where most seal failures originate, even if the leak appears on the discharge side.
- Acceleration Head (Ha): This is the pressure required to accelerate the fluid in the suction line during the start of the stroke. If Ha lowers the pressure below the fluid’s vapor pressure, cavitation occurs. The collapsing vapor bubbles erode seals and diaphragms violently.
- NPSH Available vs. Required: While critical for all pumps, it is nuanced for metering pumps. NPSHr values from manufacturers are often based on water. Viscous fluids (polymers) or volatile fluids (hypo) require significantly higher margins to prevent cavitation-induced seal damage.
Installation Environment & Constructability
Physical installation constraints often force piping geometries that doom seals to failure.
- Flooded Suction: Whenever possible, specify flooded suction. Lifting fluid with a reciprocating pump increases vacuum on the suction side, stressing diaphragms and inviting air ingress past plunger packing.
- Maintenance Access: Seals are wear parts. If a pump is installed against a wall or beneath piping such that the liquid end cannot be easily removed, maintenance crews may overtighten bolts to stop leaks rather than replacing the seal, warping the head and causing permanent leakage paths.
Reliability, Redundancy & Failure Modes
Engineering for failure involves acknowledging that seals will eventually wear out and designing the system to mitigate the impact.
- Leak Detection: For critical chemicals, specify double-diaphragm pumps with integrated leak detection (pressure switch or conductivity probe). This allows the pump to contain the fluid even after the primary seal fails, triggering an alarm rather than a spill.
- Run-Dry Protection: Many seal failures occur when a tank runs empty, and the pump runs dry, generating friction heat that destroys O-rings and packing. Integrate low-level tank switches into the pump control logic.
Controls & Automation Interfaces
The control strategy impacts seal life. Rapid start/stop cycling (e.g., from a rigid ON/OFF control loop) accelerates wear on dynamic seals and fatigues diaphragms.
- VFD vs. Stroke Adjustment: Using a Variable Frequency Drive (VFD) to slow the motor is generally gentler on seals than mechanical stroke adjustment, as it reduces the frequency of the pressure pulses.
- Ramping Functions: Program PLCs to ramp pumps up and down rather than hard-starting them. This reduces “water hammer” effects on the check valve seals.
Maintainability, Safety & Access
Safety is paramount when dealing with seal failures involving hazardous chemicals.
- Shielding: Specify spray shields for pump heads. When a seal fails under pressure, it can spray corrosive chemicals several feet.
- Isolation Valves: Ensure true union ball valves are installed immediately upstream and downstream to facilitate quick, safe removal of the liquid end for bench repair.
Lifecycle Cost Drivers
Cheap pumps often have expensive seals. A solenoid pump may cost $500 but require $200 rebuild kits every 3 months in difficult service. A motor-driven hydraulic diaphragm pump may cost $3,000 but run for 5 years without a seal change. Analyze the Total Cost of Ownership (TCO) based on maintenance intervals, not just initial CAPEX.
Comparison of Metering Pump Technologies
The following tables provide an engineering comparison of common metering pump architectures and their respective sealing mechanisms. Understanding the inherent strengths and weaknesses of each type is essential for selecting the right equipment for the application.
It helps to place these architectures in context first. Metering pumps are a precision subclass of positive displacement pumps, sharing the fixed-volume-per-cycle principle but adding stroke adjustment and the accuracy requirements that define the category. Two adjacent technologies appear repeatedly in the tables below because they compete for the same duties: peristaltic pumps, which eliminate dynamic seals and check valves entirely by making the hose itself the pressure boundary, and air-operated diaphragm pumps, which share the diaphragm principle but trade metering accuracy for solids handling and self-priming capability. Where dosing accuracy is not the controlling requirement, one of those alternatives is frequently the more durable answer.
| Technology Type | Sealing Mechanism | Primary Seal Failure Mode | Best-Fit Applications | Limitations |
|---|---|---|---|---|
| Mechanical Diaphragm | Flexible diaphragm mechanically connected to a reciprocating rod. Static O-rings at head. | Fatigue/Rupture: Stress concentration at the connection point. High suction pressure can distend the diaphragm. | General purpose water/wastewater chemicals (Alum, dilute acids). Low pressure (< 150 psi). | Limited pressure capability. Diaphragm is the weak link. Not suitable for high viscosities. |
| Hydraulic Diaphragm | Diaphragm is hydraulically balanced (oil on one side, process fluid on other). No mechanical stress concentration. | Oil Contamination/Drift: Leakage of internal relief valve or oil past the piston seal affects diaphragm stroke. | Critical process duty, high pressures (> 3000 psi possible), hazardous chemicals requiring leak containment. | Higher CAPEX. Requires monitoring of hydraulic oil level and condition. |
| Plunger / Piston | Dynamic packing (Chevron, braided, or injectable) around a reciprocating plunger. | Abrasive Wear/Leakage: Packing wears over time. Requires controlled leakage for lubrication (in some designs). | High pressure, high temperature, or clean fluids where slight leakage is managed. | Not leak-free. Requires regular packing adjustment. Not for hazardous/toxic fluids without containment. |
| Peristaltic (Hose) | No dynamic seals or valves. The hose is the seal. | Hose Fatigue: The hose eventually fails due to repeated compression cycles. | High solids (Lime), viscous fluids (Polymers), off-gassing fluids (Hypo). | Limited pressure. Hose rupture can be catastrophic without leak detection. Flow pulsation is significant. |
| Solenoid Diaphragm | Electromagnetically driven shaft acting on a diaphragm. | Heat/Fatigue: Solenoid heat can degrade elastomers. Short stroke invites vapor locking. | Low flow, non-critical dosing. Commercial/light industrial. | Low durability. “Throw-away” liquid ends. Poor handling of off-gassing fluids. |
| Application Scenario | Primary Seal Challenge | Recommended Material/Design Strategy | Maintenance Watch-Out |
|---|---|---|---|
| Sodium Hypochlorite (Hypo) | Off-gassing: Vapor lock causes dry running. Crystallization: Salt builds up on check valve seals. | High-velocity pump heads to pass gas bubbles. PTFE or specialized composite diaphragms. Degassing valves. | Check valves require frequent cleaning of crystallized salts. Inspect for “checking” (cracking) on elastomer seals. |
| Polymers (Emulsion/Mannich) | Shear Sensitivity & Viscosity: High viscosity prevents check balls from seating, causing backflow/erosion. | Spring-loaded ball checks to force seating. Oversized ports. Peristaltic pumps preferred for shear sensitivity. | Cleaning polymer spills is difficult. Seal leaks often result in massive, slippery messes. Avoid plunger pumps. |
| Lime Slurry | Abrasion: Particles embed in soft seals, turning them into sandpaper against mating surfaces. | Peristaltic pumps or Diaphragm pumps with hardened seats/balls. Avoid soft O-rings in flow path. | Sedimentation occurs if flow stops. Flushing lines is mandatory. Seals fail rapidly if pump runs against a clogged line. |
| Sulfuric Acid | Exothermic Reaction/Heat: Water mixing creates heat. Strong chemical attack. | PTFE / Teflon liquid ends. Viton (FKM) usually acceptable depending on concentration. | Safety is critical. Acid leaks do not evaporate; they concentrate. Double containment is standard. |
Engineer & Operator Field Notes
Real-world reliability is often determined by the practices employed during commissioning and daily operation. The following notes highlight practical steps to mitigate Metering Pumps Seal Failures: Causes.
Commissioning & Acceptance Testing
The Site Acceptance Test (SAT) is the best time to catch hydraulic issues that kill seals.
- Calibration Column Verification: Do not rely solely on the pump’s dial setting. Use a suction-side calibration column to verify actual flow. If the pump is delivering significantly less flow than the curve suggests, it may be experiencing cavitation or high backpressure—both of which stress the seals.
- Water vs. Chemical Commissioning: Most pumps are tested with water at the factory. When introducing the process chemical, retorque the head bolts after 24 hours of operation. Elastomers “take a set” (relax) after initial compression and thermal cycling, leading to leaks if not retightened.
- Relief Valve Setting: Verify the external pressure relief valve (PRV) is set at 10-15% above the system operating pressure, but below the pump’s maximum rated pressure. A blocked discharge line without a functional PRV will inevitably rupture the diaphragm or blow out a gasket.
Common Specification Mistakes
- Oversizing the Pump: Engineers often apply a 2x safety factor, then the plant operates at 50% capacity. The pump ends up running at 10-15% stroke length. At this short stroke, the diaphragm movement is minimal, leading to poor check valve seating and erratic forces on the seals. Target normal operation between 70% and 90% of pump capacity.
- Ignoring Pipe Stress: PVC piping is rigid. If the suction or discharge piping is forced into alignment with the pump head, that stress is transferred to the pump casing and seals. Over time, vibration causes the plastic threads or mating surfaces to crack. Use flexible connectors or expansion joints immediately adjacent to the pump.
- Missing Pulsation Dampeners: On long discharge runs, the inertial mass of the fluid resists the pulsating flow. Without a dampener, the pressure spike at the peak of the stroke can be 3-4 times the average system pressure, blowing out seals instantly.
O&M Burden & Strategy
- Diaphragm Replacement: Do not wait for failure. Implement a time-based replacement schedule. For benign chemicals, 12-18 months is typical. For aggressive chemicals (hypo, acids), 6-12 months is safer.
- Torque Specifications: “Hand tight plus a quarter turn” is not a specification. Metering pump heads, especially plastic ones (PVC/PVDF), are sensitive to torque. Uneven tightening warps the head, creating leak paths. Use a torque wrench and follow the star pattern recommended by the OEM.
- Check Valve Maintenance: The balls and seats are the “heart valves” of the pump. If they leak, the pump loses efficiency. Often, a “seal failure” is actually a check valve failure that caused the pump to run erroneously, generating heat or vibration that subsequently damaged the main seal.
Troubleshooting Guide
- Symptom: Leakage at the Pump Head Mating Surface.
Root Cause: Loose bolts, warped head from over-torquing, or worn O-ring.
Action: Check bolt torque. If correct, disassemble and inspect head flatness. Replace O-ring. - Symptom: Diaphragm Rupture (Process Fluid in Oil/Gearbox).
Root Cause: Discharge over-pressure, closed valve, or natural fatigue life exceeded.
Action: Check discharge line for blockages. Verify PRV functionality. Check age of diaphragm. - Symptom: Loud Banging/Knocking Noise.
Root Cause: Cavitation or Water Hammer. This kills seals via shock waves.
Action: Check suction pressure (NPSHa). Install pulsation dampener. Check for starved suction line. - Symptom: Flow Declines Gradually Over Weeks at a Fixed Setting.
Root Cause: Check valve seat wear or crystallization, worn ball, or a slowly failing diaphragm losing effective displacement.
Action: Verify against a calibration column before adjusting the stroke. Increasing stroke to compensate masks the fault and accelerates the underlying wear. - Symptom: Pump Runs but Delivers Nothing After a Tank Change.
Root Cause: Vapor lock or loss of prime, common with off-gassing chemicals and suction lift installations.
Action: Vent the liquid end and verify suction line integrity. Repeated occurrences indicate the installation needs flooded suction or a degassing head rather than a repair.
Design Details & Hydraulic Calculations
To prevent Metering Pumps Seal Failures: Causes rooted in hydraulics, engineers must perform specific calculations during the design phase. The most critical oversight is typically Acceleration Head.
Sizing Logic & Methodology
Unlike centrifugal pumps where flow is continuous, reciprocating pumps stop and start the fluid column on every stroke. This requires overcoming the inertia of the liquid.
Calculating Acceleration Head (Ha)
Acceleration head is the pressure fluctuation due to the acceleration and deceleration of the fluid in the suction line. If Ha is high enough to drop the suction pressure below the fluid’s vapor pressure, the fluid flashes to vapor (cavitation). The subsequent collapse of bubbles tears at the diaphragm and seals.
The Formula (Standard API 675):
- L: Length of suction pipe (feet).
- V: Velocity in suction pipe (ft/sec).
- N: Pump speed (strokes per minute).
- C: Constant (depends on pump type, e.g., 0.6 for simplex single-acting).
- g: Gravity (32.2 ft/sec²).
- K: Fluid compressibility factor (usually 1.4 for water/chemicals).
Design Implication: To reduce Ha and save the seals:
- Shorten the suction line length (L).
- Increase the suction pipe diameter to reduce velocity (V).
- Slow down the pump speed (N).
- Install a suction-side pulsation dampener (effectively reduces L to near zero).
Reading the result: the calculated acceleration head is subtracted from available suction pressure alongside static lift and friction loss. Because Ha scales linearly with suction line length, pipe velocity, and stroke rate, the three variables compound rather than trade off: a long, undersized suction line on a fast-stroking pump can produce an acceleration head several times the static suction head available, which is how a pump on flooded suction still manages to cavitate. Run the calculation before finalizing pump room layout, because suction line length is nearly impossible to change once the equipment is set.
Specification Checklist
Ensure your specification document includes these critical items to protect pump integrity:
- Viscosity Correction: If fluid viscosity > 50-100 cP, require the manufacturer to provide correction factors for valve sizing.
- Vapor Pressure Margin: Require that NPSHa > NPSHr + 5 feet (or more for volatiles).
- Material Certifications: For critical seals (Kalrez, Chemraz), require certification of material authenticity, as counterfeit elastomers are common.
- Testing: Specify a hydrostatic test of the pump head at 1.5x design pressure to ensure static seal integrity before shipment.
- Acceleration Head Calculation: Require the supplier or designer to submit the Ha calculation for the as-built suction piping arrangement, not for an idealized short run.
- Turndown and Accuracy: State the required turndown ratio and the steady-state accuracy to be maintained across it, so the pump is not sized to a single duty point it will rarely occupy.
- Protective Accessories: Specify relief valve, back pressure valve, pulsation dampener, calibration column, and isolation valves as part of the pump package rather than leaving them to the installing contractor.
Standards & Compliance
- API 675: The gold standard for heavy-duty industrial metering pumps. Defines linearity, repeatability, and steady-state accuracy.
- Hydraulic Institute (HI 7.1-7.5): Covers nomenclature, definitions, applications, and operation of metering pumps.
- NSF/ANSI 61: Mandatory for any wetted parts (including seals and diaphragms) in potable water applications.
API 675 defines the three performance terms that get used interchangeably and should not be. Steady-state accuracy is how close delivered flow sits to the set point under constant conditions. Linearity is how closely the flow-versus-setting relationship holds across the turndown range. Repeatability is how consistently the pump returns to the same flow at the same setting. A pump can be highly repeatable and still inaccurate, which is why calibration column verification is not optional and why a vendor quoting a single accuracy percentage has not answered the question.
Frequently Asked Questions
What are the primary Metering Pumps Seal Failures: Causes?
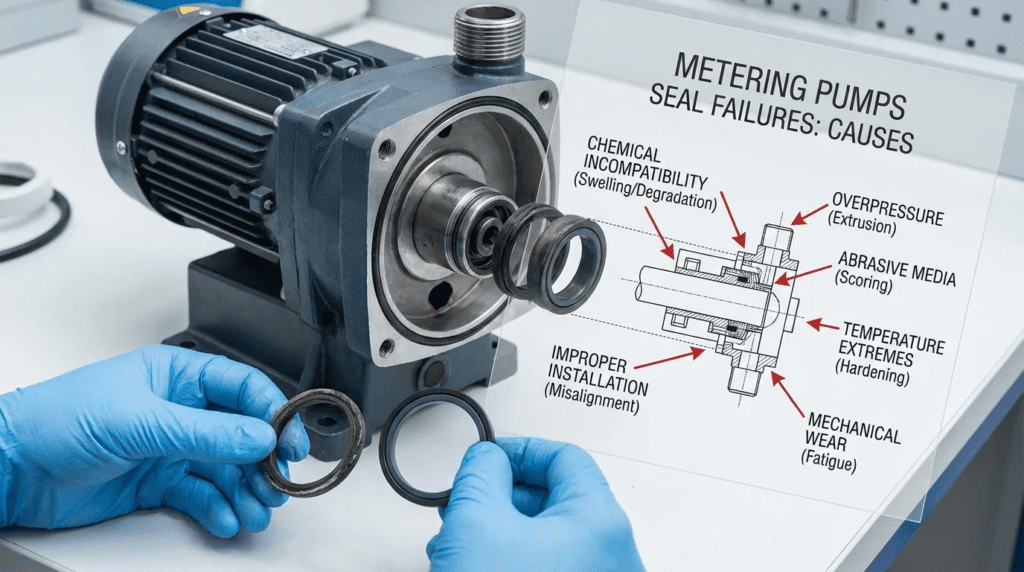
The most common causes include chemical incompatibility (swelling/cracking), excessive discharge pressure causing rupture, cavitation due to poor suction conditions, thermal damage from dry running, and improper installation (piping stress). In many cases, “seal failure” is actually a symptom of poor hydraulic design, specifically ignoring acceleration head requirements.
How does acceleration head affect metering pump seals?
Acceleration head creates pressure fluctuations in the suction line. If the pressure drops too low, the fluid vaporizes (cavitates). When these vapor bubbles collapse inside the pump head, they release intense localized energy that pits metal surfaces and tears elastomer diaphragms and seals. Reducing suction line length or adding pulsation dampeners mitigates this.
What is the typical lifespan of a metering pump diaphragm?
In standard water treatment applications (e.g., Alum, dilute Caustic), a high-quality diaphragm typically lasts 12 to 24 months. In harsh applications (Sodium Hypochlorite, Sulfuric Acid), lifespans may drop to 6 to 12 months. Manufacturers often recommend annual replacement as a preventive measure regardless of visual condition.
What is the difference between a dynamic seal and a static seal in metering pumps?
A static seal (like an O-ring on a pump head or a diaphragm clamped at the rim) does not move relative to the mating surface; it fails due to compression set or chemical attack. A dynamic seal (like plunger packing) moves against a surface; it fails due to friction, abrasion, and wear. Diaphragm pumps are generally preferred for hazardous chemicals because they lack dynamic seals that can leak to the atmosphere.
Why do sodium hypochlorite pumps frequently experience seal and check valve failure?
Sodium hypochlorite tends to “off-gas,” creating vapor locks that cause the pump to run dry, generating heat that damages seals. Additionally, when the fluid dries, it crystallizes into sharp salts that cut elastomers and prevent check balls from seating properly. Using special “off-gassing” pump heads and rigorous flushing protocols helps prevent this.
How do I select the right elastomer for metering pump seals?
Consult chemical resistance charts specifically for the concentration and temperature of your fluid. Common materials include EPDM (good for caustics, bad for oils), Viton/FKM (good for acids, bad for ketones), and PTFE (universally resistant but less elastic). Be aware that temperature changes can alter chemical resistance properties significantly.
When should I use a double diaphragm pump?
Double diaphragm pumps are recommended for highly hazardous, toxic, or expensive chemicals. The space between the two diaphragms is monitored by a sensor. If the primary diaphragm fails, the chemical is contained by the secondary diaphragm, and the sensor triggers an alarm, preventing an external spill and allowing for safe shutdown.
Why does an oversized metering pump fail more often than a correctly sized one?
An oversized pump is forced to run at a very short stroke to deliver the required dose. At short stroke, diaphragm displacement is small relative to the volume of the pump head, so check balls may not lift and seat cleanly, and the fluid column receives sharp, brief acceleration pulses rather than smooth movement. The result is valve chatter, poor priming, and erratic loading on the diaphragm and seals. Target normal operation between roughly 70% and 90% of rated capacity, and if a wide dosing range is genuinely required, achieve it through speed control rather than through extreme stroke reduction.
Do I need both a back pressure valve and a relief valve?
They solve different problems and most installations need both. A back pressure valve maintains a minimum resistance on the discharge side so the pump meters accurately and does not siphon when injecting into a line at low or negative pressure. A pressure relief valve protects the pump from over-pressure if the discharge is blocked or a valve is closed, and it is the single accessory most directly responsible for preventing diaphragm rupture. Neither substitutes for the other, and a relief valve set above the pump’s rated pressure provides no protection at all.
How should chemical feed pumps be handled when a tank is changed or a line is flushed?
Tank changeover and flushing are among the highest-risk routine activities for seal life because they introduce air, dry-running, and sometimes incompatible flush fluids. Stop the pump before the tank runs dry rather than after, vent the liquid end when the new tank is connected, and confirm prime against a calibration column before returning to automatic control. For crystallizing chemicals such as hypochlorite and lime, flush with compatible water on a defined schedule instead of waiting for a flow decline, since deposits that form on check seats are far easier to prevent than to remove.
Conclusion
Key Takeaways
- Hydraulics Matter Most: Most “seal” failures are actually suction piping failures. Calculate NPSHa and Acceleration Head (Ha) for every application.
- Chemical Context: A seal material compatible at 20°C may fail at 40°C. Consider the full range of operating temperatures and concentrations.
- Preventive Maintenance: Replace diaphragms and seals on a schedule (e.g., annually) rather than running to failure. The cost of a rebuild kit is negligible compared to process downtime.
- Installation Hygiene: Avoid piping stress on pump heads and ensure proper torque specifications are used during assembly.
- Safety First: For hazardous fluids, specify double diaphragms with leak detection and spray shields.
- Architecture Precedes Everything: The sealing arrangement follows from the drive technology and the chemical service, so pump type and material selection are the decisions that determine which failure modes are even possible.
Addressing Metering Pumps Seal Failures: Causes requires a holistic engineering approach. It is not enough to simply select a pump from a catalog based on flow and pressure. The engineer must consider the fluid dynamics of the suction piping, the chemical interaction with elastomers under varying thermal conditions, and the physical constraints of the installation.
By shifting focus from component replacement to system design—specifically optimizing suction conditions and selecting materials based on rigorous compatibility analysis—utilities and industrial plants can transform their chemical feed systems from maintenance headaches into reliable process assets. When specifying new equipment, prioritize constructability, maintenance access, and robust hydraulic protection (dampeners and relief valves) to ensure the seals have a fighting chance to perform for their expected lifecycle. The subcategory guides linked above cover pump architecture, chemical service selection, and specification practice in the depth that each of those decisions deserves.