
Top OEMs for Check Valves
Introduction
In municipal and industrial water and wastewater systems, the check valve serves a critical, albeit often understated, function: the prevention of reverse flow. While the fundamental concept—allowing flow in one direction while blocking it in the other—appears simple, the engineering reality is complex. Check valves are the primary defense against pump reversal, which can lead to mechanical seal failure, bearing damage, and motor burnout. More importantly, they play a pivotal role in the hydraulic transient response of a pipeline, influencing the severity of surge pressures (water hammer) following abrupt pump trips.
For consulting engineers, plant managers, and utility superintendents, the selection of a check valve is rarely a “one-size-fits-all” decision. The operational environments range from high-pressure potable water distribution networks requiring minimal head loss to aggressive wastewater lift stations laden with solids, grit, and ragging materials. Regulatory contexts, including compliance with AWWA standards (such as C508 and C518) and NSF/ANSI 61/372 certifications for potable water, set the baseline for acceptance. However, the long-term reliability and maintainability of the valve depend heavily on the specific design philosophies and manufacturing quality of the Original Equipment Manufacturer (OEM).
The distinction between a commodity valve and an engineered solution becomes evident in the lifecycle analysis. A poorly selected or manufactured check valve can lead to excessive energy consumption due to high head loss, catastrophic pipe bursts due to slamming, or frequent maintenance intervals due to clogging or seat degradation. Therefore, understanding the engineering pedigree, manufacturing capabilities, and specific product portfolios of top OEMs is essential for specifying equipment that ensures system integrity and operational efficiency. Higher-specification variants such as dual plate check valves illustrate the point directly: two spring-loaded half-discs close far faster than a single swinging disc, and the difference between manufacturers in spring rate, hinge pin material, and disc geometry determines whether that speed advantage survives twenty years of service.
How to Select This Valve Type
Selecting the appropriate check valve requires a rigorous engineering approach that moves beyond pipe diameter matching. The valve must be treated as a dynamic component of the hydraulic system. Engineers must evaluate the valve’s response to changes in flow velocity and its interaction with the pump and piping geometry. The following criteria are essential for a comprehensive specification strategy.
Valve Function and Duty Cycle
The primary function is non-return, but the duty cycle dictates the design. Is the pump cycling every 10 minutes or running continuously for weeks? High-cycle applications, such as fill-and-draw systems or lift stations with small wet wells, place immense stress on moving parts like hinge pins, springs, and discs. In these scenarios, fatigue failure is a genuine risk. Engineers must specify valves designed for high-cycle endurance, often favoring designs with minimal moving parts or resilient hinge mechanisms that eliminate mechanical wear points.
Dynamic Characteristics and Surge Control
Perhaps the most critical engineering consideration is the valve’s “non-slam” characteristic. Slamming occurs when the reverse velocity of the fluid builds up before the valve disc is fully seated. When the disc finally impacts the seat, the sudden halt of the reversing water column generates a pressure spike (surge). To prevent this, the valve must close before significant reverse velocity develops. This requires analyzing the deceleration of the fluid column versus the closing speed of the valve. Tilted disc and spring-assisted silent check valves are often specified where rapid flow reversal is anticipated to mitigate water hammer.
Pressure and Flow Conditions
Static pressure rating is straightforward, but dynamic flow conditions are nuanced. Engineers must ensure the valve is sized to be fully open at normal operating flow rates. If a check valve is oversized, the disc may not lift fully against the internal stop, leading to “chatter” or oscillation. This constant movement causes premature wear on the hinge and seat. Conversely, an undersized valve creates excessive head loss. The Coefficient of Flow ($C_v$) and the resistance coefficient ($K$) must be evaluated to calculate the permanent pressure drop and the resulting energy cost over the valve’s lifecycle.
Materials of Construction
Material selection is dictated by the media and the environment:
- Body: ASTM A536 Ductile Iron is the industry standard for strength and shock resistance in modern municipal applications, preferred over Cast Iron (ASTM A126) for its ductility.
- Seats: Bronze or stainless steel seats offer durability, but resilient seats (EPDM, Buna-N, or Neoprene) are preferred for “drop-tight” sealing, especially in low-pressure applications or where grit is present.
- Internal Hardware: Hinge pins and springs should be 304 or 316 Stainless Steel to prevent corrosion that could seize the mechanism.
- Coatings: Fusion Bonded Epoxy (FBE) lining and coating are mandatory for corrosion protection in both water and wastewater, preventing tuberculation and ensuring smooth flow paths.
Sealing Mechanisms
The seal design impacts both leakage rates and longevity. Metal-to-metal seats are robust but may allow minor leakage over time, which can be problematic for retaining pump prime. Resilient seats provide zero-leakage performance but are susceptible to abrasion and chemical attack. In wastewater, the seat design must also resist trapping solids. Angled seats or ball checks are often employed to ensure that gravity assists the seating process and that debris is flushed away during the closing cycle.
Wastewater Specifics: Clogging and Ragging
In wastewater applications, the “clearway” or “free passage” specification is paramount. Standard swing check valves often have internal protrusions (hinge arms, stops) that catch “rags” (fibrous wipes and debris). Over time, this buildup prevents the valve from closing or opening fully. Ball check valves, cushioned swing checks with external levers, or tilted disc valves with contoured bodies are engineered to pass solids equivalent to the pipe size. Understanding the nature of the influent—specifically the solids burden—is critical for preventing maintenance nightmares.
Installation Environment and Orientation
Not all check valves function in vertical piping. While most operate horizontally, vertical flows (typically upward) require specific designs to ensure the disc closes via gravity or spring force when flow stops. Furthermore, installation proximity to the pump discharge and downstream fittings (elbows, tees) affects turbulence. Turbulent flow causes disc instability and accelerated wear. Engineers should adhere to the “5D to 10D” rule (5 to 10 pipe diameters of straight pipe) whenever possible, or select valves specifically designed to handle turbulent inlet conditions.
Maintenance and Serviceability
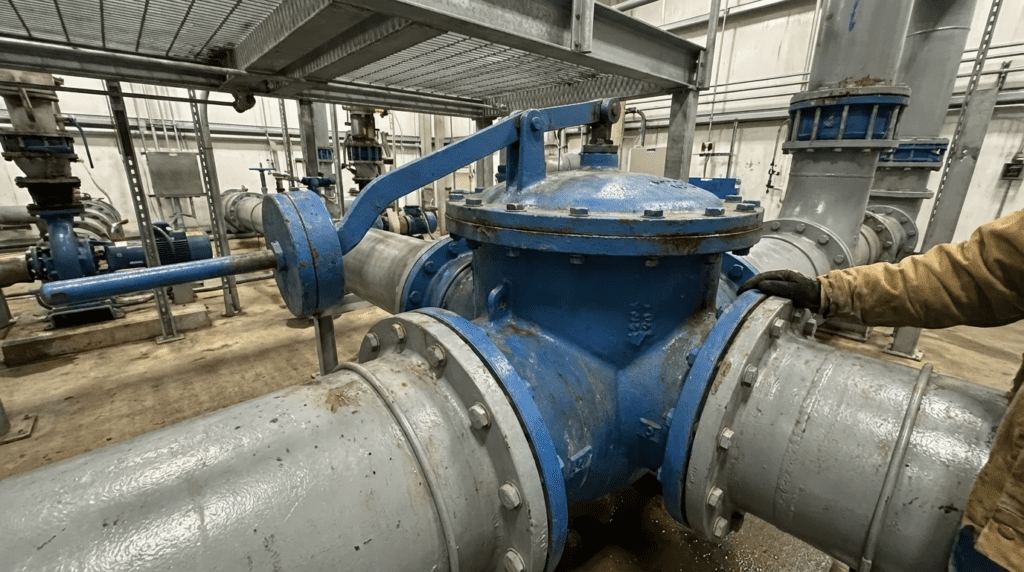
For Plant Managers, the question is: “How do I fix it when it fails?” Valves with top-access covers (bonnets) allow operators to inspect and replace internal components without removing the heavy valve body from the line. In contrast, wafer-style valves typically require removal from the flange to service. External levers and weights allow operators to visually confirm valve position and manually initiate movement if a disc is stuck, a feature highly valued in wastewater lift stations.
Lifecycle Cost Considerations
The purchase price of a check valve is a fraction of its total cost of ownership. The primary cost driver is energy consumption due to head loss. A valve with a low head loss design can save thousands of dollars annually in pumping costs compared to a high-loss alternative. Additionally, the cost of unplanned downtime and labor for unclogging valves in wastewater systems must be factored into the selection process.
Check Valve Types and Manufacturer Alignment
Manufacturer strength is not uniform across check valve architectures. Several of the OEMs profiled below dominate one valve type while being marginal in another, which means the type decision constrains the supplier shortlist before any commercial comparison begins. The three architectures below account for the large majority of municipal installations.
Swing Check Architecture
The swing check remains the default for general distribution service, and it is the architecture against which the others are measured. The behaviour of swing check valves is governed by disc travel and gravity: the disc rotates through roughly ninety degrees, and closure depends on the disc falling back to the seat as forward flow decays.
That long stroke is both the strength and the weakness. It produces a large unobstructed waterway and low head loss when fully open, and it makes the design simple, serviceable, and cheap to stock. But closure is slow relative to flow reversal in systems with high deceleration, which is precisely the slamming mechanism described above. Outside lever and weight or lever and spring accessories partially compensate by accelerating closure, and they add the operational benefit of visible position indication. For steady-flow distribution mains at moderate pressure, the standard swing check is the correct and economical answer.
Non-Slam and Silent Check Architecture
Where flow reversal is rapid, the design objective inverts: the valve must close before reverse velocity develops rather than in response to it. The family of non-slam check valves — spring-assisted silent checks, dual disc designs, and tilted disc geometries — achieves this through short disc travel combined with spring loading.
The trade-off is head loss and complexity. A spring that closes the valve quickly also resists opening, which imposes a permanent cracking pressure and a continuous energy cost. Springs are a wear item and a corrosion risk, which is why 304 or 316 stainless is specified rather than treated as an option. The engineering question is not whether non-slam performance is desirable — it always is — but whether the system’s deceleration rate actually requires it. Specifying a spring-loaded silent check into a low-deceleration gravity system buys a permanent pumping penalty to solve a problem the system does not have.
Lift Check and Guided Poppet Architecture
The third architecture constrains the closure element to axial movement rather than rotation. In lift check valves the disc or poppet travels along a guide perpendicular to the seat, which gives precise, repeatable seating and excellent resistance to chatter under fluctuating flow.
That guidance is the reason this architecture dominates in VFD-driven and vertical well service, where flow modulates continuously and a swinging disc would flutter against its stop. The constraints are head loss — the flow path turns, and the guide structure obstructs it — and solids tolerance, since the close clearances that provide guidance are also where grit and fibrous material lodge. Lift checks belong in clean water and are a poor choice for raw wastewater regardless of manufacturer.
Comparison Table
The following table provides a comparative overview of the specified OEMs. It is intended to assist engineers and operators in matching manufacturer strengths with specific project requirements. This is not a numerical ranking of quality, but rather a guide to the “engineering DNA” and primary focus areas of each manufacturer. Users should interpret “Limitations” as boundary conditions for application, urging careful review of specifications for those particular scenarios.
| OEM Name | Core Check Valve Technologies | Typical Applications | Engineering Strengths | Considerations & Limitations |
|---|---|---|---|---|
| Val-Matic Valve & Mfg. | Tilted Disc, Swing-Flex®, Surgebuster®, Silent Check, Dual Disc | Municipal Water, Wastewater Lift Stations, High-Service Pumping, Surge Control | Industry-leading surge control designs; Swing-Flex resilient hinge minimizes maintenance (no moving parts to wear); Low head loss characteristics. | Premium engineered designs may carry higher initial CAPEX compared to commodity swing checks; specialized sizing required for Surgebuster. |
| Henry Pratt | Rubber Flapper, Ball Check, Tilted Disc, Swing Check | Wastewater, Raw Water Intakes, Large Diameter Transmission | Extremely robust, heavy-duty construction; Rubber flapper design is excellent for raw sewage and sludge; strong history in very large diameter valves. | Product portfolio leans heavily towards large industrial/municipal scale; may be “over-spec” for small commercial-grade utility tie-ins. |
| Mueller | Swing Check (Gravity & Spring), Iron Body Bronze Mounted (IBBM) | Potable Water Distribution, Fire Protection, General Utility | Massive installed base and parts availability; standardized designs meet virtually all municipal specifications (AWWA); high reliability in standard water applications. | Traditional swing check designs are susceptible to slamming in high-dynamic applications without external damping accessories. |
| Proco Products | Duckbill (Rubber) Check Valves, In-line Series 700 | Stormwater Outfalls, Diffusers, Sludge, Corrosive Media | Passive design with zero mechanical parts; immune to corrosion and seizing; “Barnacle-proof”; ideal for low head loss, solids-laden, or environmentally exposed applications. | Not suitable for high-pressure transmission lines compared to iron valves; backpressure limitations exist based on elastomer stiffness. |
| Flomatic Corporation | Submersible Pump Checks, VFD Special Valves, Ball Checks, Wafer | Groundwater Wells, Booster Stations, VFD Systems, Wastewater | Specializes in preventing water hammer in vertical well applications; patented VFD-compatible valve designs; stainless steel internal components standard on many lines. | Historically focused on small to mid-range sizes (though range is expanding); specific focus on well/booster markets distinct from large transmission mains. |
Top OEM Manufacturers
Val-Matic Valve & Manufacturing
Val-Matic is widely regarded by engineering consultants as a premier manufacturer for high-performance check valves, particularly where hydraulic transients (surge) and energy efficiency are primary concerns. Their engineering philosophy centers on the dynamic behavior of the valve disc.
Technical Profile: Val-Matic’s flagship Tilted Disc Check Valve is a staple in high-service pump stations. The pivot point of the disc is located eccentrically, allowing the bottom of the disc to swing open with the flow while the top rotates backward. This geometry provides a short stroke (typically 40 degrees versus 90 degrees for a swing check), resulting in rapid closure that significantly reduces the potential for water hammer. The valve offers very low head loss, translating to operational energy savings.
Wastewater Innovations: For wastewater, Val-Matic developed the Swing-Flex® and Surgebuster® check valves. These designs utilize a resilient disc with an integral hinge, eliminating the traditional hinge pin and potential leak paths. The absence of internal moving parts prevents ragging and mechanical wear. The Surgebuster includes a “Disc Accelerator,” a mechanical device that speeds up closure to prevent slamming in systems with high reverse flow deceleration.
Engineering Assessment: Val-Matic is a “go-to” specification for critical pump stations where reliability and surge mitigation are non-negotiable. Their provision of detailed surge analysis data and head loss curves simplifies the design engineer’s task.
Henry Pratt
Henry Pratt, part of the Mueller Water Products family but operating with a distinct engineering lineage, is synonymous with heavy-duty valves for large-scale infrastructure. While famous for butterfly valves, their check valve portfolio is engineered for severe service environments.
Technical Profile: Pratt’s Rubber Flapper Check Valve is a standout for raw sewage and solids-bearing water. The design features a disc with a 45-degree seat angle, which reduces the travel distance required to close, thereby minimizing slam potential. The “flapper” is a steel disc fully encapsulated in rubber, providing a drop-tight seal and high resistance to abrasion. The hinge mechanism is designed to be virtually maintenance-free, with the continuous rubber flex replacing mechanical rotation.
Ball Check Valves: Pratt also manufactures robust ball check valves. These utilize a sinking ball that moves fully out of the flow path into a recessed cover area, providing a full-port flow with low head loss. As flow stops, the ball rolls back to the seat. This rolling action constantly presents a different seating surface, ensuring uniform wear and self-cleaning operation.
Engineering Assessment: Pratt is an optimal choice for large-diameter raw water intakes and wastewater treatment plant headers. Their valves are built with substantial safety factors in wall thickness and material strength, prioritizing longevity in abrasive and abusive environments.
Mueller
Mueller is arguably the most ubiquitous brand in North American water infrastructure. Their check valves represent the standard for reliability in potable water distribution and fire protection systems. Their focus is on compliance, standardization, and breadth of availability.
Technical Profile: Mueller’s primary offering in this category is the AWWA C508 Swing Check Valve. Constructed of ductile iron with bronze trim (IBBM), these valves are designed for durability and ease of maintenance. They feature full-flow waterways and are available with a variety of arm and lever configurations. Options include outside lever and weight (to assist closing) or outside lever and spring (to accelerate closing). This external hardware also allows operators to visually inspect the valve position.
Serviceability: A key strength of the Mueller design is the bolted bonnet. This allows complete access to the interior for maintenance (disc replacement, seat inspection) without removing the valve body from the pipeline—a critical feature for buried service vaults or tight mechanical rooms.
Engineering Assessment: Mueller is the baseline specification for municipal distribution networks. While they may not offer the exotic surge-damping geometries of specialized OEMs, their valves are proven, cost-effective, and supported by an extensive network of spare parts. They are best suited for standard duty cycles in potable water systems.
Proco Products
Proco Products occupies a unique niche in the check valve market, specializing in elastomeric (rubber) check valves, commonly known as “duckbill” valves. Their engineering approach is radically different from the iron-and-steel manufacturers, focusing on passive, corrosion-immune solutions.
Technical Profile: The Proco Series 700 is an elastomeric check valve that looks like a duck’s bill. It relies on the line pressure to open and the elasticity of the rubber (and backpressure) to close. There are no mechanical hinges, seats, seals, or springs to corrode, seize, or wear out. This makes them ideal for stormwater outfalls, diffuser systems, and corrosive chemical lines.
Application Specifics: In wastewater treatment, Proco valves are often used in sludge lines or as backflow preventers in contact tanks. Their “barnacle-proof” nature makes them the only viable option for submerged marine outfalls where marine growth would seize a mechanical valve. They offer low head loss and can handle significant slurries and solids without jamming.
Engineering Assessment: Proco is the definitive choice for “end-of-line” protection and aggressive media. Engineers specify Proco when mechanical failure is not an option due to accessibility issues (e.g., underwater) or chemical incompatibility. They are not typically used for high-pressure pump discharge but are unbeatable in their specific domain.
Flomatic Corporation
Flomatic Corporation distinguishes itself through a focus on valve geometry and high-quality materials, often targeting the intersection of efficiency and VFD (Variable Frequency Drive) operations. They have a strong pedigree in the groundwater and booster station sectors.
Technical Profile: Flomatic is well-known for the Enviro-Check® and their submersible pump check valves. They utilize a guided poppet system that is engineered to be VFD compatible. Rapid flow changes from VFD ramping can wreak havoc on standard valves; Flomatic’s designs are sprung and guided to handle these modulations without chattering. Their valves frequently feature stainless steel bodies or internal components as standard, offering superior corrosion resistance compared to standard iron valves.
Versatility: They also manufacture the Model 408 Ball Check Valve for wastewater, which features a floating, self-cleaning ball. Their “AIS” (American Iron and Steel) compliant product lines meet federal funding requirements for municipal projects.
Engineering Assessment: Flomatic is an excellent specification for vertical turbine pumps, wells, and booster stations where space is at a premium and water hammer protection is critical. Their focus on unleaded bronze and stainless steel makes them highly suitable for strict potable water compliance environments.
Head-to-Head Manufacturer Comparisons
The profiles above establish where each supplier concentrates its engineering effort, but bid evaluation almost always narrows to a direct choice between two candidates that both meet the specification. The comparisons below address the pairings that recur most often on municipal check valve procurements.
Heavy-Duty Construction Versus Surge-Optimised Hydraulics
The most common pairing in wastewater and large-diameter work sets robust construction against dynamic performance, and both approaches have legitimate claims. The comparison of Henry Pratt vs Val-Matic for check valves works through this trade-off, covering rubber flapper and ball check designs against tilted disc and resilient-hinge alternatives.
The screening logic follows from the material above. Where the governing risk is abrasion, solids burden, and sheer service life in an abusive environment — raw sewage headers, large intakes, grit-laden influent — heavy wall sections and encapsulated flapper designs earn their weight. Where the governing risk is a hydraulic transient that could rupture a force main, closure speed and documented surge performance matter more than wall thickness. The decisive question is which failure the system is actually exposed to, and a transient analysis answers it more reliably than intuition.
Industrial Heritage Versus Municipal Specialisation
The second pairing sets a manufacturer with broad industrial and general valve heritage against one specialised in municipal water and wastewater service. The evaluation of Crane vs Henry Pratt check valves examines this distinction, which surfaces most often on industrial effluent and cross-sector projects.
Industrial-heritage suppliers typically bring wider pressure class and material range, stronger coverage of ASME and API dimensional standards, and better options for elevated temperature or aggressive chemistry. Municipal specialists bring AWWA C508 and C518 compliance as a default rather than an option, designs shaped around ragging and solids, and dimensional consistency with an installed base going back decades. On a potable water or municipal wastewater project the municipal specialist is usually the shorter path; on industrial effluent with unusual chemistry or pressure class, the industrial supplier frequently has the only compliant product.
Actuation Specialists Versus Control Valve Manufacturers
The third pairing crosses into automated and controlled check service, where the valve is not a purely passive device. The comparison of Rotork vs Singer Valve check valves addresses this layer, setting an actuation and controls specialist against a manufacturer of hydraulically controlled valves.
The relevant application is pump control, where a single device must prevent reverse flow and also open and close on a controlled ramp to manage the transient at pump start and stop. That is a controlled valve with a check function, not a check valve with an accessory, and it is specified differently: opening and closing speeds become independent adjustable parameters, the control signal source must be defined, and failure behaviour on loss of power or signal becomes an explicit decision rather than a default. Where a passive check genuinely suffices, this added complexity is a liability; where the transient must be shaped rather than merely survived, it is the only workable approach.
Application Fit Guidance
Successful valve application requires matching the OEM’s specific design philosophy to the system’s hydraulic reality. The following breakdown aligns manufacturers with their strongest application environments.
Municipal Water Distribution
Preferred: Mueller, Val-Matic.
For general distribution mains where flow is relatively steady and pressures are moderate, Mueller’s AWWA swing checks offer the best balance of cost and maintainability. In high-service pump stations feeding these mains, where pump trips could cause significant surges, Val-Matic’s Tilted Disc or Surgebuster valves are preferred to protect the infrastructure from water hammer.
Municipal Wastewater (Lift Stations & Treatment)
Preferred: Val-Matic, Henry Pratt, Flomatic.
Standard swing checks are prone to clogging here. Val-Matic’s Swing-Flex and Pratt’s Rubber Flapper are industry standards because they lack the internal snag points that catch rags. For smaller lift stations (4” and under), Flomatic’s Ball Checks are highly effective. For large raw sewage influent lines, Pratt’s heavy-duty construction provides the necessary longevity.
Stormwater and Outfalls
Preferred: Proco Products.
For pipes discharging into rivers, oceans, or retention ponds, mechanical valves are a liability due to corrosion and debris. Proco’s duckbill valves are the dominant solution, requiring zero maintenance and providing reliable backflow prevention even when buried in silt or surrounded by marine growth.
High-Pressure and Vertical Applications
Preferred: Val-Matic, Flomatic.
Vertical lines require spring-assisted closure or specific geometric designs to function correctly. Flomatic’s silent check valves and Val-Matic’s axial flow or tilted disc options are engineered to handle the high head pressures and rapid flow reversals found in high-rise boosting or deep well applications.
Engineer & Operator Considerations
Beyond the catalog specifications, real-world operation reveals challenges that must be addressed during the design phase.
Installation Best Practices
The “5D Rule” cannot be overstressed. Installing a check valve immediately downstream of an elbow or immediately upstream of a modulating control valve creates turbulence. This turbulence causes the disc or ball to flutter, leading to “keyholing” of hinge pins or uneven seat wear. If space constraints make 5 pipe diameters of straight run impossible, engineers must specify valves designed for turbulent service or consult the OEM for derating factors.
Common Specification Mistakes
- Oversizing: Engineers often match the valve size to the line size without checking the minimum velocity required to fully open the valve. If a 12-inch valve is installed in a line with low flow, the disc will float in a partially open position, oscillating and wearing out prematurely. It is often better to install a smaller valve (with reducers) to ensure the disc remains fully open and stable during operation.
- Ignoring “Slam” Potential: Specifying a standard swing check in a system with high dynamic head and a long vertical column is a recipe for disaster. When the pump trips, the column reverses instantly. A standard swing check closes too slowly, resulting in a violent slam. In these cases, a Silent Check or Tilted Disc is mandatory.
Maintenance Access
Operators frequently cite poor access as their primary frustration. If a valve is installed in a vault, is there clearance to remove the bonnet bolts? Can the hinge pin be extracted horizontally without hitting the vault wall? For wastewater applications, specifying valves with “backflow actuators” or external levers allows operators to manually lift the disc to flush out debris—a critical feature for unclogging pumps without disassembly.
Spare Parts and Obsolescence
Water infrastructure is designed for 50-year lifecycles. OEMs like Mueller and Pratt have product lines that have remained dimensionally consistent for decades. This backward compatibility ensures that a bonnet gasket or hinge pin ordered today will fit a valve cast in 1980. Importing “white label” valves may save money upfront, but often leads to total valve replacement when a simple seal fails 10 years later due to lack of parts.
Frequently Asked Questions
How do I know whether my system needs a non-slam check valve?
The determining factor is the deceleration rate of the water column after a pump trip, which depends on pipeline length, static head, and fluid inertia. Short lines with low static head decelerate slowly and tolerate a standard swing check. Long force mains with high static head reverse quickly and will slam a conventional valve. A transient analysis provides the answer quantitatively; as a rough screen, any system with a long force main and significant elevation gain should be assumed to require non-slam performance until analysis shows otherwise.
Why does oversizing a check valve cause damage?
A check valve disc needs a minimum flow velocity to lift fully against its internal stop and stay there. Below that velocity, the disc floats in a partially open position and oscillates with every minor flow fluctuation, wearing the hinge pin and seat continuously. Because the valve is the same size as the line, engineers assume it is correctly sized, and the resulting wear is often misattributed to poor manufacturing quality. Installing a smaller valve with reducers is frequently the better engineering answer.
What is the most common check valve failure in wastewater service?
Ragging. Fibrous material catches on hinge arms, stops, and any internal protrusion, accumulating until the disc can no longer close fully or open cleanly. The valve then leaks backward, allows the pump to spin in reverse, or blocks flow entirely. This is a design-stage problem rather than a maintenance one: architectures with unobstructed waterways and no internal snag points prevent it, while conventional swing checks in wastewater service will accumulate rags no matter how often they are cleaned.
Do check valves need maintenance if they have no external actuator?
Yes. Hinge pins wear, seats degrade, springs fatigue and corrode, and resilient discs harden with age. A check valve that has never been opened for inspection in fifteen years is not proof of reliability; it is an unknown. Annual inspection through the bonnet, where the design permits it, catches seat and hinge wear before it becomes leakage or a stuck disc. Valves without top access should be scheduled for removal and bench inspection on a defined interval.
How much does head loss across a check valve actually cost?
Enough to change the selection on continuously operating pump discharge. Head loss translates directly into pumping energy, and the difference between a low-loss and a high-loss architecture on a continuously running pump commonly exceeds the capital price difference within a few years. The analysis requires the valve’s resistance coefficient at the actual operating velocity, not its catalogue pressure drop at a nominal flow, and it should be performed rather than assumed in either direction.
Key Takeaways
- Match the architecture before the manufacturer — swing, non-slam, and lift check designs draw from different supplier strengths, and choosing a brand first quietly dictates the architecture.
- Slam risk is a system property, not a valve property — deceleration rate after pump trip determines whether non-slam performance is required; a transient analysis answers it, intuition does not.
- Do not size the valve to the pipe by default — a disc that never lifts fully oscillates and destroys its own hinge and seat, and a smaller valve with reducers is often correct.
- Ragging is designed out, not maintained out — unobstructed waterways and the absence of internal snag points are the only reliable defence in wastewater service.
- Head loss is a recurring cost — on continuously operating pump discharge it frequently outweighs the capital difference between competing designs within a few years.
- Specify stainless for every internal wear part — hinge pins and springs that seize turn a passive device into a blockage.
- Verify serviceability in the actual vault — bonnet clearance and hinge pin extraction path are design-stage checks that cannot be corrected afterward.
Conclusion
The selection of a check valve is a critical engineering decision that directly impacts the hydraulic stability, energy efficiency, and maintenance burden of water and wastewater systems. It is not a commodity purchase. The “Top” OEM for a specific project depends entirely on the application context: Val-Matic excels in surge control and high-performance hydraulics; Pratt offers unmatched robustness for large-scale, solids-laden applications; Mueller provides the standard for potable water maintainability and parts availability; Proco solves the unique challenges of passive, corrosive, and outfall environments; and Flomatic delivers precision for wells and VFD-driven systems.
For the consulting engineer and the plant manager, the goal is to align the valve’s mechanical characteristics with the system’s hydraulic behavior. By looking past the initial purchase price and evaluating the total lifecycle cost—including energy loss and maintenance hours—utilities can secure infrastructure reliability that endures for decades.