Aeration Blower Types: An In-depth Exploration
Aeration blowers are essential in various industries, particularly in wastewater treatment facilities, aquaculture, and chemical processing sectors. The primary function of these blowers is to supply air to systems requiring oxygenation or agitation. This prevents anaerobic conditions, promotes bacterial growth for decomposition, and ensures optimal process conditions. This article delves into different types of aeration blowers, examining their operations, applications, advantages, and disadvantages.
Type selection is one of the two decisions that determine what an aeration system costs to run for the next two decades, the other being how it is sized. Within the broader subject of aeration blowers, the choice among machine families is less about which is best in the abstract and more about which one matches the pressure, the load profile, and the environment a specific plant actually presents.
Introduction to Aeration Blowers
Importance of Aeration
Aeration is a critical process in many industries, aimed at introducing air into a liquid, promoting oxygen transfer. In wastewater treatment, aeration is essential for the biological degradation of organic pollutants. In aquaculture, it maintains oxygen levels to support healthy aquatic life.
Basics of Aeration Blowers
Aeration blowers are mechanical devices designed to inject air into liquids. They come in different shapes and sizes but share the common goal of ensuring sufficient oxygen transfer rates and efficient mixing.
How Blowers Compress Air: The Fundamental Divide
Every blower on the market belongs to one of two families, and understanding the difference explains most of the behaviour that follows — including several characteristics that are frequently misattributed to individual manufacturers.
Positive Displacement
A positive displacement machine traps a fixed volume of air in a chamber and pushes it into the discharge. Because the volume per revolution is fixed by geometry, flow is essentially independent of discharge pressure — the machine delivers what it delivers, and the system determines the pressure required to accept it. Raising the pressure raises the power draw but not the flow. This gives positive displacement blowers a flat, predictable characteristic that tolerates changes in system resistance without any risk of instability, which is the main reason they remain the default in smaller plants and in systems where diffuser fouling steadily raises back pressure over time.
Dynamic Compression
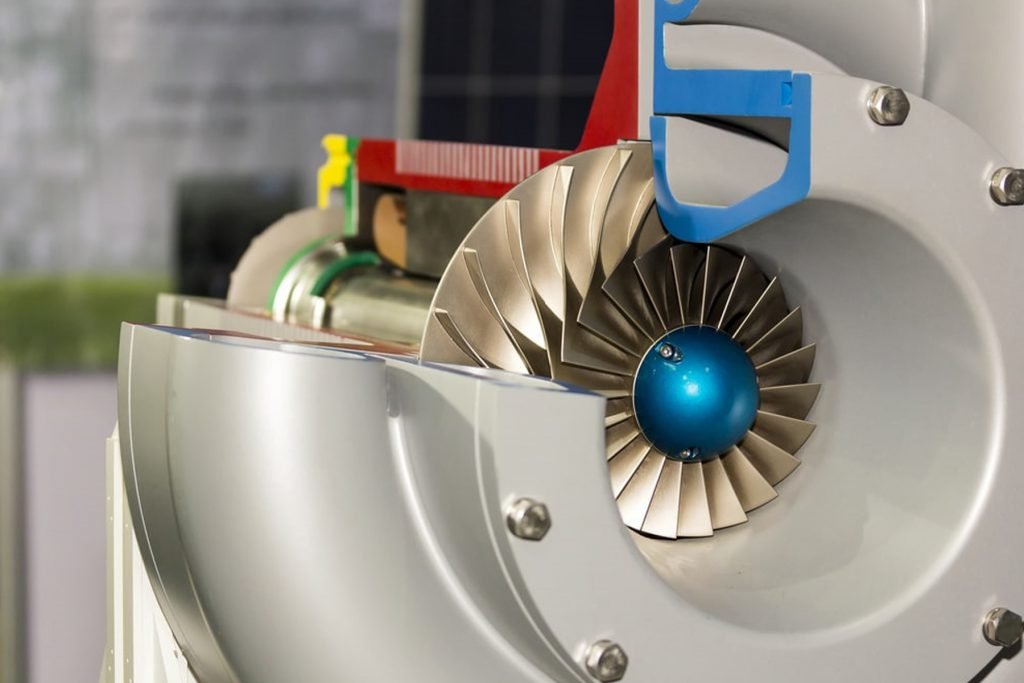
A dynamic machine — any centrifugal or turbo type — accelerates air with an impeller and converts that velocity into pressure. Flow and pressure are coupled: the machine follows a performance curve, and the operating point is wherever that curve intersects the system resistance curve. Raise the back pressure and the flow falls. This coupling makes dynamic machines more efficient at their design point but far more sensitive to system changes, and it introduces a failure mode that positive displacement machines simply do not have.
Why Surge Matters
As flow through a dynamic machine is reduced at constant pressure, it eventually reaches a point where the impeller can no longer sustain the discharge pressure. Flow reverses momentarily, pressure collapses, flow re-establishes, and the cycle repeats — often several times per second. This is surge, and it produces violent vibration, rapid bearing and seal damage, and in severe cases catastrophic failure. Every centrifugal and turbo blower has a surge line on its performance map, and the useful operating range lies to the right of it with a margin of typically 10 to 15 percent. Turndown on a dynamic machine is therefore limited by surge rather than by the drive, which is the single most important practical distinction between the two families.
Types of Aeration Blowers
Centrifugal Blowers
Centrifugal blowers, also known as radial blowers, utilize centrifugal force to move air. They consist of a rotating impeller inside a casing. As the impeller spins, it accelerates the air outward to the edge of the casing, converting velocity into pressure.
In wastewater service the two dominant configurations are multistage and single-stage geared. Multistage machines put several impellers in series on a common shaft, typically delivering 5 to 15 psig, and turn down by inlet throttling or inlet guide vanes across roughly 60 to 100 percent of rated flow before surge intervenes. Single-stage geared machines use one high-speed impeller with both inlet guide vanes and a variable diffuser, which widens usable turndown to roughly 45 to 100 percent and pushes wire-to-air efficiency into the 70 to 80 percent range at and near the design point.
Applications
- Wastewater Treatment: Used in large-scale aeration tanks.
- HVAC Systems: For air handling and ventilation.
- Industrial Processes: Common in pneumatic conveying and cooking operations.
Advantages
- High Efficiency: Capable of producing high airflow rates at lower energy consumption.
- Stable Performance: Offers consistent pressure output.
- Durability: Relatively long lifespan and low maintenance.
Disadvantages
- Complex Installation: Requires precise alignment and balancing.
- Noise Levels: Can be noisier compared to some other types.
- Surge Limitation: Turndown is bounded by the surge line, not by the drive.
Positive Displacement Blowers
Positive displacement blowers trap a specific volume of air and then force it into the aeration system. They come in various designs, including rotary lobe, screw, and piston blowers.
Rotary Lobe Blowers
Rotary lobe blowers utilize two intermeshing rotors to displace air. The rotors spin in opposite directions, trapping air in the pockets formed between the rotors and the casing.
Rotary lobe machines have no internal compression — air is pushed out against system pressure rather than being compressed within the machine. That is what makes them simple and robust, and also what limits their efficiency, which typically falls in the 45 to 60 percent wire-to-air range and declines as discharge pressure rises. Practical single-stage pressure is around 15 psig, and bare-machine noise commonly exceeds 95 dBA, which is why an acoustic enclosure is effectively standard rather than optional.
Applications
- Wastewater Treatment: Often used in aeration tanks and digesters.
- Industrial Vacuum: Applied in conveying systems.
- Pneumatic Transport: Useful in material handling operations.
Advantages
- Simplicity: Simple design and robust construction.
- Variable Flow Rates: Capable of adjusting flow rates.
- Low Maintenance: Minimal moving parts contribute to lower maintenance.
- No Surge Risk: Flow is independent of discharge pressure.
Disadvantages
- Noise: Known for being noisy, especially at higher pressures.
- Efficiency: Less efficient than centrifugal blowers at higher pressures.
- Pulsation: Discharge pulsation requires silencers and can stress piping.
Screw Blowers
Screw blowers utilize twin helical screws to compress and transport air. These screws rotate and mesh in a synchronized manner, creating a continuous flow of air.
The distinguishing feature is internal compression: unlike a lobe machine, the screw profile progressively reduces the trapped volume before discharge, so the air arrives at close to system pressure rather than being pushed against it. That single design difference typically yields 10 to 30 percent lower energy consumption than a lobe machine at the same duty, with wire-to-air efficiency in the 60 to 70 percent range and practical pressures to roughly 22 psig. It also produces far less pulsation, which is why screw machines run noticeably quieter.
Applications
- Wastewater Treatment: Suitable for aeration systems requiring continuous airflow.
- Process Industries: Used in food processing and chemical plants for fermentation processes.
Advantages
- Efficiency: High efficiency over a broad range of operating conditions.
- Noise Reduction: Quieter than rotary lobe blowers due to less pulsation.
- Thermal Management: Reduced heat generation compared to other positive displacement blowers.
Disadvantages
- Cost: Generally more expensive to purchase and maintain.
- Complexity: More complex design resulting in intricate maintenance procedures.
High-Speed Turbo Blowers
High-speed turbo blowers are a distinct dynamic machine family that has taken substantial market share in municipal aeration over the past two decades. A single high-speed impeller is driven directly by a permanent magnet motor through a variable frequency drive, supported on either magnetic or air-foil bearings, with no gearbox and no lubrication system.
The result is the highest wire-to-air efficiency generally available — commonly 70 to 80 percent — combined with wide speed-based turndown of roughly 40 to 100 percent, oil-free operation, low noise in the 75 to 85 dBA range, and a compact packaged footprint. The trade-offs are real: capital cost is higher, performance is sensitive to inlet air temperature and site elevation in ways that must be verified rather than assumed, and the machine places sophisticated power electronics in a humid and often corrosive environment. Surge remains a constraint, though the wide speed range and integrated controls manage it more gracefully than throttled machines do.
Applications
- Municipal Wastewater Treatment: Increasingly the default where energy cost dominates.
- Plant Upgrades: Compact packaging suits retrofit into existing blower buildings.
Piston Blowers
Piston blowers use a reciprocating piston mechanism to displace air. The air is drawn into a cylinder and compressed as the piston moves through its cycle.
Applications
- Medical Applications: Often used in respiratory devices and ventilators.
- Precision Aeration: Applied in systems where precise air control is critical.
Advantages
- Precision: Capable of providing highly accurate air delivery.
- Pressure Capabilities: Can achieve very high pressures.
Disadvantages
- Complexity: Requires frequent maintenance due to more moving parts.
- Noise and Vibration: Tends to be noisier and more prone to vibration issues.
Liquid Ring Blowers
Liquid ring blowers, also known as liquid ring compressors, employ a rotating assembly that includes a pump casing partially filled with liquid. Air is drawn into the casing, and the liquid forms a moving ring that compresses the air.
Applications
- Vacuum Processing: Common in applications requiring low-pressure vacuum.
- Dewatering Systems: Utilized in industries that need continuous dewatering.
- Steam Recovery: Used in systems recovering vapor and steam.
Advantages
- Reliability: Robust and reliable performance.
- Low Noise Levels: Operates more quietly than other blower types.
- Handles Contaminants: Can handle air mixed with liquids or small amounts of particulates.
Disadvantages
- Efficiency: Generally less efficient compared to centrifugal blowers.
- Complexity: Requires careful maintenance to manage the liquid medium and avoid leaks.
Regenerative Blowers
Regenerative blowers, also known as side channel blowers, use an impeller with numerous blades that pass through a channel. Air is drawn into the impeller and circulated several times within the blower housing to increase pressure before being discharged.
Their working range is limited — typically to around 2 to 3 psig — which confines them to shallow basins, small package plants, and aquaculture rather than municipal aeration at depth. Within that range they are inexpensive, compact, and effectively maintenance-free.
Applications
- Aquaculture: Maintains oxygen levels in fish farms.
- Vacuum Lifting: Used in material lifting and conveying systems.
- OEM Equipment: Incorporated into various OEM systems requiring low-pressure, high-volume airflow.
Advantages
- Compact Design: Small footprint and lightweight.
- Low Maintenance: Minimal wear components, leading to reduced maintenance.
- Operational Versatility: Can be used in both pressure and vacuum applications.
Disadvantages
- Performance Limitations: Less effective for high-pressure applications.
- Efficiency: May have lower efficiency at higher pressures compared to centrifugal blowers.
Comparison of Aeration Blower Types
The table below compares the machine families across the criteria that decide selection. Values are typical or approximate and vary by manufacturer, duty point, and package configuration.
| Type | Typical Pressure Range | Wire-to-Air Efficiency | Turndown | Noise (bare machine) | Best-Fit Applications |
|---|---|---|---|---|---|
| Rotary lobe (PD) | Up to ~15 psig | 45–60% | Wide, VFD-limited | 95–105 dBA; enclosure required | Small to mid plants, variable back pressure, tight capital budgets |
| Rotary screw (PD) | Up to ~22 psig | 60–70% | Wide, VFD-limited | 85–90 dBA | Deep basins and higher pressures where lobe efficiency falls away |
| Multistage centrifugal | 5–15 psig | 55–70% | ~60–100%, surge-limited | Moderate to high | Stable base load, large constant duty |
| Single-stage geared centrifugal | Wide | 70–80% | ~45–100%, surge-limited | Moderate | Well-characterized load profiles at larger plants |
| High-speed turbo | Typically to ~15 psig | 70–80% | ~40–100% on speed | 75–85 dBA | Energy-driven municipal duty; retrofits with space constraints |
| Regenerative (side channel) | ~2–3 psig | Low | Limited | Low | Aquaculture, package plants, shallow basins |
Turndown, Control, and Discharge Temperature
Three operating characteristics separate the families in service, and all three should be settled before a machine is chosen rather than discovered afterwards.
How Each Family Turns Down
Positive displacement machines turn down on speed through a variable frequency drive, with power falling close to proportionally with flow. The practical floor is set by motor cooling and by heat build-up at low speed rather than by any aerodynamic limit. Multistage centrifugal machines turn down by throttling the inlet or adjusting guide vanes, which moves the operating point along the curve toward the surge line — and throttling wastes energy, since the machine still does work against the restriction. Single-stage geared machines combine guide vanes with a variable diffuser to hold efficiency across a wider band. High-speed turbo machines vary impeller speed directly, which is the most efficient method available, bounded at the low end by minimum speed and surge.
Control Strategy Matters as Much as Machine Choice
An efficient machine under poor control delivers a fraction of its potential. Dissolved oxygen control with automatic airflow modulation, most-open-valve pressure trim that keeps at least one control valve nearly fully open to eliminate throttling losses, and staging logic that brings units on and off at sensible thresholds together account for a large share of realizable savings. This is closely tied to the blower sizing exercise, since the turndown a machine must deliver follows directly from the range between minimum and maximum calculated airflow, and a type selected without reference to that range will be wrong regardless of its catalogue efficiency.
Discharge Temperature and Downstream Materials
Compression heats air, and the effect is larger than most specifiers expect. Discharge temperatures well above 100 °C are routine at higher pressures, particularly on lobe machines which have no internal compression to moderate the rise. That matters downstream: PVC piping is generally limited to around 60 °C, which is why blower discharge headers are steel or stainless rather than plastic, and why expansion provision and flexible connectors belong in the piping design rather than being added after the first thermal cycle cracks a joint.
Factors to Consider When Choosing Aeration Blowers
- Specific Application Requirements: Different systems require different airflow rates, pressures, and duty cycles.
- Energy Efficiency: Higher efficiency can result in significant cost savings over time.
- Noise and Vibration: Some blower types are inherently quieter and produce less vibration.
- Maintenance Requirements: Consider the maintenance schedule and ease of access.
- Initial Cost vs. Lifetime Cost: Factor in energy consumption and maintenance costs over time.
Two further factors deserve equal weight. Site conditions — elevation and the full range of inlet air temperature — change the capacity a given machine actually delivers, and dynamic machines are more sensitive to them than positive displacement machines. And local service capability determines availability more than any published reliability figure: a high-efficiency package whose nearest qualified service technician is a day’s travel away will spend more hours out of service than a simpler machine the plant’s own staff can maintain. The broader treatment of wastewater treatment blowers covers how these machines behave once installed, packaged, and integrated into plant operations, which is where those practical factors show up.
Selection Framework
Type selection follows a short sequence, and running it in order eliminates most candidates before any vendor conversation begins.
Step 1: Let Pressure Narrow the Field
Required discharge pressure, built up from diffuser submergence plus system losses plus a fouling allowance, immediately excludes families. Above roughly 15 psig, rotary lobe machines and most turbo units drop out and the choice narrows to screw or multistage machines. Below 3 psig, regenerative blowers become viable and everything else is oversized for the duty.
Step 2: Plot the Load Duration Curve
Establish how many hours per year the system spends at each airflow. Most municipal plants operate near design airflow for only a few dozen hours annually and spend most of the year between 40 and 60 percent. A machine chosen for peak-point efficiency and a machine chosen for efficiency where the hours actually accumulate are frequently different machines, and the second one costs less to run.
Step 3: Compare on Lifecycle Energy
Consider a duty of 8,000 SCFM at 8 psig running continuously, with electricity at $0.10 per kWh. The adiabatic power required for that compression is approximately 175 kW. At a rotary lobe wire-to-air efficiency of 55 percent, actual draw is about 318 kW; at a high-speed turbo efficiency of 75 percent, about 233 kW. The 85 kW difference amounts to roughly 745,000 kWh and $74,500 per year, or on the order of $1.5 million across a twenty-year service life before any discounting.
That figure will usually exceed the entire capital difference between the two packages several times over — which is why the efficiency comparison should be run before capital cost is discussed, not after. It also explains why the calculation reverses at small scale: on a duty a tenth that size, the annual difference falls to a few thousand dollars and the simplicity and serviceability of a lobe machine may well win.
Step 4: Verify Against Site Conditions and Support
Confirm performance at the actual site elevation and across the full design inlet temperature range, not at standard conditions. Confirm surge margin at every duty point for dynamic machines. Then evaluate the supplier: the review of aeration blower manufacturers covers the suppliers active in this market and the criteria — service coverage, parts availability, control system openness — that determine whether the selected machine performs across its service life rather than only on the test stand.
Advancements in Aeration Blower Technology
- Smart Blowers: Real-time monitoring enables predictive maintenance and optimization.
- Variable Speed Drives (VSD): Adjust blower speeds to match process needs, improving efficiency.
- Noise Reduction Technologies: Developments in acoustic engineering have led to quieter blowers.
Field Notes
Most blower disappointments trace back to a mismatch between the machine’s characteristic and the system it was installed into, and they are visible early if anyone measures.
Commissioning and Verification
Record airflow, discharge pressure, inlet air temperature, and blower input power together at several duty points during commissioning, with clean diffusers. That set of readings is the only defensible basis for a later efficiency claim, and inlet temperature in particular is routinely omitted — which makes the whole record unusable for comparison against a guarantee. On dynamic machines, verify surge margin at the lowest expected duty point rather than assuming the control system will protect it, and confirm that the anti-surge response has been tested rather than merely configured.
Pro Tip: Ask every vendor for the full performance map, not the single guaranteed duty point. The map shows efficiency across the whole operating range, and it shows where the surge line sits on dynamic machines. Overlay your load duration curve on it and the comparison answers itself — a machine that is three points more efficient at the peak but falls off a cliff at 50 percent flow will lose to a flatter competitor over a year of real operation. Vendors supply the map on request; almost nobody asks for it.
Common Selection Mistakes
The most frequent error is comparing efficiency figures without confirming they are stated on the same basis — wire-to-air package efficiency and bare-shaft efficiency differ by the drive, motor, and filter losses, and a comparison mixing the two is meaningless. The second is selecting a dynamic machine for a system whose back pressure will rise substantially as diffusers foul, since rising pressure pushes the operating point toward surge and reduces flow just when more is needed. The third is treating noise as a package accessory rather than a selection criterion, then discovering that the enclosure required to meet a site limit adds cost and complicates maintenance access. The fourth is ignoring inlet air quality: blowers draw large volumes through filters that need real maintenance, and a neglected filter costs pressure and therefore energy every hour.
Common Mistake: Selecting a high-efficiency dynamic machine for a plant whose load varies over a wide range without checking turndown against the surge line. Peak-point efficiency is irrelevant if the machine spends most of the year near its minimum flow, where a throttled centrifugal unit either approaches surge or blows off excess air to stay clear of it — and blow-off is energy purchased and then discarded. Match the machine’s usable turndown to the actual load duration curve first; compare peak efficiency second.
Design Details and Standards
Blower selection is governed principally by testing standards, which are what make competing efficiency claims comparable in the first place.
Applicable Standards and References
Selection and procurement practice draws on ASME PTC 13, Wire-to-Air Performance Test Code for Blower Systems, which defines how package efficiency is measured and is the correct reference for any performance guarantee; ISO 1217 for displacement compressor acceptance testing and ISO 5389 for turbocompressor performance testing; ASME PTC 9 for displacement compressors and exhausters; WEF Manual of Practice No. 8, Design of Water Resource Recovery Facilities, and the joint WEF and ASCE manual of practice on aeration for process context; ISO 2151 for noise measurement on compressors and vacuum pumps, alongside applicable occupational noise exposure limits; NEMA MG-1 and the applicable motor efficiency regulations for the drive; and the Recommended Standards for Wastewater Facilities (Ten States Standards) for redundancy and firm capacity criteria.
Specification Checklist
- Required airflow range — minimum and maximum — with the load duration profile stated
- Discharge pressure built up from submergence, system losses, and a fouled-diffuser allowance
- Site elevation and full design inlet air temperature range specified explicitly
- Efficiency guarantee stated as wire-to-air package efficiency referenced to ASME PTC 13
- Full performance map required as a submittal, not just the guaranteed duty point
- Turndown range with the method stated, and surge margin verified at every duty point for dynamic machines
- Anti-surge protection and its test procedure defined for dynamic machines
- Noise limit at a stated distance, with enclosure requirements and maintenance access considered together
- Discharge temperature at maximum duty, with downstream piping materials and expansion provision suited to it
- Inlet filtration specification with pressure drop allowance and service interval
- Control interface and protocol, including compatibility with plant DO control and most-open-valve logic
- Firm capacity and staging arrangement — design demand met with the largest unit out of service
- Service coverage, spare parts availability, and lead times confirmed for the specific supplier
Frequently Asked Questions
What is the practical difference between positive displacement and centrifugal blowers?
A positive displacement machine delivers a fixed volume per revolution, so flow is independent of discharge pressure and the machine tolerates rising back pressure without instability. A centrifugal machine follows a performance curve where flow and pressure are coupled, so raising back pressure reduces flow, and reducing flow too far causes surge. That difference drives most of the selection logic: positive displacement suits systems with variable or rising resistance, dynamic machines suit stable, well-characterized duty at larger scale.
What is surge and why does it limit turndown?
Surge occurs when flow through a dynamic machine falls below the point at which the impeller can sustain discharge pressure. Flow reverses momentarily, then re-establishes, cycling rapidly and producing violent vibration that damages bearings and seals. Every centrifugal and turbo machine has a surge line on its performance map, and safe operation requires a margin of roughly 10 to 15 percent to the right of it — which is why turndown on these machines is bounded by aerodynamics rather than by the drive.
Why are screw blowers more efficient than rotary lobe blowers?
Internal compression. A lobe machine pushes trapped air out against system pressure with no compression inside the machine, while a screw profile progressively reduces the trapped volume so air arrives near system pressure. That typically yields 10 to 30 percent lower energy consumption at the same duty, along with far less pulsation and correspondingly lower noise.
Are high-speed turbo blowers always the best choice?
No. They offer the highest wire-to-air efficiency generally available and wide speed-based turndown, which makes them compelling where energy dominates operating cost at municipal scale. But capital cost is higher, performance is sensitive to elevation and inlet temperature, and they place sophisticated electronics in a humid environment. At smaller scale the annual energy difference shrinks to a few thousand dollars, at which point the simplicity and local serviceability of a lobe machine often wins.
How much does blower type actually affect operating cost?
Substantially. At a duty of 8,000 SCFM and 8 psig running continuously, the difference between 55 percent and 75 percent wire-to-air efficiency is about 85 kW — roughly 745,000 kWh and $74,500 per year at $0.10 per kWh, or on the order of $1.5 million over a twenty-year life. That difference typically exceeds the capital gap between the packages several times over, which is why the efficiency comparison belongs before the capital discussion.
Key Takeaways
- The PD/dynamic divide explains most behaviour — positive displacement delivers fixed volume regardless of pressure; dynamic machines follow a curve and can surge.
- Surge, not the drive, limits turndown on dynamic machines — verify margin at the lowest duty point, and test the anti-surge response rather than just configuring it.
- Internal compression is why screw beats lobe — 10 to 30 percent lower energy at the same duty, with less pulsation and lower noise.
- Plot the load duration curve before choosing — most plants sit at 40 to 60 percent of design for most of the year, and the machine that wins there is often not the one that wins at peak.
- Efficiency figures must be on the same basis — wire-to-air package efficiency and bare-shaft efficiency are not comparable numbers.
- Ask for the full performance map — it shows efficiency across the range and where the surge line sits; vendors supply it on request and almost nobody asks.
- Discharge heat constrains downstream materials — temperatures well above 100 °C rule out PVC headers and make expansion provision a design requirement.
Conclusion
Aeration blowers are crucial across industries. Understanding the nuances of each type and staying informed about technological advancements helps industries optimize aeration processes for better performance, sustainability, and cost-efficiency.
The selection sequence that produces a defensible answer is short: let required discharge pressure eliminate the families that cannot reach it, plot the load duration curve to find where the operating hours actually accumulate, compare candidates on lifecycle energy at that duty rather than at peak, and verify performance at real site elevation and inlet temperature with surge margin confirmed across the range. Worked in that order, type selection usually resolves itself well before the capital comparison. Worked backwards from capital cost, it produces a machine that meets its guarantee on the test stand and disappoints for twenty years.