
Sleeve Valves Automation: Actuation Options
INTRODUCTION
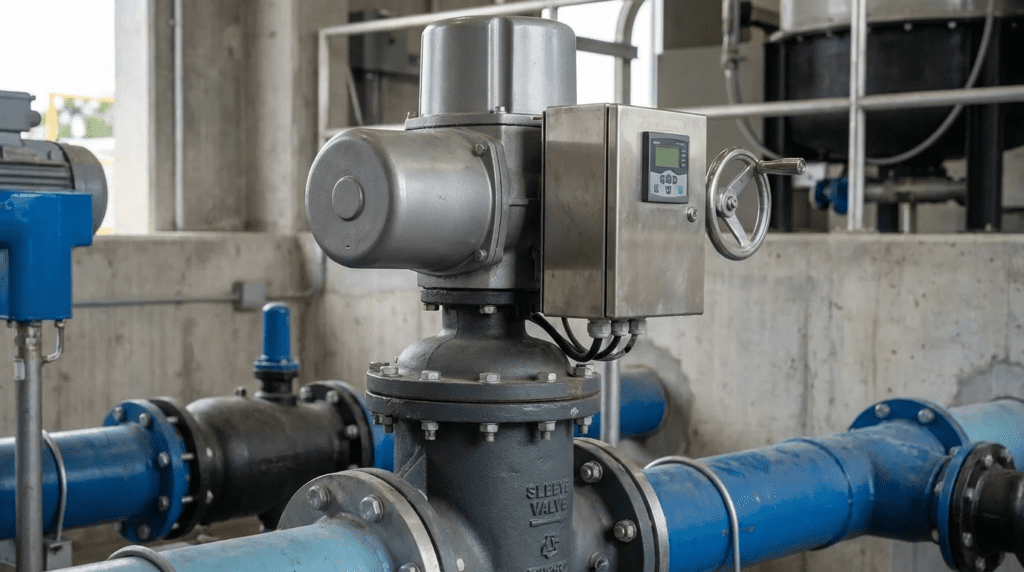
One of the most critical challenges engineers face in high-pressure water transmission and treatment facilities is precisely controlling flow while mitigating cavitation. When specifying energy-dissipating equipment, engineers often focus entirely on the valve’s hydraulic performance and port design, treating the actuator as an afterthought. This is a costly specification mistake. A sleeve valve is only as effective as the actuator controlling it. Without careful consideration of Sleeve Valves Automation: Actuation Options, facilities frequently experience actuator hunting, premature mechanical wear, seal failure, or catastrophic loss of flow control during transient events.
Sleeve valves operate by sliding an external or internal cylindrical gate (the sleeve) over a stationary pipe section dotted with precisely machined orifices. Because these valves are inherently designed for high differential pressure applications—such as reservoir discharges, pressure reducing stations, and turbine bypass systems—they require significant thrust to overcome friction and hydrodynamic forces. Furthermore, because they are typically employed for continuous modulation rather than simple open/close isolation, the actuator must possess exceptional resolution, minimal deadband, and robust continuous-duty capabilities.
This article provides a comprehensive, unbiased engineering framework for evaluating Sleeve Valves Automation: Actuation Options. Designed for utility engineers, public works decision-makers, and plant superintendents, this guide breaks down the technical selection criteria, mechanical constraints, and lifecycle cost drivers of various actuation technologies. By understanding the intricate relationship between the sleeve valve’s mechanical requirements and the actuator’s performance envelope, engineers can specify automation packages that ensure long-term reliability, precise process control, and optimal total cost of ownership. Sleeve valves occupy a specialized niche among the valves used in water treatment: they exist specifically to destroy energy in a controlled way, and that purpose shapes every automation decision that follows.
SLEEVE VALVES IN CONTEXT: CATEGORY OVERVIEW
A sleeve valve is a multi-orifice throttling device. Rather than forcing the entire flow through a single restriction, it distributes the pressure drop across many small ports discharging into a surrounding chamber or downstream pipe, so cavitation bubbles collapse in open water rather than against a metal surface. That places it in the same functional family as anti-cavitation valves, which achieve the same result through stacked trim, labyrinth paths, or drilled cages, and alongside cone valves, the other device commonly specified for high-head free discharge and turbine bypass service. Because sleeve valves modulate continuously against substantial differential pressure, the actuator is not an accessory but a process component, which is why the broader subject of valve actuators is inseparable from sleeve valve specification.
Three areas determine whether a sleeve valve installation performs as designed, and each has its own coverage on this site.
Manufacturer and Product Landscape
Sleeve valve supply is concentrated among a small number of specialists, and the designs are not interchangeable. Port pattern, sleeve travel, guide arrangement, seat design, and whether the valve is configured for inline or terminal free discharge all vary by manufacturer, and each vendor sizes against its own proprietary Cv and cavitation data. Our review of the top OEMs for sleeve valves covers the major suppliers serving municipal and industrial water systems. Manufacturer selection matters more here than in commodity valve categories for two reasons: the thrust and stroke characteristics the actuator must satisfy are set by the specific valve design, and replacement sleeves and seats over a multi-decade service life are available from the original supplier only. Establish parts availability and application engineering support before the hydraulic comparison narrows the field.
Installation Practice and Leak Prevention
Sleeve valves are less forgiving of installation error than isolation valves because they operate continuously under high differential pressure, so any defect is loaded constantly rather than intermittently. The recurring problems are pipe stress transferred into the valve body from misaligned flanges, inadequate support of the valve and actuator assembly in vertical terminal installations, insufficient downstream submergence on free-discharge configurations, and debris left in the line during commissioning that lodges in the orifice ports and scores the sleeve. Upstream straight pipe run is another routine omission: a sleeve valve set immediately downstream of an elbow or a partly open isolation valve receives a distorted velocity profile that loads the sleeve unevenly and produces a thrust requirement above the calculated figure. Confirm alignment with a dial indicator rather than by eye, and flush the line before the valve goes into modulating service.
Sizing, Cv, and Cavitation Selection
Sizing a sleeve valve is a cavitation problem as much as a capacity problem. The flow coefficient establishes how much flow the valve passes at a given differential pressure and opening, but the governing question is whether the pressure recovery downstream of the ports drives the fluid below vapor pressure and, if so, whether the resulting bubbles collapse in free water or against the sleeve. Selection therefore works from the cavitation index at each operating condition rather than from a single duty point, and the useful operating range is bounded at the low end as well as the high: a sleeve valve throttled to a very small opening concentrates the entire pressure drop across a handful of ports, which is exactly the condition the multi-port geometry exists to avoid. Establish the full range of upstream and downstream pressures the valve will see, including seasonal and demand extremes, before fixing a size. An oversized sleeve valve that spends its life nearly closed is a more common failure than an undersized one.
HOW TO SELECT / SPECIFY SLEEVE VALVES AUTOMATION: ACTUATION OPTIONS
Selecting the correct actuator for a sleeve valve requires a holistic analysis of the installation environment, process dynamics, and utility infrastructure. The following engineering criteria form the foundation for a robust specification.
Duty Conditions & Operating Envelope
Unlike isolation valves, sleeve valves typically operate in a continuous modulating mode to maintain a precise downstream pressure, flow rate, or reservoir level. The actuator must be rated for continuous modulation (typically defined as Class III or Class IV duty per AWWA and ISA classifications).
- Thrust Requirements: Sleeve valves require linear thrust (or rotary torque converted to linear motion via a mechanical linkage). The required thrust must account for dynamic fluid forces, static friction (stiction) of the seals, and breakaway forces after long periods of inactivity.
- Stroke Speed: While rapid closure is sometimes necessary to prevent reservoir overflow, actuating a sleeve valve too quickly can induce severe water hammer. The operating envelope must define independent, adjustable opening and closing stroke times.
- Modulation Frequency: Systems requiring constant micro-adjustments will quickly wear out the mechanical contactors in standard electric actuators. Solid-state motor controllers or hydraulic systems are preferred for high-frequency modulation.
Materials & Compatibility
The operating environment dictates the materials of construction and the enclosure ratings required for the actuator.
- Enclosure Ratings: For indoor or weather-protected environments, NEMA 4 (IP66) is standard. For vaults subject to flooding, NEMA 6P (IP68) continuous submergence ratings are mandatory. Specifications must clearly state the required submergence depth and duration (e.g., 10 meters for 72 hours).
- Corrosion Protection: In wastewater applications with high hydrogen sulfide (H2S) concentrations, or coastal environments, actuators must feature specialized coatings (such as marine-grade epoxy) and Type 316 stainless steel fasteners.
- Hydraulic Fluids: If specifying an electro-hydraulic actuator near a potable water source, environmental regulations often mandate the use of biodegradable, food-grade hydraulic fluids. These fluids have different viscosity indices and temperature limits compared to standard mineral oils.
Hydraulics & Process Performance
The integration of the actuator with the sleeve valve’s inherent flow characteristic is critical for process stability.
- Resolution and Deadband: The actuator must be capable of small incremental movements. A high-resolution actuator (e.g., 0.1% of stroke) ensures the valve can precisely match the process setpoint. Excessive deadband leads to control loop hunting, where the valve oscillates continuously around the setpoint.
- Stick-Slip Phenomenon: Particularly relevant to pneumatic actuators, “stick-slip” occurs due to the compressibility of air. The actuator builds pressure until it overcomes the static friction of the sleeve valve, causing the valve to jerk forward and overshoot the target position. This is why pneumatic actuators are generally avoided for precise modulating sleeve valves unless equipped with high-performance positioners and volume boosters.
Installation Environment & Constructability
Physical constraints often dictate the practical limits of Sleeve Valves Automation: Actuation Options.
- Vault Constraints: Underground pressure-reducing vaults are notoriously cramped. Purely hydraulic cylinders offer the highest power density (thrust-to-size ratio), making them ideal for tight spaces, provided a Hydraulic Power Unit (HPU) can be located nearby.
- Power Availability: Remote reservoir discharge valves may lack 480V, 3-phase power. In such cases, 24VDC solar-powered electric actuators or self-contained gas-over-oil systems must be evaluated.
- Orientation: Actuators mounted horizontally may experience accelerated wear on one side of the cylinder or stem nut due to gravity. The specification must explicitly state the mounting orientation so the manufacturer can provide appropriate internal supports.
When specifying electro-hydraulic actuators in unventilated outdoor vaults, ensure the design accounts for thermal expansion of the hydraulic fluid. High ambient summer temperatures can cause fluid expansion, leading to uncommanded valve creeping if thermal relief valves or accumulators are not properly sized.
Reliability, Redundancy & Failure Modes
The response of the automated sleeve valve to a loss of primary power or control signal is arguably its most critical specification parameter.
- Fail-Safe Action: Depending on the process, upon power loss, the valve must either Fail Open (to relieve pressure), Fail Closed (to prevent flooding), or Fail Last Position.
- Fail-Safe Mechanisms: Electric actuators typically require an uninterruptible power supply (UPS) or an internal mechanical spring to achieve fail-safe operation. Springs limit the maximum size of the actuator. Electro-hydraulic systems utilize nitrogen-charged accumulators to provide fail-safe thrust without relying on electrical power.
- Mean Time Between Failures (MTBF): For mission-critical bypass applications, require MTBF documentation and specify redundant control elements (e.g., dual redundant LVDT position sensors).
Controls & Automation Interfaces
Modern actuation options must integrate seamlessly with plant SCADA (Supervisory Control and Data Acquisition) systems.
- Protocols: Standard analog control utilizes 4-20mA signals for command and feedback. Digital networks (Modbus RTU/TCP, Ethernet/IP, Profinet) provide richer data, including torque profiles, internal temperatures, and alarm diagnostics.
- Position Feedback: Absolute encoders are superior to incremental encoders. If power is lost and the valve is manually moved via a handwheel, an absolute encoder instantly knows the valve’s true position upon power restoration without requiring a recalibration stroke.
Maintainability, Safety & Access
Maintenance personnel must be able to interact safely with the automated valve under all conditions.
- Manual Override: All automated sleeve valves must include a declutchable manual override handwheel. The gear ratio must be sized so that an operator can stroke the valve against full differential pressure without exceeding 50 lbs (approx. 220 N) of rim pull force.
- Lockout/Tagout (LOTO): Hydraulic and pneumatic systems require dedicated block-and-bleed valves to safely depressurize the system before maintenance.
Lifecycle Cost Drivers
A Total Cost of Ownership (TCO) analysis should drive the final selection of Sleeve Valves Automation: Actuation Options.
- CAPEX: Electric motor actuators have a lower initial cost and simpler installation footprint compared to complex electro-hydraulic systems.
- OPEX: Hydraulic systems require periodic fluid sampling, filter replacements, and seal inspections. Conversely, modern smart electric actuators require very little preventative maintenance beyond routine visual inspections and occasional stem lubrication.
- Energy Efficiency: Modulating pneumatic systems consume compressed air continuously (instrument bleed), which represents a hidden but significant energy cost. Electric actuators consume power primarily only when in motion.
COMPARISON TABLES FOR SLEEVE VALVES AUTOMATION: ACTUATION OPTIONS
The following tables provide a structured comparison of the primary actuation technologies and their suitability for various sleeve valve applications. Use Table 1 to evaluate the inherent characteristics of each technology, and Table 2 to determine the best fit based on specific operational scenarios.
| Technology Type | Key Features & Resolution | Best-Fit Applications | Limitations & Considerations | Typical Maintenance Profile |
|---|---|---|---|---|
| Electric Motor (Smart Actuator) | High precision (0.1% resolution), extensive diagnostic data, simple wiring integration. | General PRV stations, flow control with moderate speeds, reliable power grids. | Difficult to achieve rapid fail-safe action without external UPS; lower thrust-to-size ratio. | Low. Periodic stem lubrication, battery replacement for encoders (if applicable). |
| Electro-Hydraulic (Self-Contained) | Combines electric control with hydraulic power. Excellent resolution, extremely high thrust, reliable fail-safe via accumulators. | Large diameter sleeve valves, high-pressure differentials, critical turbine bypass. | High CAPEX, larger footprint, thermal expansion sensitivities in closed vaults. | Moderate. Fluid sampling, filter changes, accumulator nitrogen pressure checks. |
| Hydraulic Cylinder (Central HPU) | Smallest footprint on the valve, highest thrust density, rugged construction. | Submerged vaults (IP68), multi-valve installations sharing one HPU, extremely harsh environments. | Requires expensive centralized HPU infrastructure and extensive hydraulic piping. Leak risks. | High. Maintaining HPU, inspecting high-pressure tubing, managing oil leaks. |
| Pneumatic Cylinder | Fast stroke speeds, inherently fail-safe via springs or volume tanks, lower initial cost. | Smaller sleeve valves, applications requiring rapid emergency closure. | Compressibility of air causes stick-slip issues during precise modulation; requires plant air infrastructure. | Moderate. Air filter regulator (AFR) maintenance, ensuring dry instrument air. |
| Application Scenario | Primary Constraint | Optimal Actuation Option | Secondary Option | Relative Cost Factor |
|---|---|---|---|---|
| Deep Vault Pressure Reduction | Submergence risk, confined space | Hydraulic Cylinder (Remote HPU) | Submersible Electric (IP68) | High ($$$) |
| Turbine Bypass / Surge Relief | Rapid opening requirement, fail-safe open | Electro-Hydraulic with Accumulator | Pneumatic with Volume Tank | High ($$$) |
| Reservoir Discharge (Grid Power) | Continuous precise modulation | Smart Electric Motor | Electro-Hydraulic | Moderate ($$) |
| Remote Off-Grid Flow Control | Limited power availability (Solar/DC) | Low-Voltage DC Electric Motor | Gas-over-Oil Actuator | Low/Moderate ($$) |
ENGINEER & OPERATOR FIELD NOTES
Specifying the equipment is only half the battle. Successful integration of Sleeve Valves Automation: Actuation Options relies heavily on rigorous testing, precise control loop tuning, and realistic maintenance strategies.
Commissioning & Acceptance Testing
Commissioning an automated sleeve valve should follow a structured verification process to ensure performance matches the design intent.
- Factory Acceptance Test (FAT): Require dynamic testing if possible. Unloaded bench testing of an actuator does not reveal how it will perform under the hydraulic unbalance and friction loads of the sleeve valve. Verify the torque/thrust proving curves from the manufacturer.
- Site Acceptance Test (SAT): At the site, stroke the valve fully open to fully closed under actual process conditions. Verify the required stroke times. Critically, perform a “step test” by issuing a 1% or 2% position change command from the SCADA system and verifying that the actuator moves cleanly without hunting or overshooting.
- Fail-Safe Verification: During the SAT, intentionally pull the primary power and verify that the fail-safe mechanism (UPS, accumulator, or spring) actuates the valve to the correct position within the specified timeframe.
Common Specification Mistakes
Consulting engineers frequently fall into several traps when writing automation specifications for sleeve valves.
- Undersizing for Breakaway Friction: A sleeve valve that has been sitting statically closed for a month requires significantly more thrust to initiate movement than it does to keep moving. Specifying an actuator based solely on “running thrust” will result in a jammed valve. Always specify a 1.5 to 2.0 safety factor over the calculated breakaway thrust.
- Ignoring Hysteresis: Allowing standard mechanical slop in the linkage between the actuator and the sleeve valve introduces hysteresis. If the process requires 0.5% control accuracy, but the linkage has 2% mechanical play, the system will never stabilize. Specifications must mandate zero-backlash couplings or direct stem connections.
- Ambiguous Control Loop Responsibility: Who is tuning the PID loop? If the actuator manufacturer, valve manufacturer, and systems integrator are separate entities, a poorly tuned system often results in finger-pointing. The specification must designate a single point of responsibility for final loop tuning.
Engineers often arbitrarily specify fast stroke times (e.g., “valve must fully close in 10 seconds”). For large diameter water transmission mains, a 10-second closure on a sleeve valve will almost certainly induce catastrophic water hammer. Perform a hydraulic transient analysis before specifying maximum actuator speeds.
O&M Burden & Strategy
Operators must adapt their maintenance strategies to the specific actuation technology deployed.
- Routine Inspection (Monthly): For all actuators, verify that there are no abnormal noises, excess heat generation, or fluid leaks. For smart electric actuators, review the internal data logger for torque alarms or increased motor starts, which indicate an emerging issue with the valve internals.
- Preventative Maintenance (Annual): Electro-hydraulic systems require annual oil sampling to check for particulate contamination and water ingress. Accumulator pre-charge pressure must be verified using a nitrogen charging kit.
- Labor Estimates: A smart electric actuator typically requires less than 4 labor hours per year for routine checks and lubrication. An electro-hydraulic system may require 12-16 labor hours per year for comprehensive fluid management and pressure testing.
Troubleshooting Guide
When an automated sleeve valve fails to control the process correctly, use this diagnostic hierarchy:
- Symptom: Valve is hunting (continuous small movements).
Root Cause: Often a PID tuning issue. The proportional band may be too narrow, or the integral time too short. Alternatively, the actuator’s internal deadband setting is smaller than the mechanical slop in the valve linkage. Quick Fix: Widen the deadband setting in the actuator configuration menu. - Symptom: Valve stalls mid-stroke.
Root Cause: Actuator is hitting its torque/thrust limit. This could be due to galling on the valve sleeve, debris lodged in the ports, or a failed hydraulic pump. Diagnostic: Attempt to move the valve with the manual handwheel. If it is physically jammed, the issue is the valve. If it turns easily, the issue is the actuator power module. - Symptom: Uncommanded movement (creeping).
Root Cause: In hydraulic actuators, this indicates fluid bypassing the piston seal or a leaking directional control valve. In electric actuators, it suggests a failed motor brake. - Symptom: Persistent noise and vibration at partial opening.
Root Cause: Cavitation at the operating condition rather than an actuator fault. Sleeve valves throttled to a small opening concentrate the full pressure drop across a few ports, defeating the multi-port geometry. Diagnostic: Log the upstream and downstream pressures at the opening where noise appears and compare against the manufacturer’s cavitation limits before adjusting anything in the control loop.
DESIGN DETAILS / CALCULATIONS
Proper sizing and specification of Sleeve Valves Automation: Actuation Options requires rigorous mathematical validation. Engineers should never rely solely on catalog estimates without understanding the underlying mechanics.
Sizing Logic & Methodology
Calculating the required thrust (Treq) for a linear sleeve valve involves summing multiple force vectors. The fundamental equation is:
Treq = (Fh + Ff + Fs) × SF
- Fh (Hydraulic Force): The dynamic force acting on the sleeve due to fluid velocity and differential pressure. This varies depending on the specific port design and internal geometry of the valve.
- Ff (Friction Force): The sliding friction of the sleeve against its internal guides and seals. Calculated as μ × N, where μ is the coefficient of friction (often highest at breakaway) and N is the normal force caused by hydraulic unbalance.
- Fs (Seating Force): The additional thrust required to compress the resilient elastomer seals tightly enough to achieve the specified leakage class (e.g., AWWA or ANSI Class VI) when fully closed.
- SF (Safety Factor): Typically 1.5 to 2.0 (150% to 200%). A higher safety factor is required for valves in raw water or wastewater service where scale build-up can increase sliding friction over time.
Worked Example Rule of Thumb: For a standard water application, if the valve manufacturer calculates a maximum combined force of 10,000 lbs under worst-case differential pressure, specify an actuator capable of delivering a continuous minimum thrust of 15,000 lbs (safety factor of 1.5).
Cavitation Index and the Operating Window
Thrust determines whether the valve moves; the cavitation index determines whether it survives. The index compares the available pressure margin above vapor pressure against the pressure drop the valve is taking, and it should be evaluated at every operating condition rather than at the design point alone. Two conditions bracket the problem. At maximum differential pressure with the valve well open, the drop per port is at its highest absolute value. At minimum flow with the valve nearly closed, the total drop concentrates across the few ports still exposed, which raises local velocity sharply even though the system differential may be modest.
The practical output of this analysis is a minimum permitted opening, not just a maximum. Where the required turndown falls below what a single valve can deliver without cavitating, the answer is usually two valves in parallel operating in sequence, or a sleeve valve paired with a smaller trim valve for low-flow duty, rather than a larger safety factor on the actuator. Establish this window before specifying stroke resolution, because a valve that must not go below thirty percent open does not need actuator resolution at five percent.
Specification Checklist
To ensure a bulletproof procurement process, your specification document should explicitly outline the following parameters:
- Process Data: Minimum/Maximum upstream pressure, downstream pressure, and flow rates.
- Actuator Type: Electric motor, electro-hydraulic, or pneumatic.
- Duty Cycle Rating: Clearly define continuous modulating duty (e.g., max 1,200 starts per hour).
- Enclosure Rating: NEMA 4, NEMA 4X, NEMA 6, or specific IP ratings.
- Control Signal: 4-20mA analog, or specific digital fieldbus protocol.
- Fail-Safe Requirement: Fail open, closed, or last position, including required time to fail position.
- Mechanical Override: Required handwheel rim pull limits.
- Diagnostics: Requirement for internal data logging and torque profiling capabilities.
- Minimum Permitted Opening: State the low-flow limit established by cavitation analysis, and require the control system to enforce it.
- Transient Analysis: Require that maximum opening and closing stroke times be confirmed against a surge analysis for the specific pipeline rather than set arbitrarily.
Standards & Compliance
Ensure the specified actuation equipment complies with relevant industry standards. While there is no single AWWA standard exclusively for “Sleeve Valves”, the actuation components must adhere to broader guidelines:
- AWWA C542: Electric Motor Actuators for Valves and Slide Gates. Ensures baseline quality for electric options.
- NEMA 250 / IEC 60529: Defines the environmental enclosure ratings (NEMA types and IP codes).
- UL/CSA/FM/ATEX: If the valve is located in a hazardous environment (e.g., an industrial wastewater plant with methane off-gassing), the actuator must carry the appropriate explosion-proof certifications (e.g., Class I, Division 1).
- ISA-75.25.01: Test Procedure for Control Valve Response Measurement from Step Inputs. Useful for defining the dynamic performance requirements of the actuator-valve assembly.
- ISA-75.01.01: Flow Equations for Sizing Control Valves. Provides the Cv methodology and the cavitation and choked flow terms used when evaluating the operating window.
The absence of a dedicated AWWA standard for sleeve valves is itself a specification issue. Because no common standard defines port geometry, leakage class, or thrust reporting for this valve type, vendor data is not directly comparable: one manufacturer’s stated thrust may include seating force while another’s does not, and cavitation limits are published against differing indices. Require each bidder to state the basis of their figures explicitly, and normalize the submittals yourself before comparing them.
FAQ ON SLEEVE VALVES AUTOMATION: ACTUATION OPTIONS
What is the primary difference between inline and terminal sleeve valves regarding actuation?
Inline sleeve valves regulate pressure or flow within a continuous pipeline, often requiring extremely precise modulating control to manage downstream pressure zones. Terminal sleeve valves discharge into the atmosphere (e.g., a reservoir or clearwell) and often prioritize rapid fail-safe capabilities to prevent overtopping. Actuator selection for inline valves typically leans toward smart electric motors for precision, while terminal valves often utilize electro-hydraulic systems for high-speed, high-thrust fail-safe action.
How do you select the correct safety factor when sizing an actuator for a sleeve valve?
Engineers typically apply a safety factor of 1.5 (150%) for clean, treated water applications. For raw water, industrial wastewater, or fluids with high scaling potential, a safety factor of 2.0 (200%) is recommended. This accounts for the gradual increase in sliding friction as mineral deposits or biofilms form on the valve sleeve over its lifecycle.
What is the typical lifespan of an electro-hydraulic actuator in a water treatment plant?
With strict adherence to preventative maintenance, an electro-hydraulic actuator typically lasts 20-30 years. However, soft goods such as piston seals and hydraulic hoses usually require replacement every 7-10 years. The hydraulic fluid should be sampled annually and replaced based on degradation analysis. Proper maintenance prevents premature failure of the high-pressure pump.
Why do sleeve valves sometimes hunt or oscillate when automated?
Hunting is usually caused by a mismatch between the plant’s PID control loop tuning and the mechanical deadband of the actuator/valve assembly. If the SCADA system demands a position adjustment smaller than the mechanical slop in the linkage or the actuator’s internal deadband limit, the system will continuously overshoot and correct. Ensure zero-backlash couplings are specified. See the Troubleshooting Guide section above for the full diagnostic sequence.
How much does a smart electric actuator for a large sleeve valve cost?
Costs vary significantly based on thrust requirements, enclosure ratings, and communication modules. For typical municipal applications (12-inch to 36-inch valves), an industrial smart electric actuator generally ranges from $10K to $35K approximate. Electro-hydraulic systems with accumulators for similar sizes can range from $30K to over $80K depending on HPU complexity and vault rating requirements.
Can pneumatic actuators be used for continuous modulating sleeve valves?
While possible, pneumatic actuators are generally not recommended for precise modulating sleeve valves due to the compressibility of air, which causes “stick-slip” movement resulting in poor resolution. If pneumatic actuation is required (e.g., for rapid fail-safe speed or plant standard alignment), it must be equipped with a high-performance digital smart positioner and volume boosters to optimize linearity.
How does a sleeve valve differ from other anti-cavitation control valves?
All of them work by splitting a single large pressure drop into many small ones, but the geometry differs. A sleeve valve distributes flow through machined ports in a cylinder and discharges into a surrounding chamber or the downstream pipe, so bubble collapse happens away from metal surfaces. Cage or trim-based anti-cavitation valves achieve the same staging inside a globe or axial body using stacked discs or drilled cages. Cone valves take a different approach, providing a straight-through low-loss path when open and relying on downstream energy dissipation rather than on staged trim. Sleeve valves are generally favoured where high differential pressure must be taken continuously and where the valve can be sized generously; cage-trim valves where space is constrained; cone valves where full-bore flow and rapid operation matter more than fine modulation.
What is the minimum opening a sleeve valve should be allowed to operate at?
It depends on the pressure conditions and the specific port design, and the manufacturer should state it. The principle is that the multi-port geometry only protects the valve while enough ports are exposed to share the pressure drop. Below that point the valve behaves like a single small orifice at high differential, which produces noise, vibration, and eventual erosion of the sleeve and seat. Establishing this limit is part of sizing, and it should be enforced in the control system rather than left to the operator or to a PID loop that does not know about it. Where the required turndown exceeds a single valve’s window, use parallel valves in sequence instead.
Does the actuator need to be sized for the fully closed condition or the operating range?
For the worst case across the entire stroke, which is usually not the same point as the maximum flow condition. Breakaway from the fully closed and seated position typically governs, because it combines seating force compression, static friction at its highest value, and full differential pressure across the sleeve. But hydraulic unbalance can peak at an intermediate opening on some port designs, so the thrust curve across the full stroke should be obtained from the manufacturer rather than assuming the closed position is always controlling. Size the actuator against the maximum of that curve, then apply the safety factor.
CONCLUSION
Key Takeaways: Sleeve Valves Automation
- Modulation is mandatory: Sleeve valves operate continuously; select actuators rated for Class III or IV continuous duty.
- Account for stiction: Always apply a 1.5 to 2.0 safety factor over the calculated breakaway thrust to prevent the valve from jamming after idle periods.
- Beware of water hammer: Do not over-specify fast closing times unless hydraulically required and validated by transient analysis.
- Match the technology to the risk: Use smart electric for precise, low-maintenance control. Use electro-hydraulic when high thrust and independent fail-safe action are non-negotiable.
- Eliminate hysteresis: Specify direct stem connections or zero-backlash couplings to prevent control loop hunting.
- Define the fail state: Clearly mandate whether the system must fail open, closed, or hold last position upon loss of power.
- Respect the low end of the range: Cavitation analysis sets a minimum permitted opening as well as a maximum drop, and that limit belongs in the control logic.
Specifying the optimal Sleeve Valves Automation: Actuation Options requires a disciplined engineering approach that balances hydraulic demands, process control theory, and practical operational constraints. By shifting the focus away from just the valve body and placing equal importance on the actuator selection, engineers can prevent the most common causes of control station failure: actuator hunting, inadequate breakaway thrust, and catastrophic power-loss scenarios.
The decision framework ultimately centers on the required operating envelope. For applications demanding extreme precision, ease of SCADA integration, and minimal maintenance, modern smart electric actuators are the preferred choice. When the physics of the application dictate exceptionally high thrust, rapid emergency stroke speeds, or failsafe requirements independent of the electrical grid, electro-hydraulic systems remain the gold standard despite their higher CAPEX and maintenance demands. Pneumatic systems, while cost-effective and fast, require careful engineering to overcome their inherent stick-slip limitations in modulating duties.
For highly complex projects involving large-diameter valves, deep submerged vaults, or severe cavitation indices, consulting engineers should involve actuation specialists early in the design phase. Conducting thorough total cost of ownership (TCO) analyses, requiring stringent FAT and SAT protocols, and providing operators with realistic maintenance expectations will ensure that the automated sleeve valve performs reliably throughout its intended multi-decade lifecycle. The category overview above links to manufacturer coverage and sets out the installation and sizing context that any automation decision depends on.